ISSN 1004-132X
CN 42-1294/TH
CN 42-1294/TH
中国机械工程 ›› 2026, Vol. 37 ›› Issue (10): 2446-2457.DOI: 10.3969/j.issn.1004-132X.2026.10.007
刘丹( ), 刘伟军, 刘顺, 杨志刚, 刘榜, 杨国哲, 姜兴宇()
收稿日期:2025-09-02
出版日期:2026-10-25
发布日期:2026-11-10
通讯作者:
姜兴宇
作者简介:刘丹,女,1982年生,博士研究生。研究方向为激光再制造与绿色制造。E-mail: 14734983@qq.com基金资助:
LIU Dan(), LIU Weijun, LIU Shun, YANG Zhigang, LIU Bang, YANG Guozhe, JIANG Xingyu()
Received:2025-09-02
Online:2026-10-25
Published:2026-11-10
Contact:
JIANG Xingyu
摘要:
针对激光熔覆过程中工艺系统能量转化效率低、加工周期长与物耗大等问题,提出一种面向低碳的激光熔覆过程工艺参数多目标优化方法。深入分析了激光熔覆工艺过程碳排放特性,以激光功率、送粉速度及扫描速度作为关键工艺参数,构建以碳排放、粉末利用率及质量(宽高比)为目标的激光熔覆工艺参数多目标优化模型。提出了一种改进的广义差分进化三代算法(GDE3),引入混沌记忆权重因子增强种群多样性,可有效解决算法过早收敛而难以获得最优工艺参数问题。以Fe3O4不锈钢为实验材料,开展了激光熔覆实验,实验结果表明,优化后的激光熔覆工艺碳排放降低25%,粉末利用率提高19%,熔覆层质量与性能显著提高。
中图分类号:
刘丹, 刘伟军, 刘顺, 杨志刚, 刘榜, 杨国哲, 姜兴宇. 面向低碳的激光熔覆过程工艺参数多目标优化[J]. 中国机械工程, 2026, 37(10): 2446-2457.
LIU Dan, LIU Weijun, LIU Shun, YANG Zhigang, LIU Bang, YANG Guozhe, JIANG Xingyu. Multi-objective Optimization of Process Parameters in Laser Cladding for Low Carbon Emission[J]. China Mechanical Engineering, 2026, 37(10): 2446-2457.
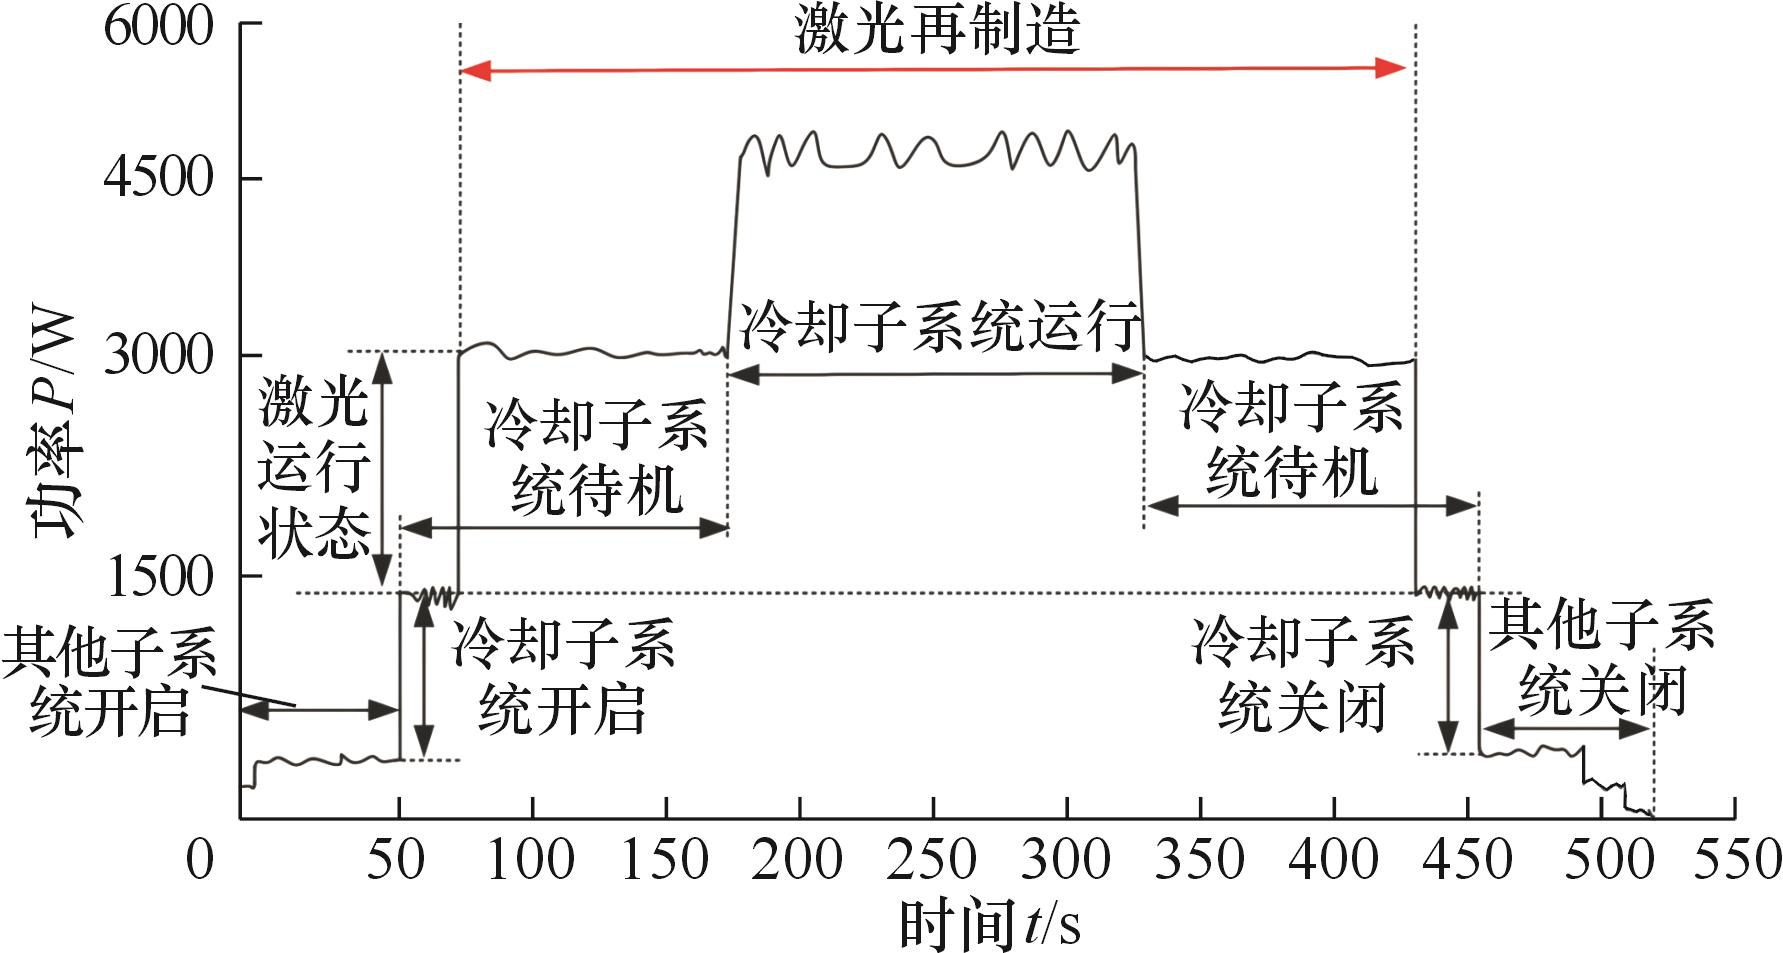
图1 激光熔覆装备的状态-功率曲线
Fig.1 State-power curve of laser cladding equipment
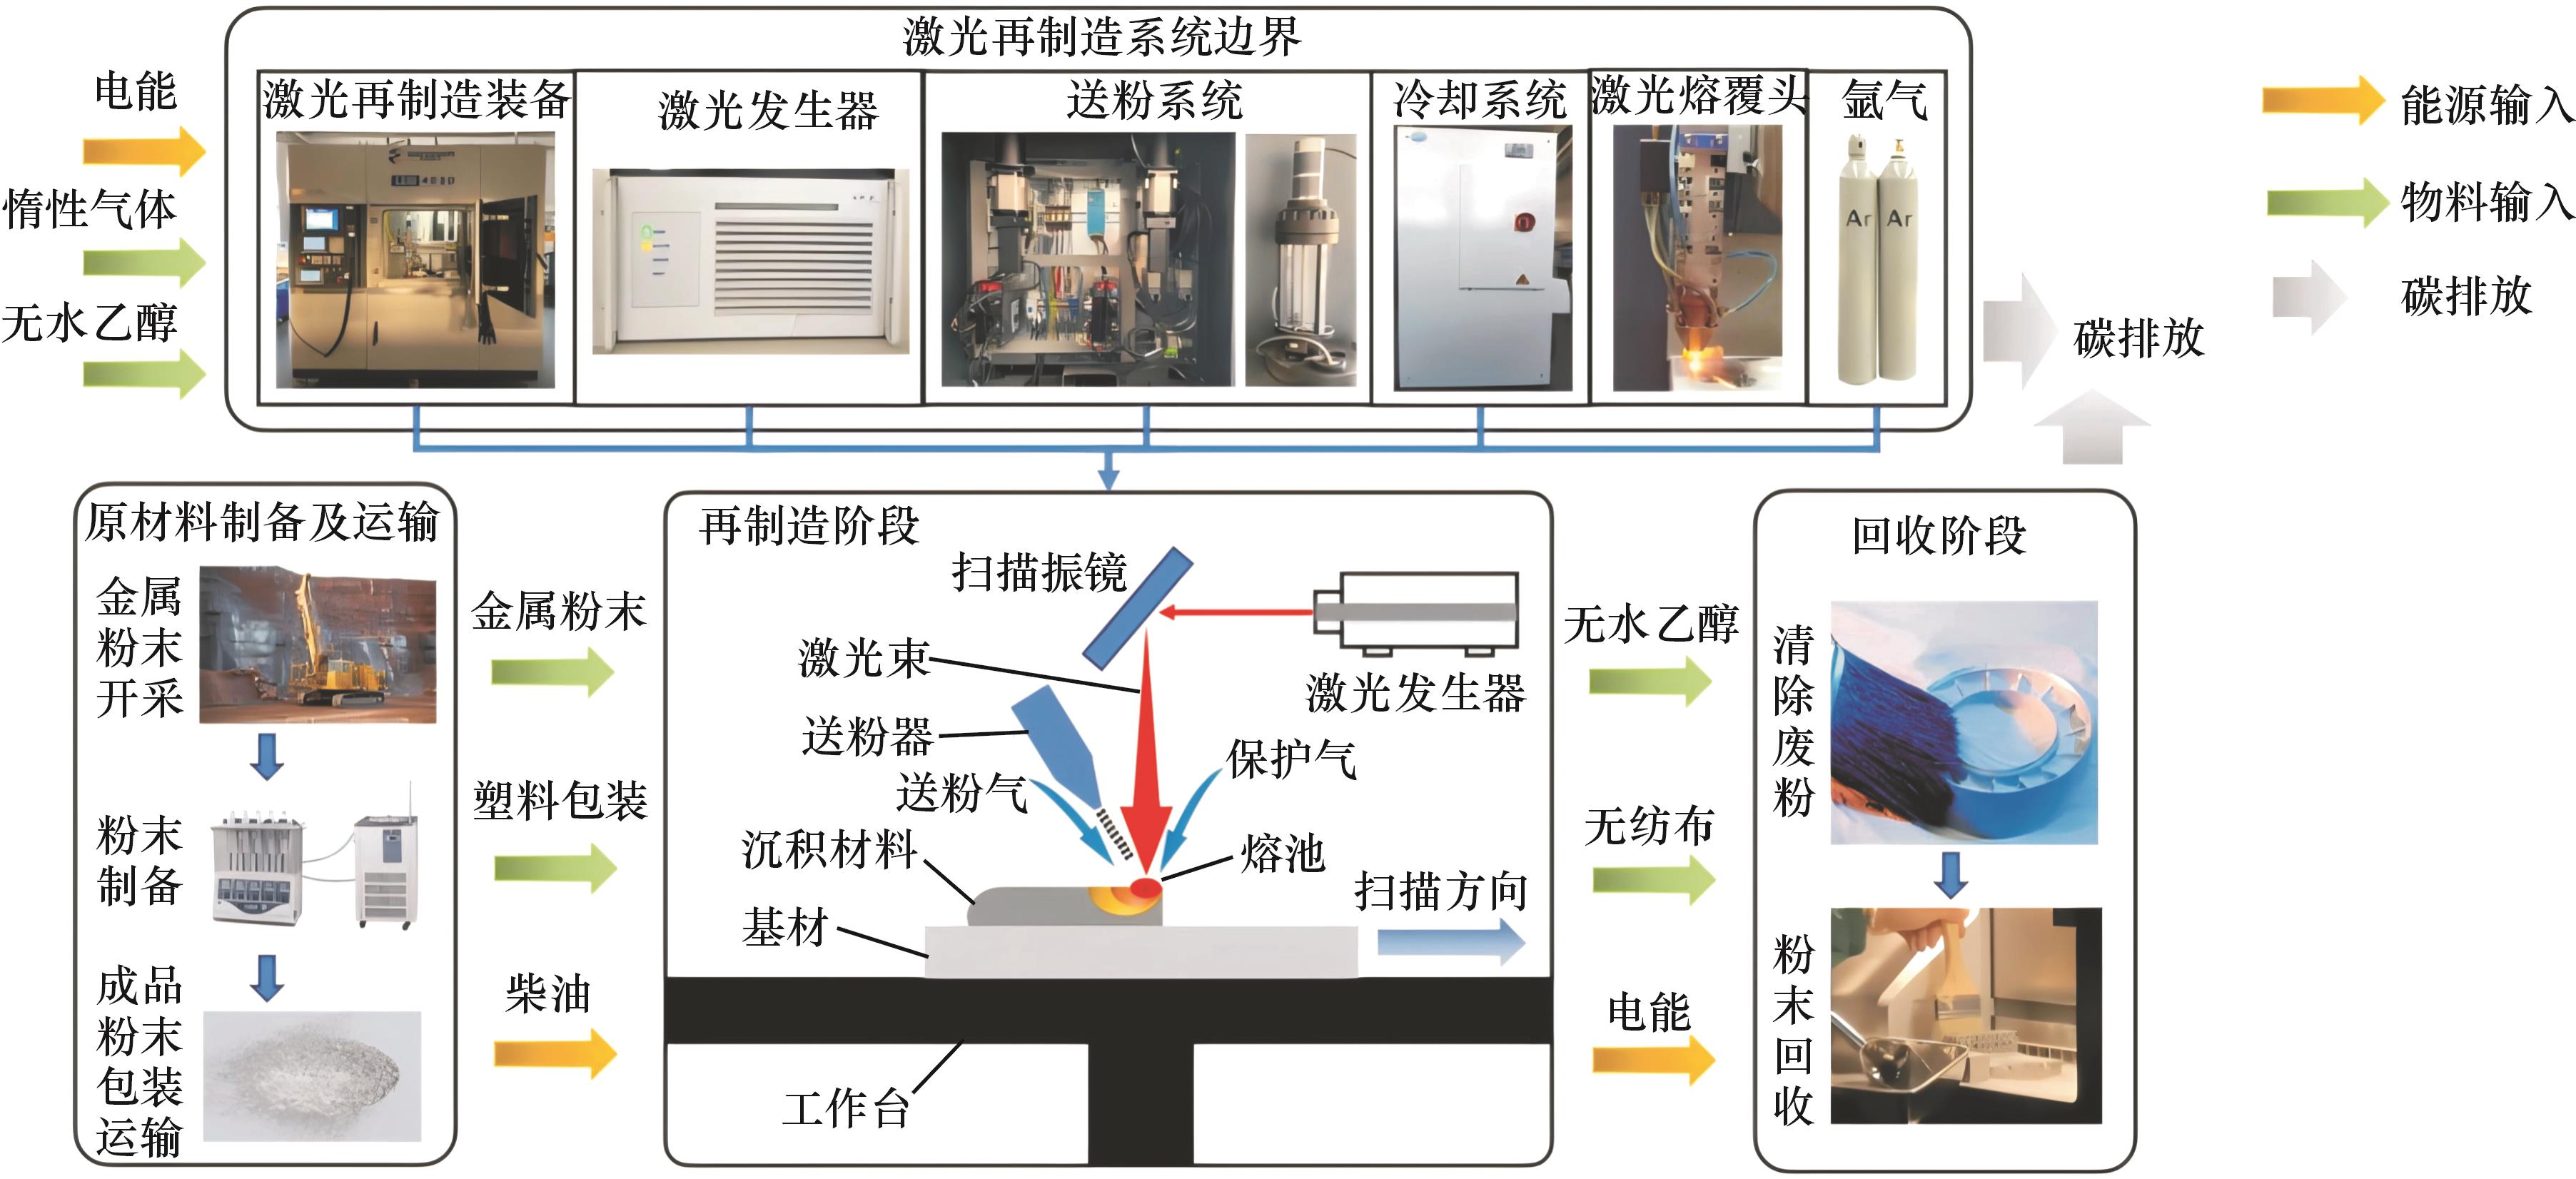
图2 激光熔覆过程的碳排放系统边界
Fig.2 System boundary of carbon emissions for the laser remanufacturing process
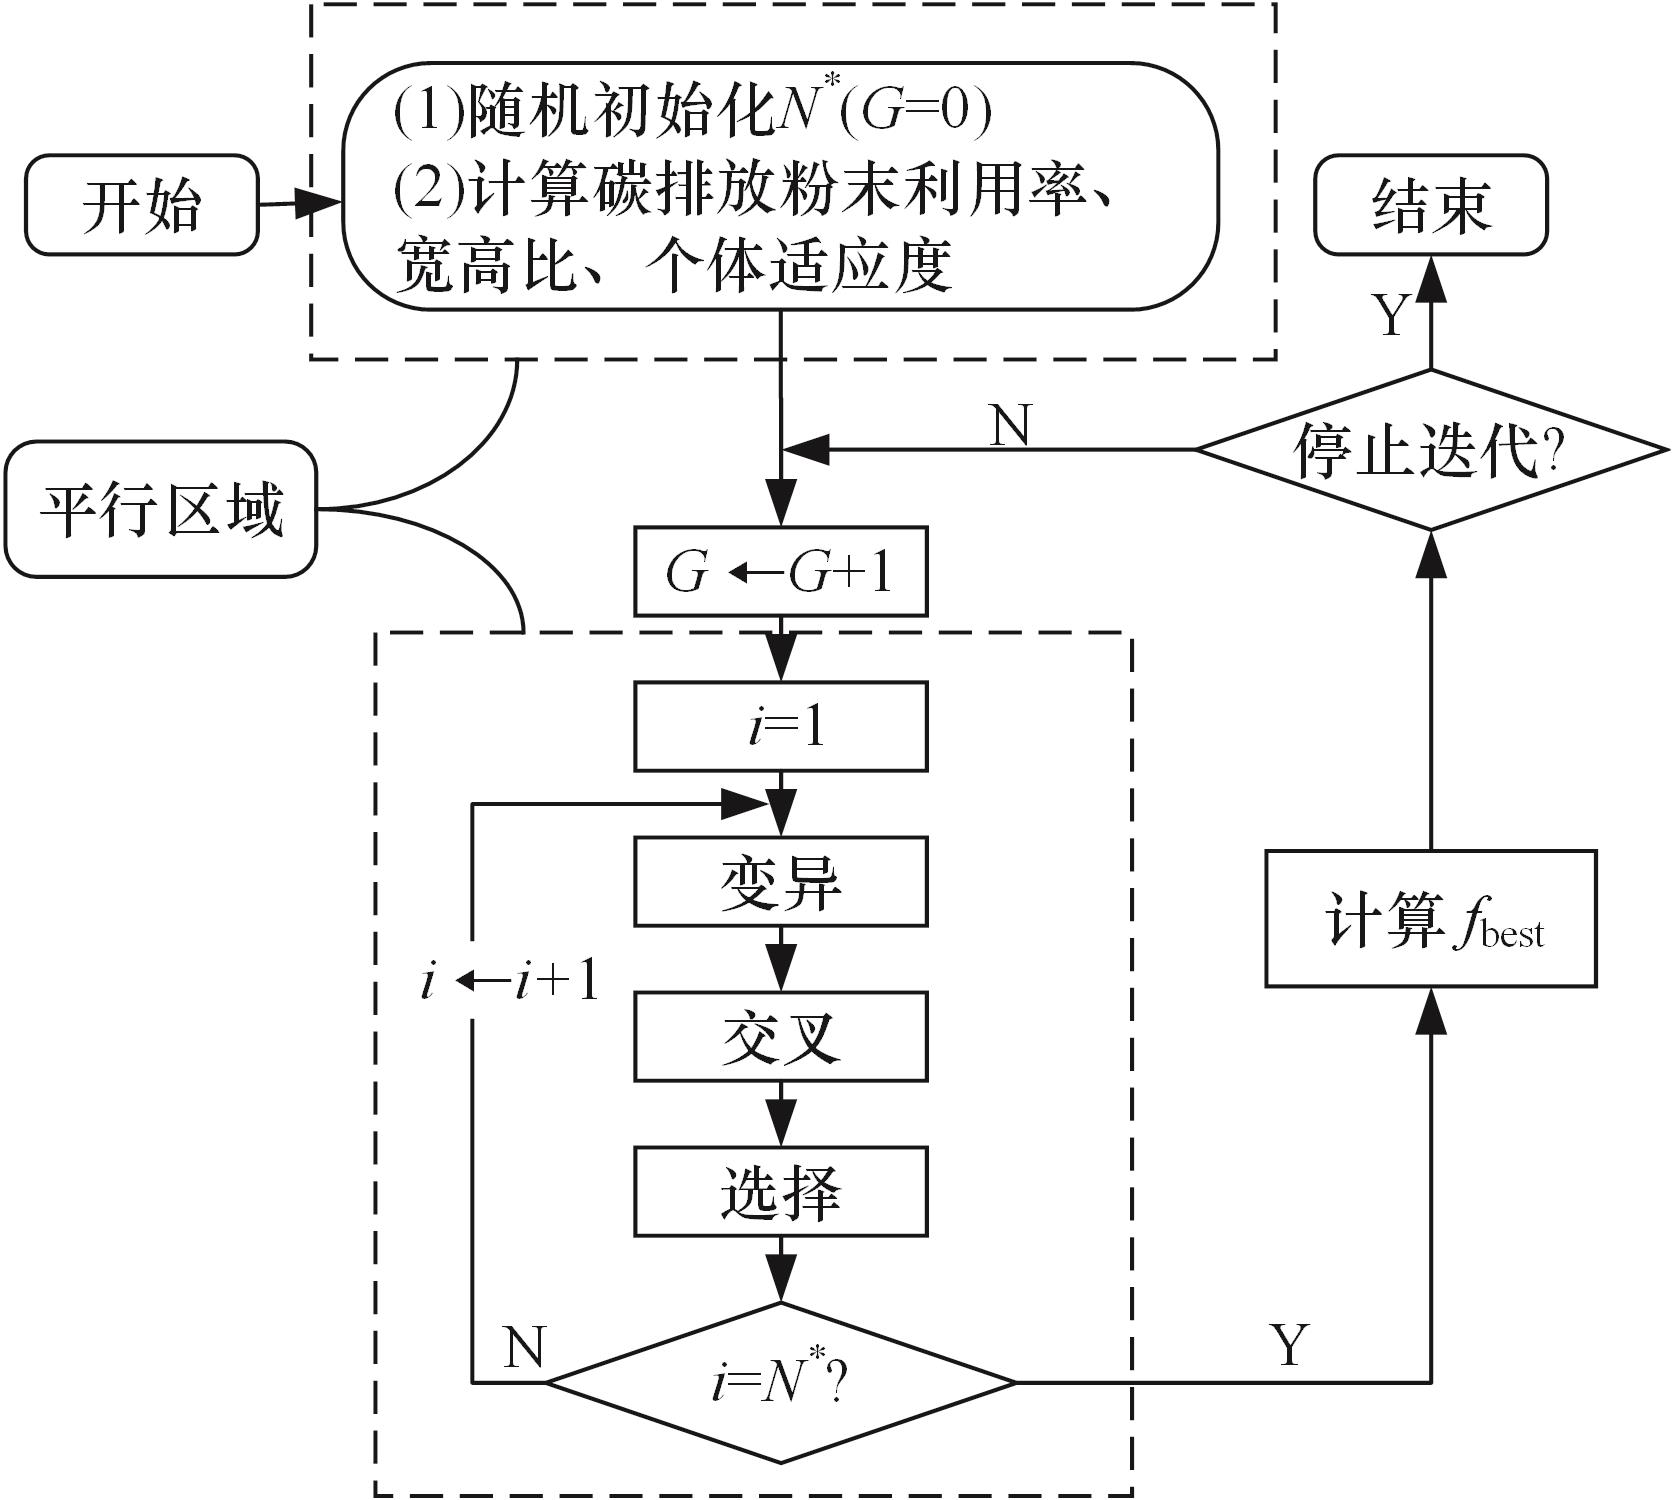
图3 局部变异策略
Fig.3 Local variation strategy
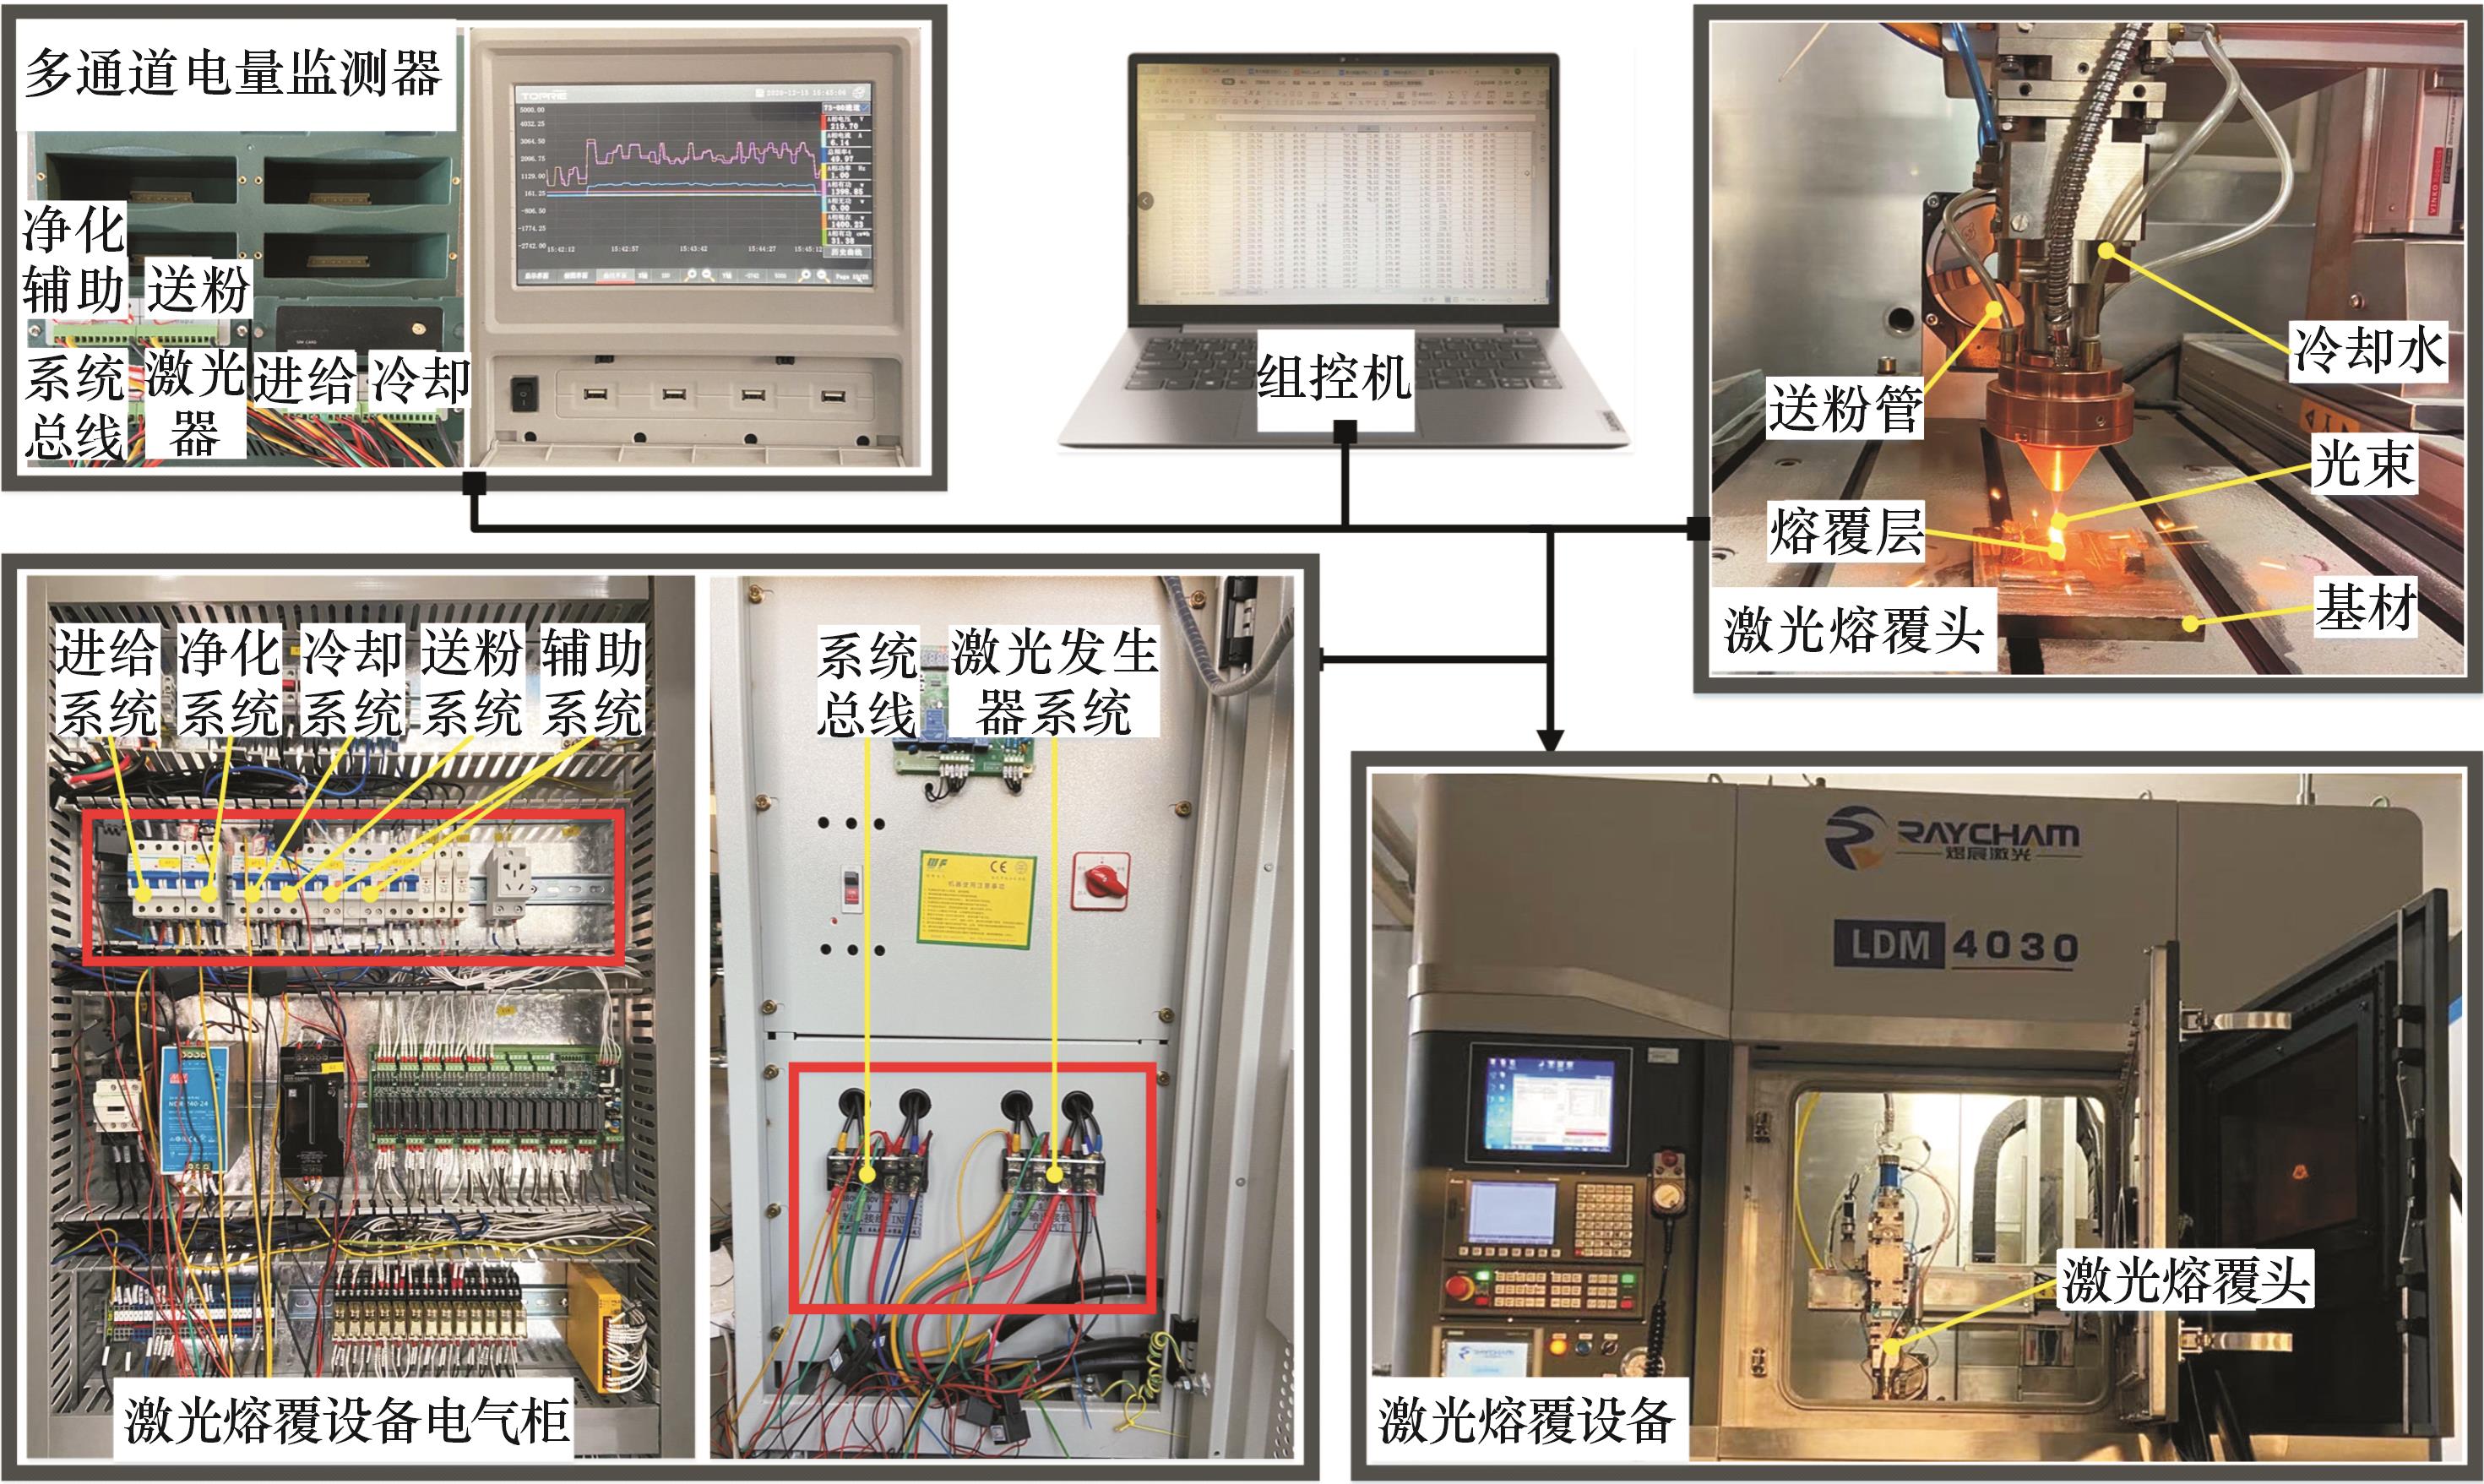
图4 激光熔覆碳排放监控平台
Fig.4 The carbon emission monitoring platform for the laser cladding
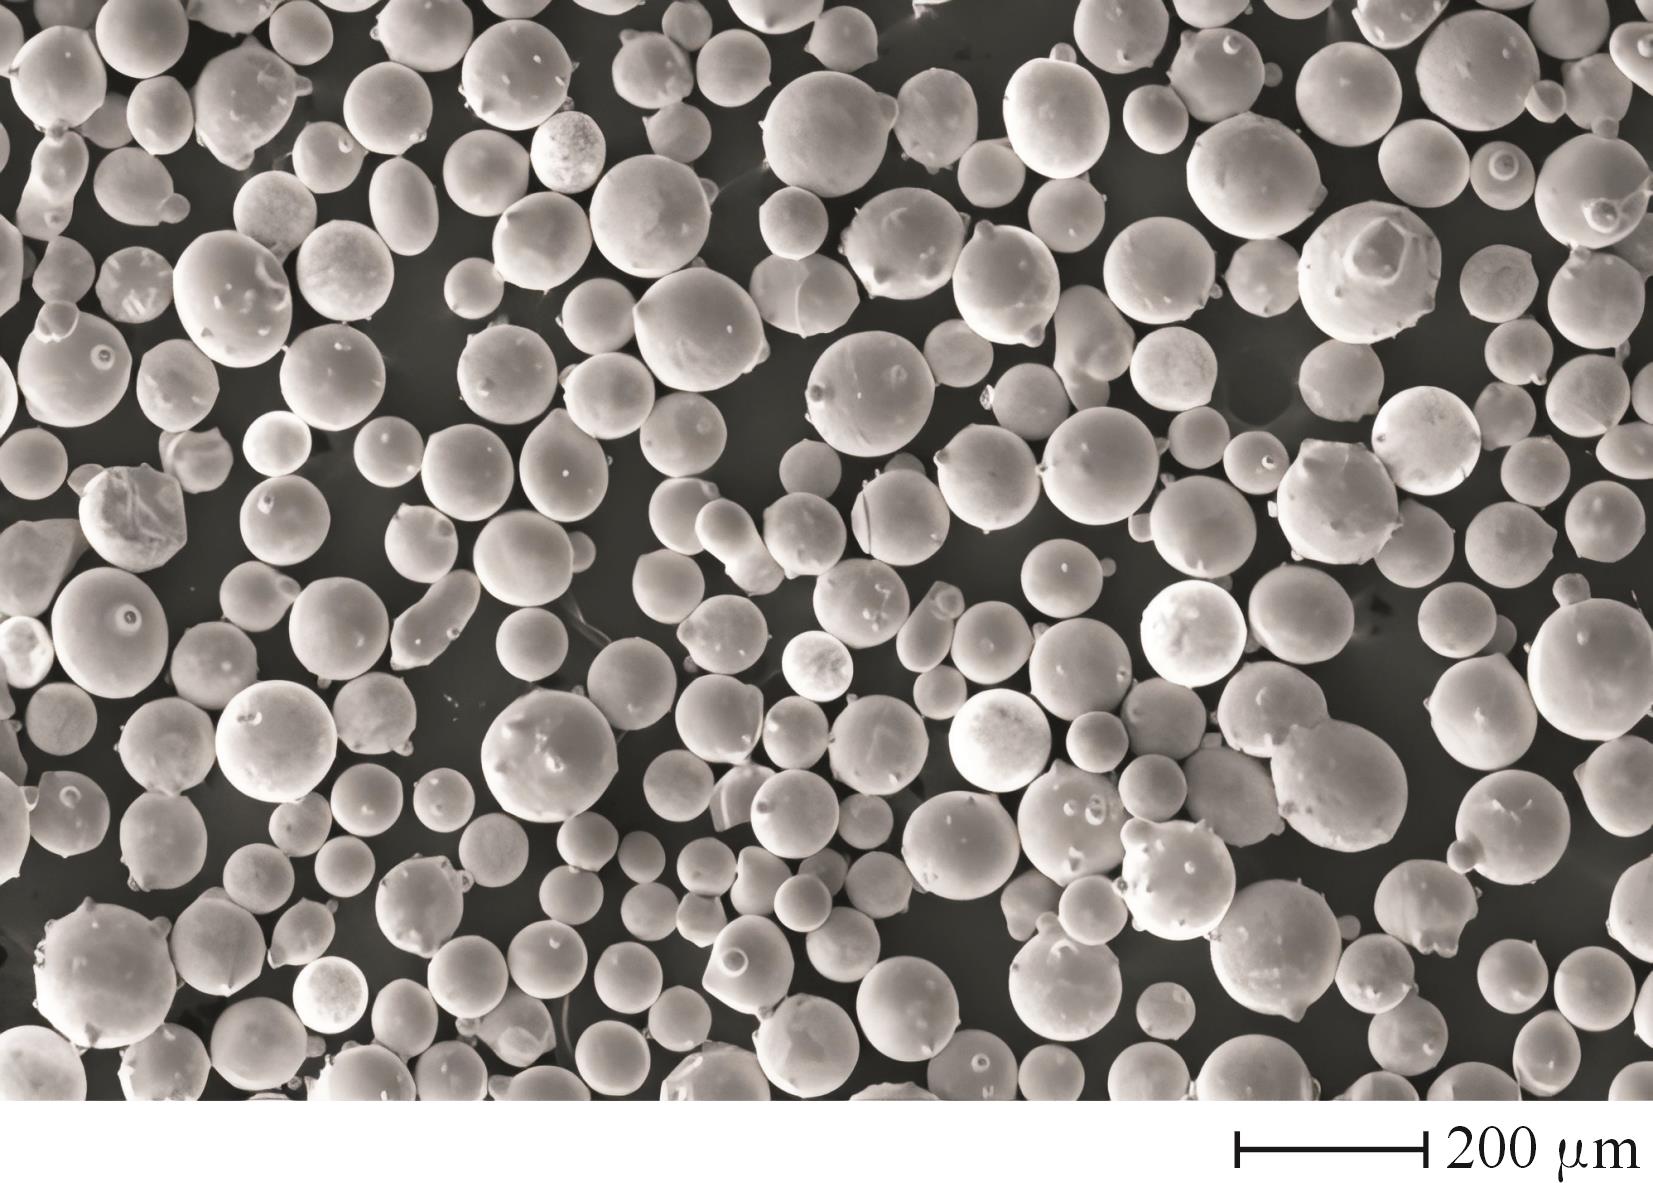
图5 Fe3O4 粉末的扫描电子显微镜(SEM)图像
Fig.5 SEM image of Fe3O4 powder
| w(C) | w(Mn) | w(Si) | w(P) | w(S) | w(Cr) | w(Ni) | w(Fe) |
|---|---|---|---|---|---|---|---|
| ≤0.07 | ≤0.20 | ≤0.10 | ≤0.035 | ≤0.03 | 0.17~ 0.19 | 0.08~ 0.11 | 其余 |
表1 Fe3O4合金粉末的化学成分(质量分数) (%)
Tab.1 Chemical composition of Fe3O4-based alloy powder (mass fraction)
| w(C) | w(Mn) | w(Si) | w(P) | w(S) | w(Cr) | w(Ni) | w(Fe) |
|---|---|---|---|---|---|---|---|
| ≤0.07 | ≤0.20 | ≤0.10 | ≤0.035 | ≤0.03 | 0.17~ 0.19 | 0.08~ 0.11 | 其余 |
| 参数 | 参数值 | 参数 | 参数值 |
|---|---|---|---|
| Plin | 300~900 W | Pli | 45 W |
| vf | 0.2~1.2 r/min | qk | 0.7 L/s |
| vs | 300~450 mm/min | 1×10³ kg/m3 | |
| c | 4.2×10³ J/(kg·K) | ||
| d | 2 mm | 1 K | |
| ti | 3 s | tp | 30 s |
| β | 50% | tg | 4 s |
表2 激光熔覆主要工艺参数
Tab. 2 Process parameters of laser remanufacturing
| 参数 | 参数值 | 参数 | 参数值 |
|---|---|---|---|
| Plin | 300~900 W | Pli | 45 W |
| vf | 0.2~1.2 r/min | qk | 0.7 L/s |
| vs | 300~450 mm/min | 1×10³ kg/m3 | |
| c | 4.2×10³ J/(kg·K) | ||
| d | 2 mm | 1 K | |
| ti | 3 s | tp | 30 s |
| β | 50% | tg | 4 s |
工艺 参数 | 1 | 2 | 3 | 4 | 5 | 6 | 7 |
|---|---|---|---|---|---|---|---|
| 450 | 500 | 550 | 600 | 650 | 700 | 750 | |
| 1465 | 1620 | 1771 | 1925 | 2076 | 2233 | 2387 |
表3 激光发生器子系统的功率变化 (W)
Tab.3 Power change of laser generator subsystem
工艺 参数 | 1 | 2 | 3 | 4 | 5 | 6 | 7 |
|---|---|---|---|---|---|---|---|
| 450 | 500 | 550 | 600 | 650 | 700 | 750 | |
| 1465 | 1620 | 1771 | 1925 | 2076 | 2233 | 2387 |
| 工艺参数 | 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 | 9 | 10 | 11 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 0.2 | 0.3 | 0.4 | 0.5 | 0.6 | 0.7 | 0.8 | 0.9 | 1.0 | 1.1 | 1.2 | |
| Ppm/W | 51.00 | 51.46 | 52.00 | 52.45 | 53.00 | 53.50 | 53.80 | 54.40 | 54.70 | 55.10 | 56.50 |
表4 送粉子系统功率变化
Tab.4 Power change of powder feeding subsystem
| 工艺参数 | 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 | 9 | 10 | 11 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 0.2 | 0.3 | 0.4 | 0.5 | 0.6 | 0.7 | 0.8 | 0.9 | 1.0 | 1.1 | 1.2 | |
| Ppm/W | 51.00 | 51.46 | 52.00 | 52.45 | 53.00 | 53.50 | 53.80 | 54.40 | 54.70 | 55.10 | 56.50 |
工艺 参数 | 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 | 9 |
|---|---|---|---|---|---|---|---|---|---|
| 320 | 330 | 340 | 350 | 360 | 370 | 380 | 390 | 400 | |
| Pmm/W | 55.1 | 55.3 | 55.3 | 55.4 | 55.5 | 55.7 | 56.1 | 56.1 | 56.3 |
表5 进给系统功率变化
Tab.5 Power variation of feed system
工艺 参数 | 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 | 9 |
|---|---|---|---|---|---|---|---|---|---|
| 320 | 330 | 340 | 350 | 360 | 370 | 380 | 390 | 400 | |
| Pmm/W | 55.1 | 55.3 | 55.3 | 55.4 | 55.5 | 55.7 | 56.1 | 56.1 | 56.3 |
| 激光装备子系统 | 待机功率 | 运行功率 |
|---|---|---|
| 激光发生系统 | 47 | |
| 送粉子系统 | 41 | |
| 输送子系统 | 50 | |
| 冷却子系统 | 1103 | 2371 |
| 照明系统 | 0 | 18 |
| 净化系统 | 0 | 25 |
表6 各子系统功率 (W)
Tab.6 Power of each subsystem
| 激光装备子系统 | 待机功率 | 运行功率 |
|---|---|---|
| 激光发生系统 | 47 | |
| 送粉子系统 | 41 | |
| 输送子系统 | 50 | |
| 冷却子系统 | 1103 | 2371 |
| 照明系统 | 0 | 18 |
| 净化系统 | 0 | 25 |
| 工艺参数 | 水平 | ||
|---|---|---|---|
| 600 | 700 | 800 | |
| vs/(mm·min-1) | 330 | 360 | 390 |
| 0.3 | 0.5 | 0.7 | |
表7 水平和因数表
Tab.7 Levels and factor
| 工艺参数 | 水平 | ||
|---|---|---|---|
| 600 | 700 | 800 | |
| vs/(mm·min-1) | 330 | 360 | 390 |
| 0.3 | 0.5 | 0.7 | |
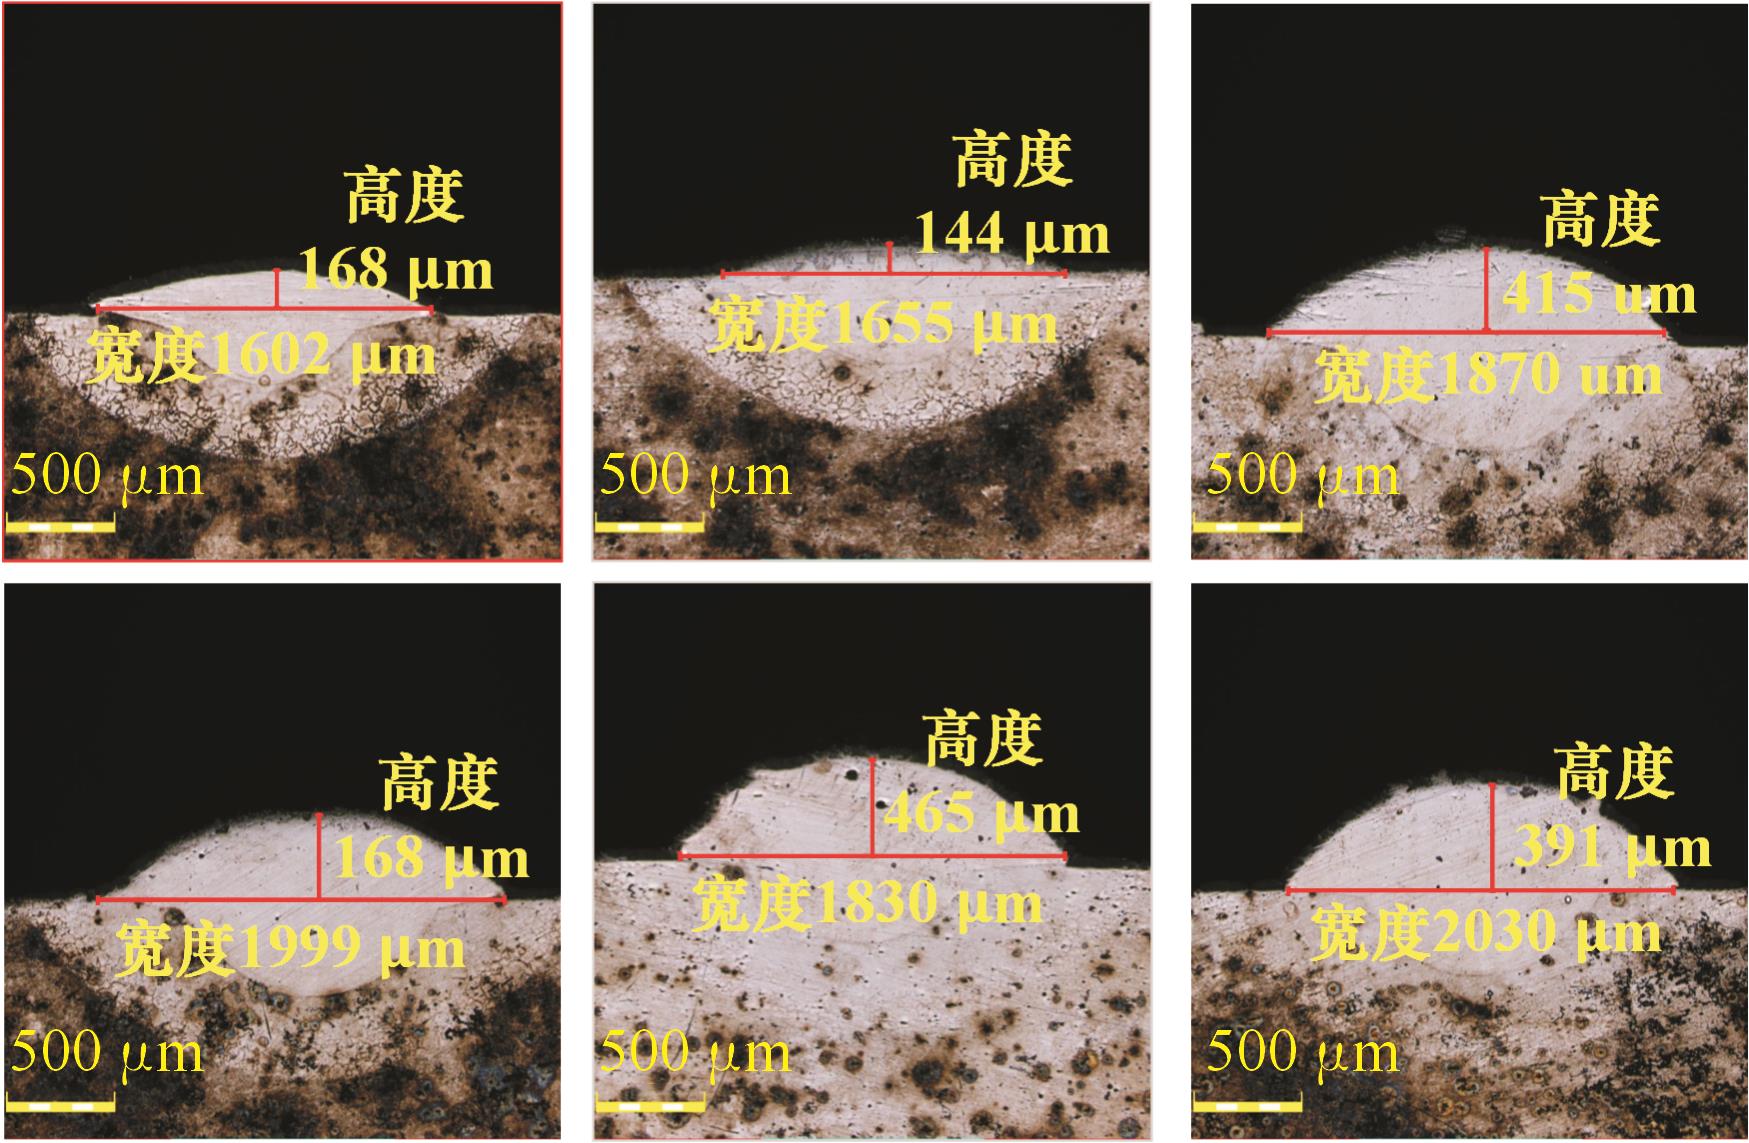
图6 部分熔覆层的高度和宽度
Fig.6 Height and width of the partial cladding layer
| 序号 | vs/(mm·min-1) | |||||||
|---|---|---|---|---|---|---|---|---|
| 1 | 600 | 0.5 | 330 | 1955 | 355 | 5.5 | 0.9000 | 0.34 |
| 2 | 700 | 0.7 | 390 | 2047 | 410 | 5.0 | 1.0470 | 0.30 |
| 3 | 700 | 0.3 | 390 | 2017 | 365 | 5.5 | 0.4653 | 0.31 |
| 4 | 700 | 0.3 | 330 | 2054 | 371 | 5.5 | 0.6469 | 0.42 |
| 5 | 600 | 0.7 | 360 | 1952 | 364 | 5.4 | 0.9616 | 0.28 |
| 6 | 700 | 0.5 | 360 | 2050 | 390 | 5.3 | 0.8263 | 0.36 |
| 7 | 800 | 0.5 | 360 | 2139 | 438 | 4.9 | 0.9689 | 0.42 |
| 8 | 600 | 0.3 | 390 | 1949 | 317 | 6.1 | 0.3337 | 0.19 |
| 9 | 700 | 0.5 | 330 | 2054 | 393 | 5.2 | 0.9500 | 0.39 |
| 10 | 800 | 0.7 | 330 | 2152 | 464 | 4.6 | 1.4086 | 0.39 |
| 11 | 600 | 0.7 | 390 | 1949 | 361 | 5.4 | 0.8466 | 0.21 |
| 12 | 800 | 0.7 | 360 | 2149 | 461 | 4.7 | 1.2467 | 0.39 |
| 13 | 600 | 0.3 | 330 | 1895 | 323 | 5.9 | 0.4914 | 0.35 |
| 14 | 600 | 0.7 | 330 | 1955 | 367 | 5.3 | 1.0976 | 0.33 |
| 15 | 700 | 0.3 | 360 | 2050 | 368 | 5.6 | 0.5485 | 0.38 |
| 16 | 700 | 0.7 | 360 | 2038 | 413 | 4.9 | 1.1042 | 0.34 |
| 17 | 800 | 0.7 | 390 | 2146 | 458 | 4.7 | 1.1098 | 0.37 |
| 18 | 800 | 0.5 | 330 | 2152 | 441 | 4.9 | 1.1055 | 0.43 |
| 19 | 700 | 0.5 | 390 | 2047 | 387 | 5.3 | 0.7217 | 0.30 |
| 20 | 800 | 0.3 | 390 | 2146 | 413 | 5.2 | 0.5968 | 0.41 |
| 21 | 700 | 0.7 | 330 | 2054 | 415 | 4.9 | 1.2531 | 0.37 |
| 22 | 600 | 0.3 | 360 | 2052 | 320 | 6.4 | 0.4060 | 0.28 |
| 23 | 600 | 0.5 | 390 | 1949 | 339 | 5.7 | 0.5901 | 0.20 |
| 24 | 800 | 0.5 | 390 | 2146 | 436 | 4.9 | 0.8533 | 0.39 |
| 25 | 600 | 0.5 | 360 | 1952 | 342 | 5.7 | 0.6838 | 0.27 |
| 26 | 800 | 0.3 | 330 | 2152 | 419 | 5.1 | 0.8024 | 0.48 |
| 27 | 800 | 0.3 | 360 | 2169 | 416 | 5.2 | 0.7024 | 0.45 |
表8 熔化高度和宽度尺寸以及粉末消耗记录
Tab.8 Melting height and width dimensions and powder gram consumption record
| 序号 | vs/(mm·min-1) | |||||||
|---|---|---|---|---|---|---|---|---|
| 1 | 600 | 0.5 | 330 | 1955 | 355 | 5.5 | 0.9000 | 0.34 |
| 2 | 700 | 0.7 | 390 | 2047 | 410 | 5.0 | 1.0470 | 0.30 |
| 3 | 700 | 0.3 | 390 | 2017 | 365 | 5.5 | 0.4653 | 0.31 |
| 4 | 700 | 0.3 | 330 | 2054 | 371 | 5.5 | 0.6469 | 0.42 |
| 5 | 600 | 0.7 | 360 | 1952 | 364 | 5.4 | 0.9616 | 0.28 |
| 6 | 700 | 0.5 | 360 | 2050 | 390 | 5.3 | 0.8263 | 0.36 |
| 7 | 800 | 0.5 | 360 | 2139 | 438 | 4.9 | 0.9689 | 0.42 |
| 8 | 600 | 0.3 | 390 | 1949 | 317 | 6.1 | 0.3337 | 0.19 |
| 9 | 700 | 0.5 | 330 | 2054 | 393 | 5.2 | 0.9500 | 0.39 |
| 10 | 800 | 0.7 | 330 | 2152 | 464 | 4.6 | 1.4086 | 0.39 |
| 11 | 600 | 0.7 | 390 | 1949 | 361 | 5.4 | 0.8466 | 0.21 |
| 12 | 800 | 0.7 | 360 | 2149 | 461 | 4.7 | 1.2467 | 0.39 |
| 13 | 600 | 0.3 | 330 | 1895 | 323 | 5.9 | 0.4914 | 0.35 |
| 14 | 600 | 0.7 | 330 | 1955 | 367 | 5.3 | 1.0976 | 0.33 |
| 15 | 700 | 0.3 | 360 | 2050 | 368 | 5.6 | 0.5485 | 0.38 |
| 16 | 700 | 0.7 | 360 | 2038 | 413 | 4.9 | 1.1042 | 0.34 |
| 17 | 800 | 0.7 | 390 | 2146 | 458 | 4.7 | 1.1098 | 0.37 |
| 18 | 800 | 0.5 | 330 | 2152 | 441 | 4.9 | 1.1055 | 0.43 |
| 19 | 700 | 0.5 | 390 | 2047 | 387 | 5.3 | 0.7217 | 0.30 |
| 20 | 800 | 0.3 | 390 | 2146 | 413 | 5.2 | 0.5968 | 0.41 |
| 21 | 700 | 0.7 | 330 | 2054 | 415 | 4.9 | 1.2531 | 0.37 |
| 22 | 600 | 0.3 | 360 | 2052 | 320 | 6.4 | 0.4060 | 0.28 |
| 23 | 600 | 0.5 | 390 | 1949 | 339 | 5.7 | 0.5901 | 0.20 |
| 24 | 800 | 0.5 | 390 | 2146 | 436 | 4.9 | 0.8533 | 0.39 |
| 25 | 600 | 0.5 | 360 | 1952 | 342 | 5.7 | 0.6838 | 0.27 |
| 26 | 800 | 0.3 | 330 | 2152 | 419 | 5.1 | 0.8024 | 0.48 |
| 27 | 800 | 0.3 | 360 | 2169 | 416 | 5.2 | 0.7024 | 0.45 |
| 送粉速度vf/(r·min-1) | 0.2 | 0.3 | 0.4 | 0.5 | 0.6 | 0.7 | 0.8 | 0.9 | 1.0 | 1.1 | 1.2 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 送粉速率vg/(g·min-1) | 3.66 | 4.66 | 5.54 | 6.49 | 7.54 | 9.26 | 10.80 | 12.05 | 13.24 | 14.48 | 15.72 |
表9 与送粉速度相对应的送粉速率
Tab.9 Powder feed rate corresponding to powder bed rotation speed
| 送粉速度vf/(r·min-1) | 0.2 | 0.3 | 0.4 | 0.5 | 0.6 | 0.7 | 0.8 | 0.9 | 1.0 | 1.1 | 1.2 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| 送粉速率vg/(g·min-1) | 3.66 | 4.66 | 5.54 | 6.49 | 7.54 | 9.26 | 10.80 | 12.05 | 13.24 | 14.48 | 15.72 |
| 序号 | (r·min-1) | (mm·min-1) | 碳排放 | 宽高比 | 粉末利用率 | |||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 预测/g | 实际/g | 误差/% | 预测 | 实际 | 误差/% | 预测/% | 实际/% | 误差/% | ||||
| 1 | 450 | 0.2 | 250 | 87.4 | 90.00 | 3 | 6.1 | 6.2 | 2 | 43.87 | 45.45 | 3 |
| 2 | 450 | 0.5 | 300 | 73.5 | 75.60 | 5 | 6.1 | 5.9 | 4 | 29.93 | 30.65 | 2 |
| 3 | 450 | 0.6 | 350 | 63.6 | 66.09 | 4 | 6.4 | 6.9 | 8 | 16.05 | 17.08 | 6 |
| 4 | 450 | 0.8 | 400 | 56.2 | 58.78 | 4 | 6.1 | 6.0 | 1 | 2.11 | 2.23 | 5 |
| 5 | 550 | 0.2 | 300 | 82.6 | 84.00 | 2 | 6.2 | 6.3 | 1 | 39.04 | 41.04 | 5 |
| 6 | 550 | 0.5 | 250 | 98.3 | 103.00 | 5 | 4.8 | 4.6 | 5 | 43.00 | 44.45 | 3 |
| 7 | 550 | 0.6 | 400 | 63.1 | 62.20 | 1 | 5.8 | 6.0 | 3 | 11.56 | 10.78 | 7 |
| 8 | 550 | 0.8 | 350 | 71.5 | 70.60 | 1 | 5.4 | 5.6 | 3 | 26.43 | 27.98 | 6 |
| 9 | 650 | 0.2 | 350 | 79.2 | 78.50 | 1 | 6.0 | 6.2 | 3 | 36.21 | 37.45 | 3 |
| 10 | 650 | 0.5 | 400 | 69.9 | 68.00 | 3 | 5.4 | 5.6 | 3 | 22.78 | 24.32 | 6 |
| 11 | 650 | 0.6 | 250 | 109.3 | 111.00 | 1 | 4.3 | 4.5 | 5 | 41.03 | 42.03 | 2 |
| 12 | 650 | 0.8 | 300 | 91.8 | 92.00 | 2 | 4.7 | 4.5 | 4 | 36.75 | 34.95 | 5 |
| 13 | 750 | 0.2 | 400 | 76.7 | 75.00 | 2 | 5.5 | 5.7 | 4 | 35.38 | 33.89 | 4 |
| 14 | 750 | 0.5 | 350 | 87.1 | 85.00 | 2 | 5.0 | 5.2 | 4 | 39.85 | 40.55 | 2 |
| 15 | 750 | 0.6 | 300 | 100.9 | 103.00 | 2 | 4.6 | 4.7 | 2 | 40.54 | 42.54 | 5 |
| 16 | 750 | 0.8 | 250 | 120.3 | 122.00 | 1 | 3.9 | 4.0 | 4 | 33.07 | 30.07 | 8 |
表10 预测值和实际值
Tab.10 Analysis table of predicted and actual values
| 序号 | (r·min-1) | (mm·min-1) | 碳排放 | 宽高比 | 粉末利用率 | |||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 预测/g | 实际/g | 误差/% | 预测 | 实际 | 误差/% | 预测/% | 实际/% | 误差/% | ||||
| 1 | 450 | 0.2 | 250 | 87.4 | 90.00 | 3 | 6.1 | 6.2 | 2 | 43.87 | 45.45 | 3 |
| 2 | 450 | 0.5 | 300 | 73.5 | 75.60 | 5 | 6.1 | 5.9 | 4 | 29.93 | 30.65 | 2 |
| 3 | 450 | 0.6 | 350 | 63.6 | 66.09 | 4 | 6.4 | 6.9 | 8 | 16.05 | 17.08 | 6 |
| 4 | 450 | 0.8 | 400 | 56.2 | 58.78 | 4 | 6.1 | 6.0 | 1 | 2.11 | 2.23 | 5 |
| 5 | 550 | 0.2 | 300 | 82.6 | 84.00 | 2 | 6.2 | 6.3 | 1 | 39.04 | 41.04 | 5 |
| 6 | 550 | 0.5 | 250 | 98.3 | 103.00 | 5 | 4.8 | 4.6 | 5 | 43.00 | 44.45 | 3 |
| 7 | 550 | 0.6 | 400 | 63.1 | 62.20 | 1 | 5.8 | 6.0 | 3 | 11.56 | 10.78 | 7 |
| 8 | 550 | 0.8 | 350 | 71.5 | 70.60 | 1 | 5.4 | 5.6 | 3 | 26.43 | 27.98 | 6 |
| 9 | 650 | 0.2 | 350 | 79.2 | 78.50 | 1 | 6.0 | 6.2 | 3 | 36.21 | 37.45 | 3 |
| 10 | 650 | 0.5 | 400 | 69.9 | 68.00 | 3 | 5.4 | 5.6 | 3 | 22.78 | 24.32 | 6 |
| 11 | 650 | 0.6 | 250 | 109.3 | 111.00 | 1 | 4.3 | 4.5 | 5 | 41.03 | 42.03 | 2 |
| 12 | 650 | 0.8 | 300 | 91.8 | 92.00 | 2 | 4.7 | 4.5 | 4 | 36.75 | 34.95 | 5 |
| 13 | 750 | 0.2 | 400 | 76.7 | 75.00 | 2 | 5.5 | 5.7 | 4 | 35.38 | 33.89 | 4 |
| 14 | 750 | 0.5 | 350 | 87.1 | 85.00 | 2 | 5.0 | 5.2 | 4 | 39.85 | 40.55 | 2 |
| 15 | 750 | 0.6 | 300 | 100.9 | 103.00 | 2 | 4.6 | 4.7 | 2 | 40.54 | 42.54 | 5 |
| 16 | 750 | 0.8 | 250 | 120.3 | 122.00 | 1 | 3.9 | 4.0 | 4 | 33.07 | 30.07 | 8 |
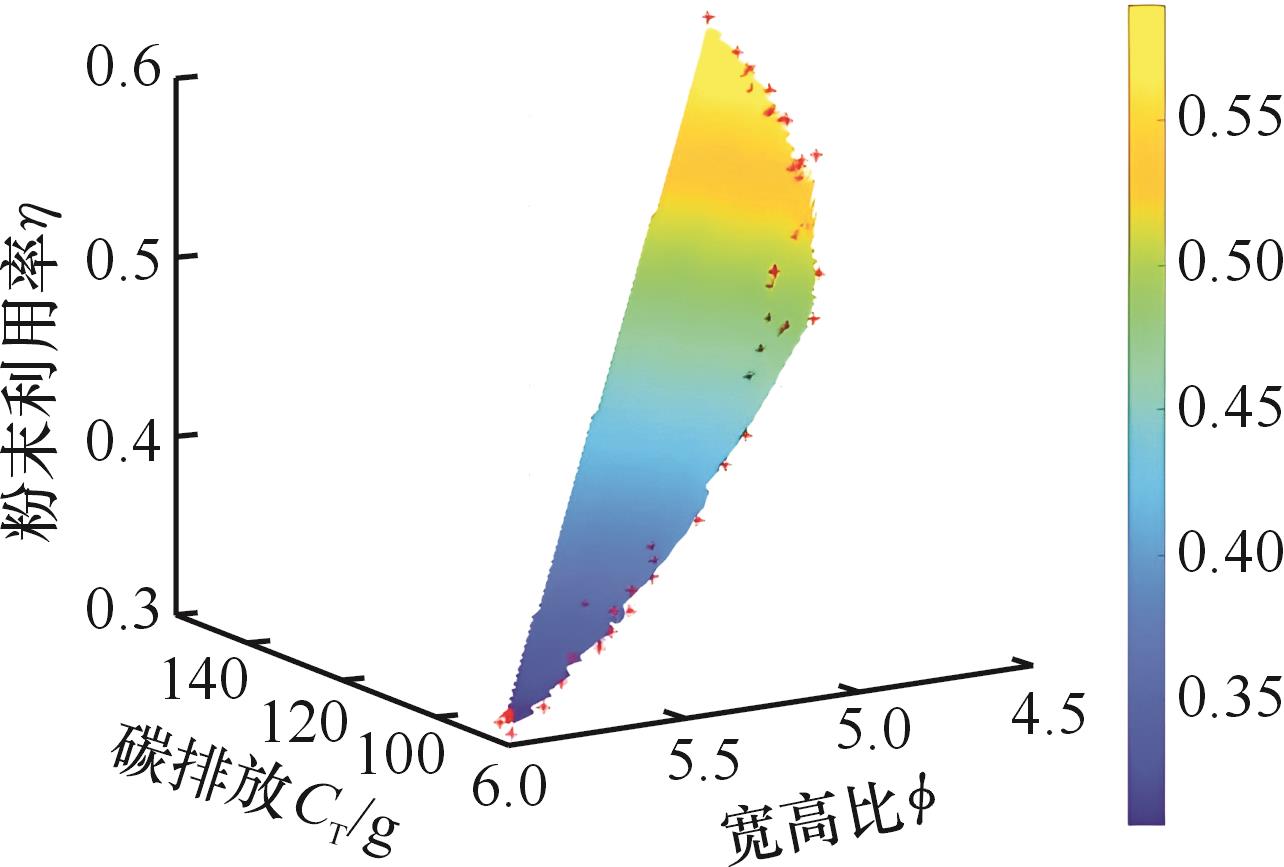
图7 帕累托前沿
Fig.7 Pareto front
| 指标 | 原始GDE3 | 改进GDE3 |
|---|---|---|
| HV | 0.120 | 0.124 |
| IGD | 0.298 | 0.276 |
| GD | 0.534 | 0.517 |
| Spacing | 0.698 | 0.683 |
| 时间 | 0.722 | 0.658 |
表11 算法性能评估
Tab.11 Performance evaluation of algorithms
| 指标 | 原始GDE3 | 改进GDE3 |
|---|---|---|
| HV | 0.120 | 0.124 |
| IGD | 0.298 | 0.276 |
| GD | 0.534 | 0.517 |
| Spacing | 0.698 | 0.683 |
| 时间 | 0.722 | 0.658 |
| 种群大小 | 迭代次数 | 改进GDE3 | GDE3 | NSGA-Ⅱ | NSGA-Ⅲ | CMOPSO | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|---|
| 200 | 200 | 0.1257 | 0.1207 | 0.1182 | 0.1177 | 0.1195 | 0.1179 | 0.1197 | 0.1176 | 0.1197 |
| 200 | 150 | 0.1231 | 0.1207 | 0.1188 | 0.1180 | 0.1194 | 0.1205 | 0.1196 | 0.1180 | 0.1195 |
| 200 | 50 | 0.1224 | 0.1205 | 0.1195 | 0.1164 | 0.1197 | 0.1200 | 0.1196 | 0.1177 | 0.1194 |
| 150 | 200 | 0.1245 | 0.1205 | 0.1184 | 0.1167 | 0.1187 | 0.1164 | 0.1193 | 0.1180 | 0.1189 |
| 150 | 150 | 0.1235 | 0.1205 | 0.1180 | 0.1176 | 0.1191 | 0.1166 | 0.1197 | 0.1190 | 0.1189 |
| 150 | 50 | 0.1230 | 0.1200 | 0.1180 | 0.1147 | 0.1195 | 0.1138 | 0.1194 | 0.1187 | 0.1187 |
| 100 | 200 | 0.1231 | 0.1201 | 0.1181 | 0.1143 | 0.1183 | 0.1117 | 0.1188 | 0.1169 | 0.1179 |
| 100 | 150 | 0.1231 | 0.1197 | 0.1188 | 0.1140 | 0.1160 | 0.1142 | 0.1187 | 0.1163 | 0.1177 |
| 100 | 50 | 0.1227 | 0.1191 | 0.1157 | 0.1128 | 0.1180 | 0.1066 | 0.1180 | 0.1152 | 0.1171 |
表12 不同参数组合的HV值
Tab.12 HV values for different parameter combinations
| 种群大小 | 迭代次数 | 改进GDE3 | GDE3 | NSGA-Ⅱ | NSGA-Ⅲ | CMOPSO | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|---|
| 200 | 200 | 0.1257 | 0.1207 | 0.1182 | 0.1177 | 0.1195 | 0.1179 | 0.1197 | 0.1176 | 0.1197 |
| 200 | 150 | 0.1231 | 0.1207 | 0.1188 | 0.1180 | 0.1194 | 0.1205 | 0.1196 | 0.1180 | 0.1195 |
| 200 | 50 | 0.1224 | 0.1205 | 0.1195 | 0.1164 | 0.1197 | 0.1200 | 0.1196 | 0.1177 | 0.1194 |
| 150 | 200 | 0.1245 | 0.1205 | 0.1184 | 0.1167 | 0.1187 | 0.1164 | 0.1193 | 0.1180 | 0.1189 |
| 150 | 150 | 0.1235 | 0.1205 | 0.1180 | 0.1176 | 0.1191 | 0.1166 | 0.1197 | 0.1190 | 0.1189 |
| 150 | 50 | 0.1230 | 0.1200 | 0.1180 | 0.1147 | 0.1195 | 0.1138 | 0.1194 | 0.1187 | 0.1187 |
| 100 | 200 | 0.1231 | 0.1201 | 0.1181 | 0.1143 | 0.1183 | 0.1117 | 0.1188 | 0.1169 | 0.1179 |
| 100 | 150 | 0.1231 | 0.1197 | 0.1188 | 0.1140 | 0.1160 | 0.1142 | 0.1187 | 0.1163 | 0.1177 |
| 100 | 50 | 0.1227 | 0.1191 | 0.1157 | 0.1128 | 0.1180 | 0.1066 | 0.1180 | 0.1152 | 0.1171 |
| 种群大小 | 迭代次数 | 改进GDE3 | GDE3 | NSGA-Ⅱ | NSGA-Ⅲ | CMOPSO | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|---|
| 200 | 200 | 0.1706 | 0.1807 | 0.2039 | 0.9006 | 0.2958 | 1.0211 | 0.3092 | 0.2373 | 0.3333 |
| 200 | 150 | 0.1760 | 0.1845 | 0.2080 | 1.2204 | 0.2944 | 1.2093 | 0.2798 | 0.3169 | 0.3528 |
| 200 | 50 | 0.1877 | 0.1906 | 0.2120 | 1.3374 | 0.2696 | 1.0900 | 0.3526 | 0.3626 | 0.5551 |
| 150 | 200 | 0.2045 | 0.2146 | 0.2437 | 0.7526 | 0.3714 | 1.2614 | 0.5921 | 0.3613 | 0.3896 |
| 150 | 150 | 0.2003 | 0.2136 | 0.2578 | 0.9966 | 0.3523 | 1.0941 | 0.4582 | 0.4743 | 0.3432 |
| 150 | 50 | 0.2206 | 0.2387 | 0.3401 | 1.5039 | 0.3533 | 1.3595 | 0.4741 | 0.5081 | 0.3995 |
| 100 | 200 | 0.2945 | 0.3142 | 0.3625 | 1.3260 | 0.4782 | 1.1390 | 0.4792 | 0.7204 | 0.5456 |
| 100 | 150 | 0.3194 | 0.3297 | 0.4161 | 1.8002 | 0.5070 | 1.1731 | 0.4830 | 0.6311 | 0.5680 |
| 100 | 50 | 0.3044 | 0.3154 | 0.3801 | 1.6657 | 0.4451 | 1.4481 | 0.5155 | 0.5356 | 0.6651 |
表13 不同参数组合的IGD值
Tab.13 IGD values for different parameter combinations
| 种群大小 | 迭代次数 | 改进GDE3 | GDE3 | NSGA-Ⅱ | NSGA-Ⅲ | CMOPSO | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|---|
| 200 | 200 | 0.1706 | 0.1807 | 0.2039 | 0.9006 | 0.2958 | 1.0211 | 0.3092 | 0.2373 | 0.3333 |
| 200 | 150 | 0.1760 | 0.1845 | 0.2080 | 1.2204 | 0.2944 | 1.2093 | 0.2798 | 0.3169 | 0.3528 |
| 200 | 50 | 0.1877 | 0.1906 | 0.2120 | 1.3374 | 0.2696 | 1.0900 | 0.3526 | 0.3626 | 0.5551 |
| 150 | 200 | 0.2045 | 0.2146 | 0.2437 | 0.7526 | 0.3714 | 1.2614 | 0.5921 | 0.3613 | 0.3896 |
| 150 | 150 | 0.2003 | 0.2136 | 0.2578 | 0.9966 | 0.3523 | 1.0941 | 0.4582 | 0.4743 | 0.3432 |
| 150 | 50 | 0.2206 | 0.2387 | 0.3401 | 1.5039 | 0.3533 | 1.3595 | 0.4741 | 0.5081 | 0.3995 |
| 100 | 200 | 0.2945 | 0.3142 | 0.3625 | 1.3260 | 0.4782 | 1.1390 | 0.4792 | 0.7204 | 0.5456 |
| 100 | 150 | 0.3194 | 0.3297 | 0.4161 | 1.8002 | 0.5070 | 1.1731 | 0.4830 | 0.6311 | 0.5680 |
| 100 | 50 | 0.3044 | 0.3154 | 0.3801 | 1.6657 | 0.4451 | 1.4481 | 0.5155 | 0.5356 | 0.6651 |
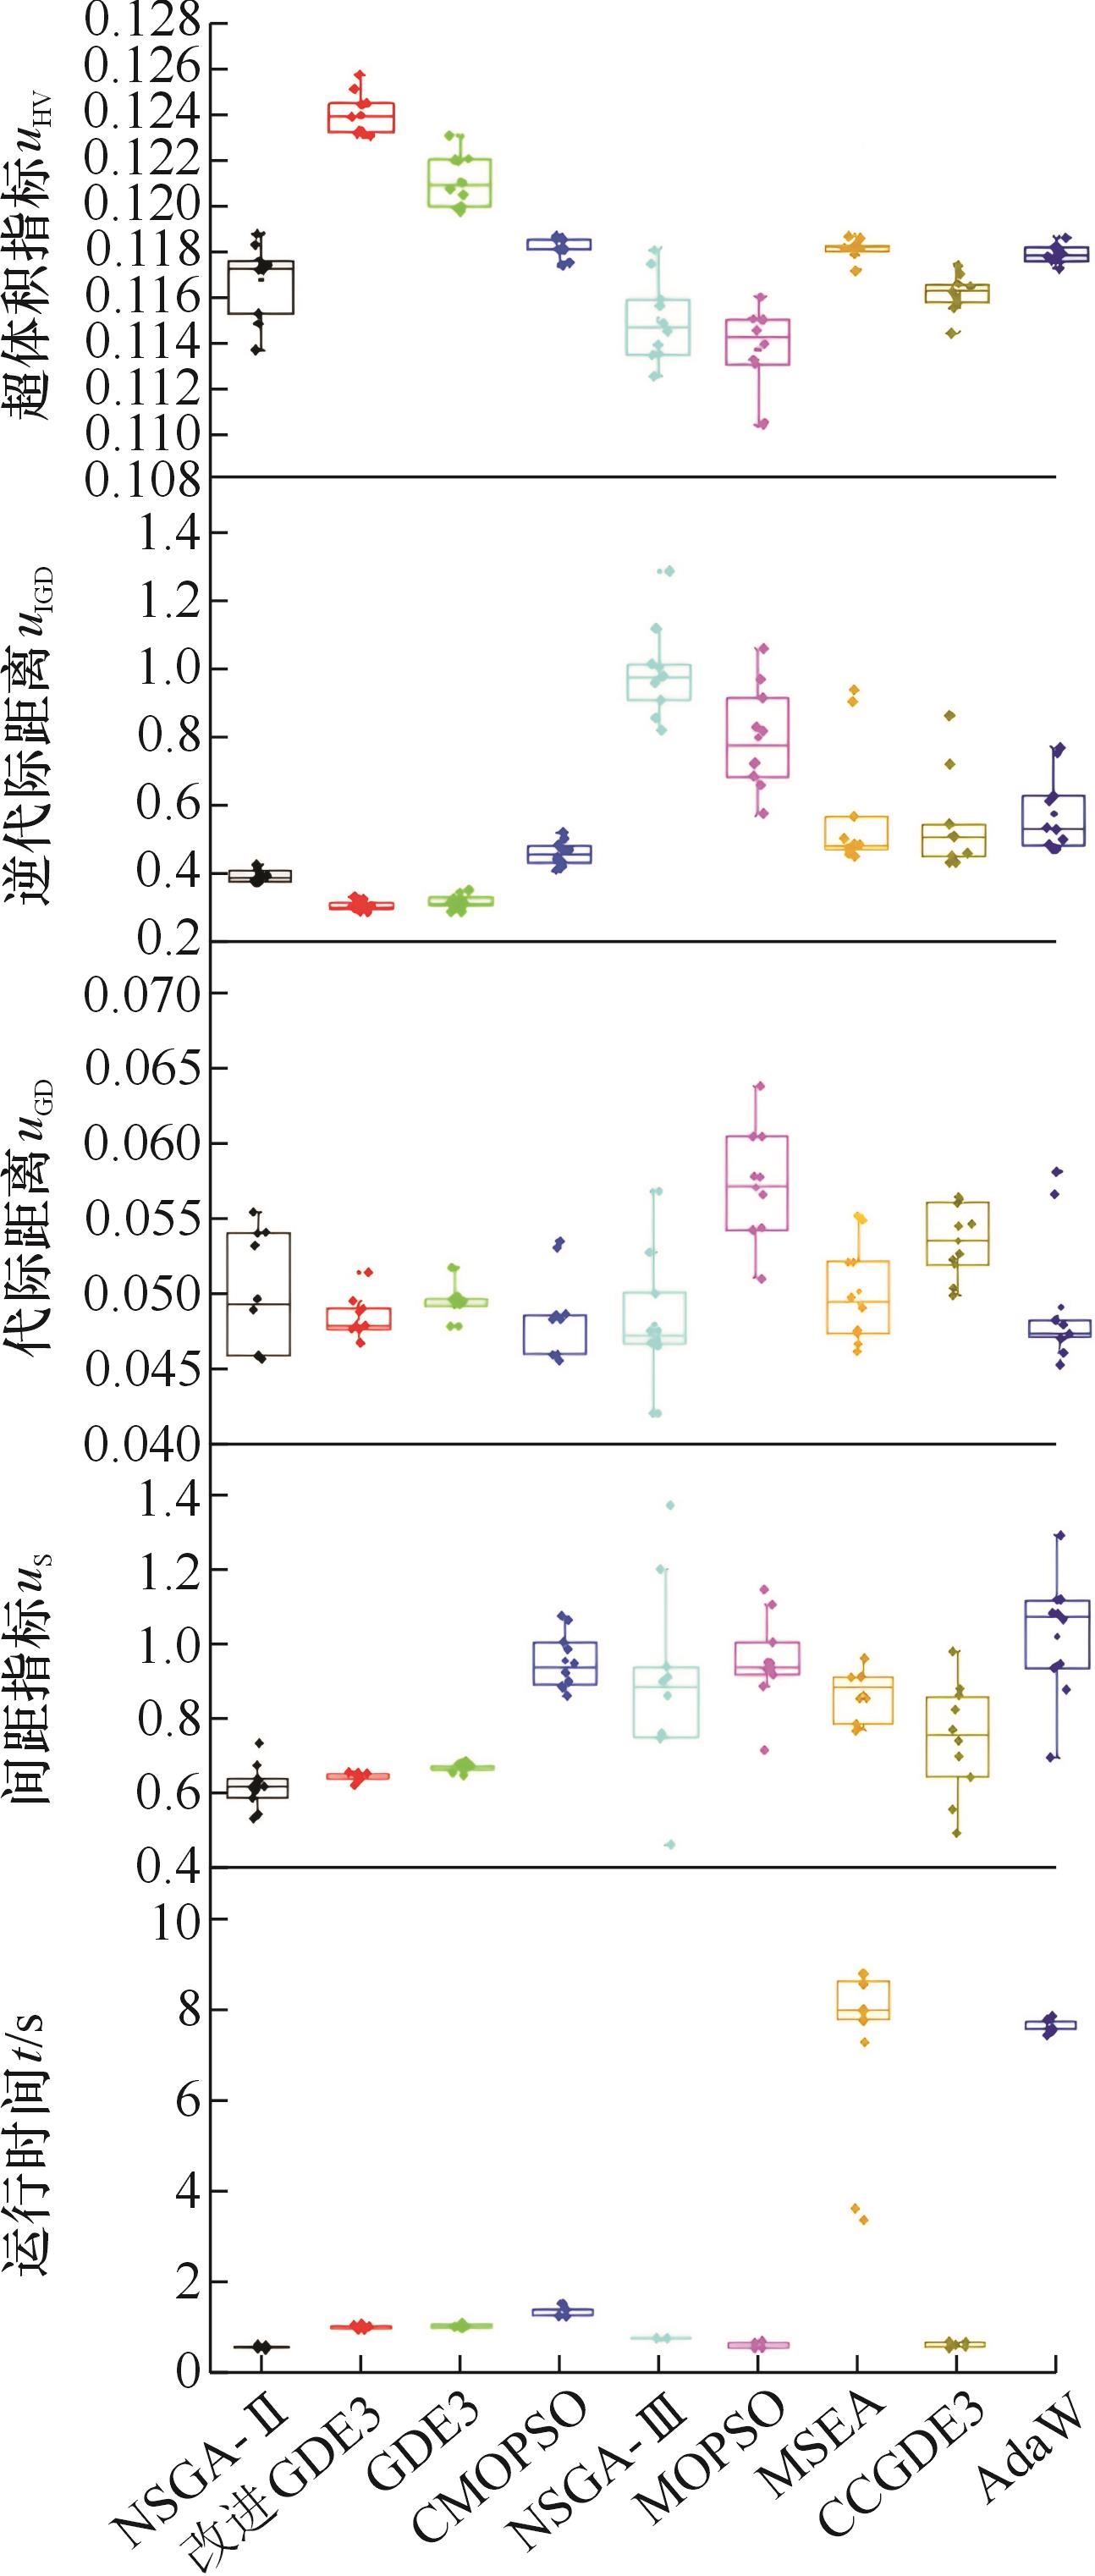
图8 各算法箱线图分析
Fig.8 Comparison box line diagram
| 指标 | NSGA-Ⅱ | 改进GDE3 | GDE3 | CMOPSO | NSGA-Ⅲ | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|
| HV | 0.116 783 | 0.124 044 | 0.123 992 | 0.118 190 | 0.115 001 | 0.113 702 | 0.118 143 | 0.116 195 | 0.117 886 |
| IGD | 0.392 496 | 0.306 155 | 0.315 485 | 0.455 973 | 0.990 612 | 0.794 283 | 0.571 219 | 0.541 170 | 0.573 158 |
| GD | 0.049 896 | 0.047 850 | 0.049 358 | 0.047 926 | 0.049 170 | 0.056 666 | 0.048 536 | 0.053 175 | 0.048 786 |
| Spacing | 0.631 471 | 0.654 635 | 0.676 761 | 0.957 632 | 0.896 569 | 0.955 735 | 0.873 143 | 0.755 528 | 1.023 198 |
| 时间/s | 0.241 710 | 0.657 990 | 0.721 960 | 1.031 230 | 0.499 310 | 0.353 980 | 8.334 900 | 0.313 600 | 7.722 720 |
表14 评价指数平均值比较
Tab.14 Evaluation index mean comparison
| 指标 | NSGA-Ⅱ | 改进GDE3 | GDE3 | CMOPSO | NSGA-Ⅲ | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|
| HV | 0.116 783 | 0.124 044 | 0.123 992 | 0.118 190 | 0.115 001 | 0.113 702 | 0.118 143 | 0.116 195 | 0.117 886 |
| IGD | 0.392 496 | 0.306 155 | 0.315 485 | 0.455 973 | 0.990 612 | 0.794 283 | 0.571 219 | 0.541 170 | 0.573 158 |
| GD | 0.049 896 | 0.047 850 | 0.049 358 | 0.047 926 | 0.049 170 | 0.056 666 | 0.048 536 | 0.053 175 | 0.048 786 |
| Spacing | 0.631 471 | 0.654 635 | 0.676 761 | 0.957 632 | 0.896 569 | 0.955 735 | 0.873 143 | 0.755 528 | 1.023 198 |
| 时间/s | 0.241 710 | 0.657 990 | 0.721 960 | 1.031 230 | 0.499 310 | 0.353 980 | 8.334 900 | 0.313 600 | 7.722 720 |
| 指标 | NSGA-Ⅱ | 改进GDE3 | GDE3 | CMOPSO | NSGA-Ⅲ | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|
| HV | 0.000 003 | 0.000 001 | 0 | 0 | 0.000 003 | 0.000 004 | 4.760 000 | 0.000 001 | 0 |
| IGD | 0.000 298 | 0.000 200 | 0.000 384 | 0.001 330 | 0.018 000 | 0.028 800 | 0 | 0.019 600 | 0.012 500 |
| GD | 0.000 016 | 0.000 002 | 0.000 011 | 0.000 022 | 0.000 018 | 0.000 018 | 0.003 500 | 0.000 006 | 0.000 020 |
| Spacing | 0.003 240 | 0.000 104 | 0.000 116 | 0.005 240 | 0.061 600 | 0.013 400 | 0.000 016 | 0.021 400 | 0.025 300 |
| 时间/s | 0.000 210 | 0.000 207 | 0.000 655 | 0.002 480 | 0.000 360 | 0.000 171 | 0.004 490 | 0.000 210 | 0.007 400 |
表15 方差分析
Tab.15 Metric variance
| 指标 | NSGA-Ⅱ | 改进GDE3 | GDE3 | CMOPSO | NSGA-Ⅲ | MOPSO | MSEA | CCGDE3 | AdaW |
|---|---|---|---|---|---|---|---|---|---|
| HV | 0.000 003 | 0.000 001 | 0 | 0 | 0.000 003 | 0.000 004 | 4.760 000 | 0.000 001 | 0 |
| IGD | 0.000 298 | 0.000 200 | 0.000 384 | 0.001 330 | 0.018 000 | 0.028 800 | 0 | 0.019 600 | 0.012 500 |
| GD | 0.000 016 | 0.000 002 | 0.000 011 | 0.000 022 | 0.000 018 | 0.000 018 | 0.003 500 | 0.000 006 | 0.000 020 |
| Spacing | 0.003 240 | 0.000 104 | 0.000 116 | 0.005 240 | 0.061 600 | 0.013 400 | 0.000 016 | 0.021 400 | 0.025 300 |
| 时间/s | 0.000 210 | 0.000 207 | 0.000 655 | 0.002 480 | 0.000 360 | 0.000 171 | 0.004 490 | 0.000 210 | 0.007 400 |
| 算法 | Plin/W | vs/(mm·min-1) | vf/(r·min-1) | 碳排放量/g | 宽高比 | 粉末利用率/% |
|---|---|---|---|---|---|---|
| 改进GDE3 | 615 | 400 | 0.5 | 88.600 | 5.71 | 19.6 |
| 637 | 390 | 0.6 | 92.800 | 5.50 | 24.6 | |
| 658 | 412 | 0.4 | 90.000 | 5.73 | 20.6 | |
| GDE3 | 634 | 400 | 0.6 | 99.829 | 5.30 | 21.4 |
| 682 | 399 | 0.7 | 103.191 | 5.00 | 26.3 | |
| 610 | 399 | 0.6 | 98.157 | 5.40 | 18.8 | |
| CCGDE3 | 669 | 409 | 0.8 | 99.920 | 4.75 | 24.5 |
| 627 | 406 | 0.9 | 97.680 | 4.91 | 21.0 | |
| 573 | 408 | 0.9 | 93.600 | 5.17 | 16.0 | |
| NSGA-Ⅱ | 524 | 410 | 0.8 | 89.800 | 5.40 | 9.7 |
| 456 | 410 | 0.4 | 85.000 | 6.80 | 2.0 | |
| 629 | 409 | 0.9 | 97.000 | 4.80 | 20.0 | |
| NSGA-Ⅲ | 568 | 409 | 0.7 | 92.800 | 5.10 | 14.0 |
| 621 | 410 | 0.6 | 96.400 | 4.90 | 20.0 | |
| 686 | 410 | 0.7 | 101.300 | 4.60 | 26.0 | |
| MOPSO | 487 | 390 | 0.6 | 87.300 | 5.70 | 4.4 |
| 717 | 409 | 0.6 | 103.300 | 4.50 | 28.6 | |
| 606 | 409 | 0.7 | 95.500 | 5.00 | 18.7 | |
| CMOPSO | 659 | 410 | 0.7 | 99.150 | 4.76 | 24.0 |
| 558 | 380 | 0.8 | 92.210 | 5.24 | 4.0 | |
| 585 | 400 | 0.9 | 94.030 | 5.10 | 17.0 | |
| MSEA | 644 | 399 | 0.6 | 100.500 | 5.40 | 22.0 |
| 613 | 400 | 0.6 | 98.300 | 5.40 | 19.0 | |
| 625 | 394 | 0.7 | 100.500 | 5.40 | 37.0 | |
| AdaW | 688 | 410 | 0.9 | 101.140 | 4.65 | 26.0 |
| 551 | 409 | 0.9 | 91.750 | 5.27 | 13.0 | |
| 596 | 420 | 0.2 | 86.000 | 6.65 | 19.0 |
表16 优化算法的部分结果
Tab.16 Partial results of the optimization algorithm
| 算法 | Plin/W | vs/(mm·min-1) | vf/(r·min-1) | 碳排放量/g | 宽高比 | 粉末利用率/% |
|---|---|---|---|---|---|---|
| 改进GDE3 | 615 | 400 | 0.5 | 88.600 | 5.71 | 19.6 |
| 637 | 390 | 0.6 | 92.800 | 5.50 | 24.6 | |
| 658 | 412 | 0.4 | 90.000 | 5.73 | 20.6 | |
| GDE3 | 634 | 400 | 0.6 | 99.829 | 5.30 | 21.4 |
| 682 | 399 | 0.7 | 103.191 | 5.00 | 26.3 | |
| 610 | 399 | 0.6 | 98.157 | 5.40 | 18.8 | |
| CCGDE3 | 669 | 409 | 0.8 | 99.920 | 4.75 | 24.5 |
| 627 | 406 | 0.9 | 97.680 | 4.91 | 21.0 | |
| 573 | 408 | 0.9 | 93.600 | 5.17 | 16.0 | |
| NSGA-Ⅱ | 524 | 410 | 0.8 | 89.800 | 5.40 | 9.7 |
| 456 | 410 | 0.4 | 85.000 | 6.80 | 2.0 | |
| 629 | 409 | 0.9 | 97.000 | 4.80 | 20.0 | |
| NSGA-Ⅲ | 568 | 409 | 0.7 | 92.800 | 5.10 | 14.0 |
| 621 | 410 | 0.6 | 96.400 | 4.90 | 20.0 | |
| 686 | 410 | 0.7 | 101.300 | 4.60 | 26.0 | |
| MOPSO | 487 | 390 | 0.6 | 87.300 | 5.70 | 4.4 |
| 717 | 409 | 0.6 | 103.300 | 4.50 | 28.6 | |
| 606 | 409 | 0.7 | 95.500 | 5.00 | 18.7 | |
| CMOPSO | 659 | 410 | 0.7 | 99.150 | 4.76 | 24.0 |
| 558 | 380 | 0.8 | 92.210 | 5.24 | 4.0 | |
| 585 | 400 | 0.9 | 94.030 | 5.10 | 17.0 | |
| MSEA | 644 | 399 | 0.6 | 100.500 | 5.40 | 22.0 |
| 613 | 400 | 0.6 | 98.300 | 5.40 | 19.0 | |
| 625 | 394 | 0.7 | 100.500 | 5.40 | 37.0 | |
| AdaW | 688 | 410 | 0.9 | 101.140 | 4.65 | 26.0 |
| 551 | 409 | 0.9 | 91.750 | 5.27 | 13.0 | |
| 596 | 420 | 0.2 | 86.000 | 6.65 | 19.0 |
| 637,390,0.6 | 92.8,24%,5.5 | 2.63 |
| 777,420,0.2 | 98.7,34%,5.59 | 2.55 |
| 658,412,0.4 | 90.0,20%,5.73 | 2.51 |
| 604,420,0.5 | 83.7,11%,5.82 | 2.48 |
| 632,418,0.6 | 86.5,16%,5.50 | 2.47 |
| 615,400,0.5 | 88.6,19%,5.71 | 2.32 |
| 795,419,0.2 | 100.5,36%,5.51 | 2.32 |
表17 灰色关联度
Tab.17 Grey correlation degree
| 637,390,0.6 | 92.8,24%,5.5 | 2.63 |
| 777,420,0.2 | 98.7,34%,5.59 | 2.55 |
| 658,412,0.4 | 90.0,20%,5.73 | 2.51 |
| 604,420,0.5 | 83.7,11%,5.82 | 2.48 |
| 632,418,0.6 | 86.5,16%,5.50 | 2.47 |
| 615,400,0.5 | 88.6,19%,5.71 | 2.32 |
| 795,419,0.2 | 100.5,36%,5.51 | 2.32 |
| 方案 | 优化目标 | Plin/W | vs/(mm·min-1) | vf/(r·min-1) | CT/g | ||
|---|---|---|---|---|---|---|---|
| 1 | CT | 300 | 450 | 0.2 | 53.9±3.2 | 3%±0.05% | 8.0±0.09 |
| 2 | 895 | 300 | 0.6 | 150.8±3.0 | 39%±1.5% | 4.48±0.050 | |
| 3 | 595 | 400 | 0.4 | 86.8±3.5 | 16%±1.4% | 6.0±0.08 | |
| 4 | 637 | 390 | 0.6 | 92.7±6.3 | 23%±2.0% | 5.5±0.07 | |
| 5 | 经验值 | 692 | 410 | 0.7 | 111.8±2.0 | 17%±2.2% | 5.3±0.06 |
表18 优化结果对比
Tab.18 Comparison of optimization results
| 方案 | 优化目标 | Plin/W | vs/(mm·min-1) | vf/(r·min-1) | CT/g | ||
|---|---|---|---|---|---|---|---|
| 1 | CT | 300 | 450 | 0.2 | 53.9±3.2 | 3%±0.05% | 8.0±0.09 |
| 2 | 895 | 300 | 0.6 | 150.8±3.0 | 39%±1.5% | 4.48±0.050 | |
| 3 | 595 | 400 | 0.4 | 86.8±3.5 | 16%±1.4% | 6.0±0.08 | |
| 4 | 637 | 390 | 0.6 | 92.7±6.3 | 23%±2.0% | 5.5±0.07 | |
| 5 | 经验值 | 692 | 410 | 0.7 | 111.8±2.0 | 17%±2.2% | 5.3±0.06 |
| 优化目标 | 优化值 | 经验值 | 优化幅度 |
|---|---|---|---|
| 碳排放 | 221.7±4.2 | 295.3±3.5 | 25% |
| 粉末利用率 | 15.0±1.1 | 12.1±0.9 | 19% |
| 宽高比 | 5.3±0.03 | 5.5±0.04 | 6% |
表19 优化前后对比
Tab.19 Comparison of before and after optimization
| 优化目标 | 优化值 | 经验值 | 优化幅度 |
|---|---|---|---|
| 碳排放 | 221.7±4.2 | 295.3±3.5 | 25% |
| 粉末利用率 | 15.0±1.1 | 12.1±0.9 | 19% |
| 宽高比 | 5.3±0.03 | 5.5±0.04 | 6% |
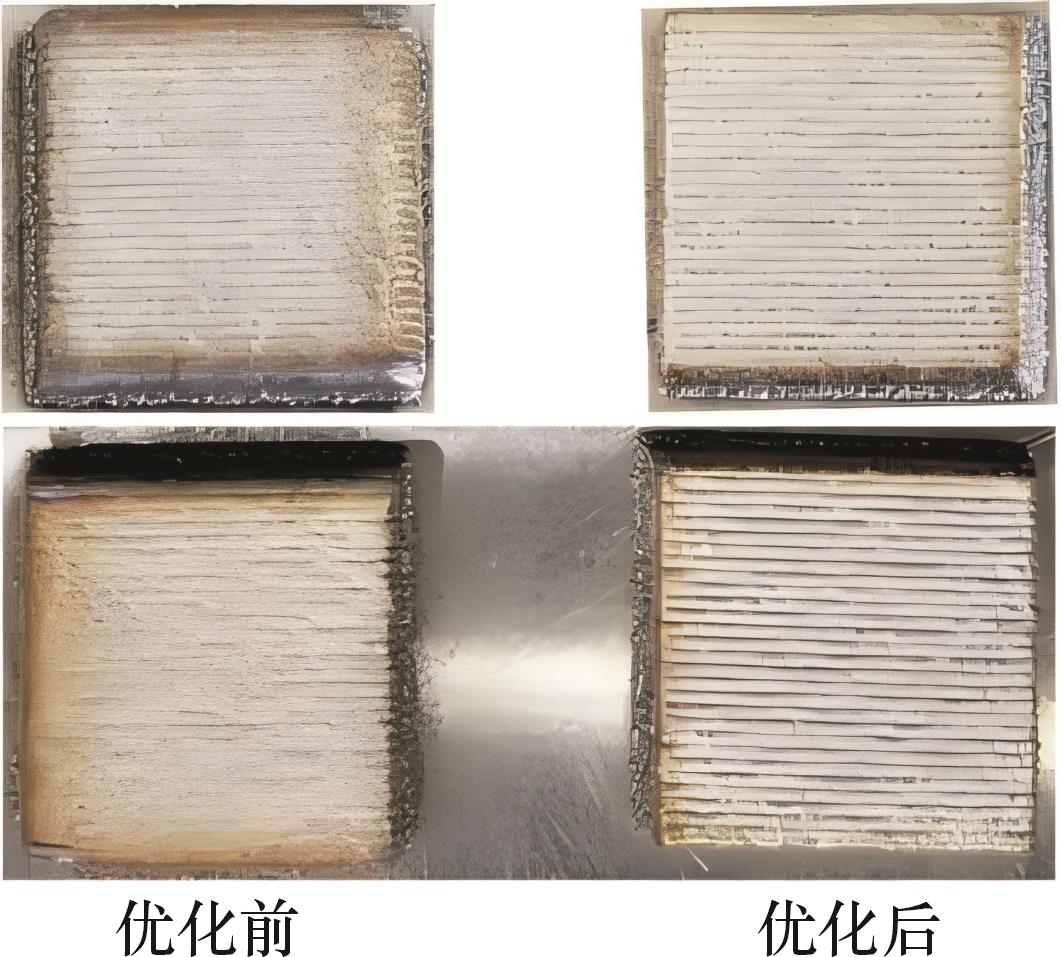
图9 样品宏观形貌对比
Fig.9 Morphology comparison of components
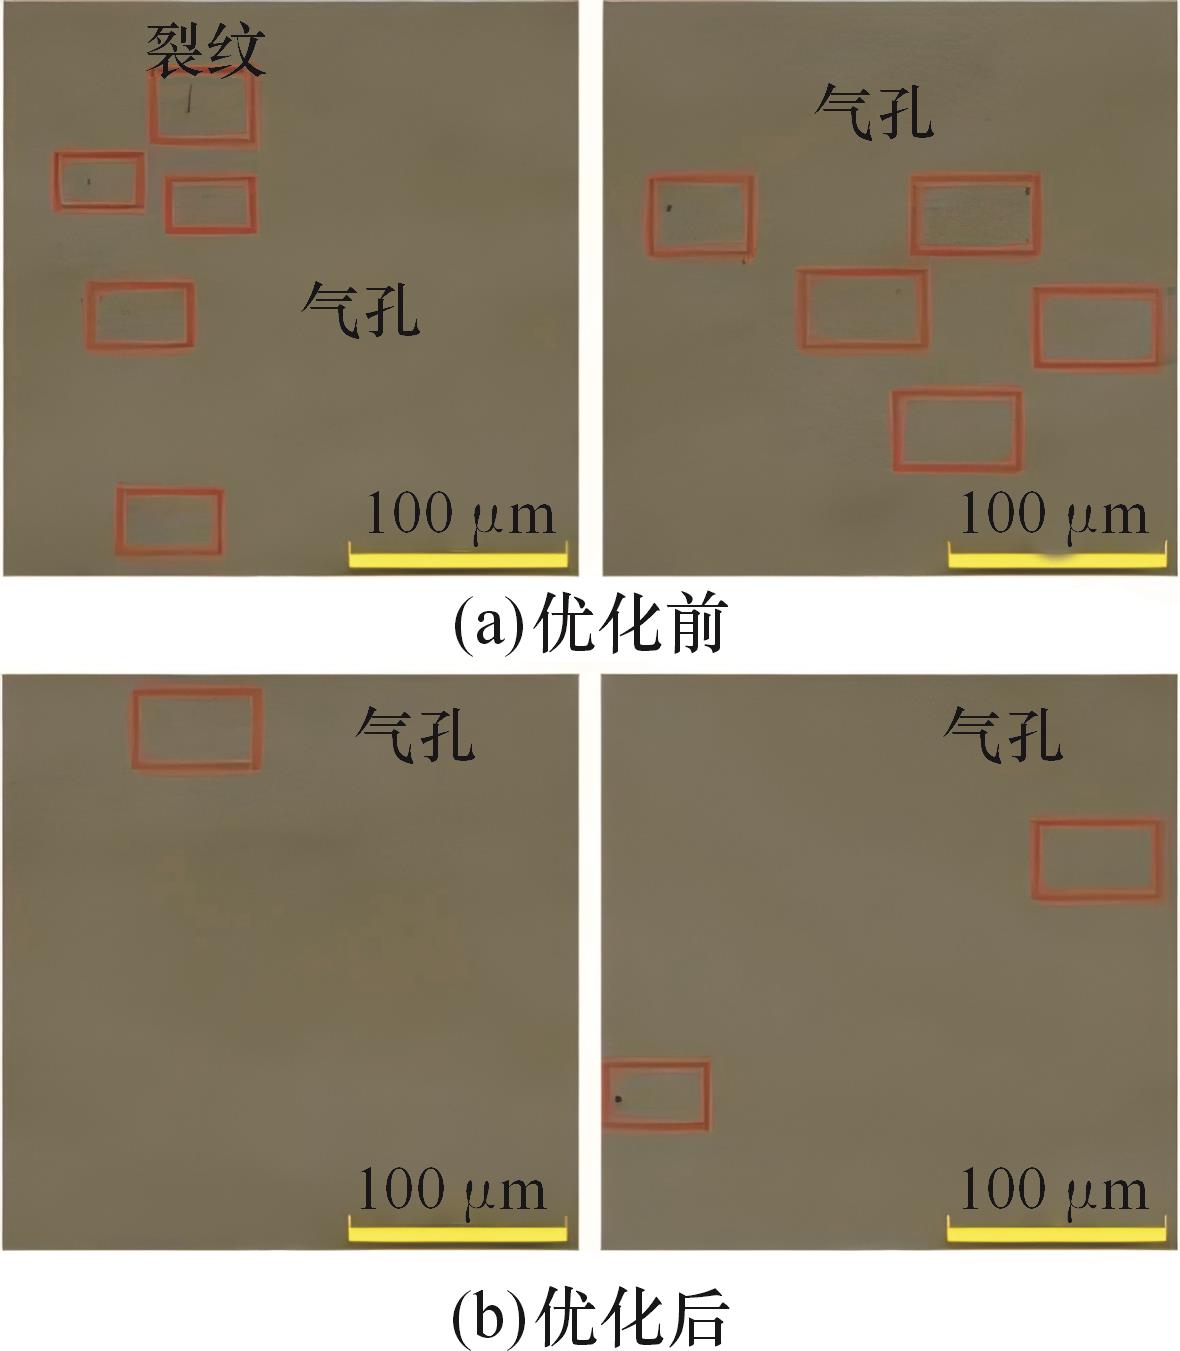
图10 样品内部气孔对比
Fig.10 Comparison of internal porosity of component
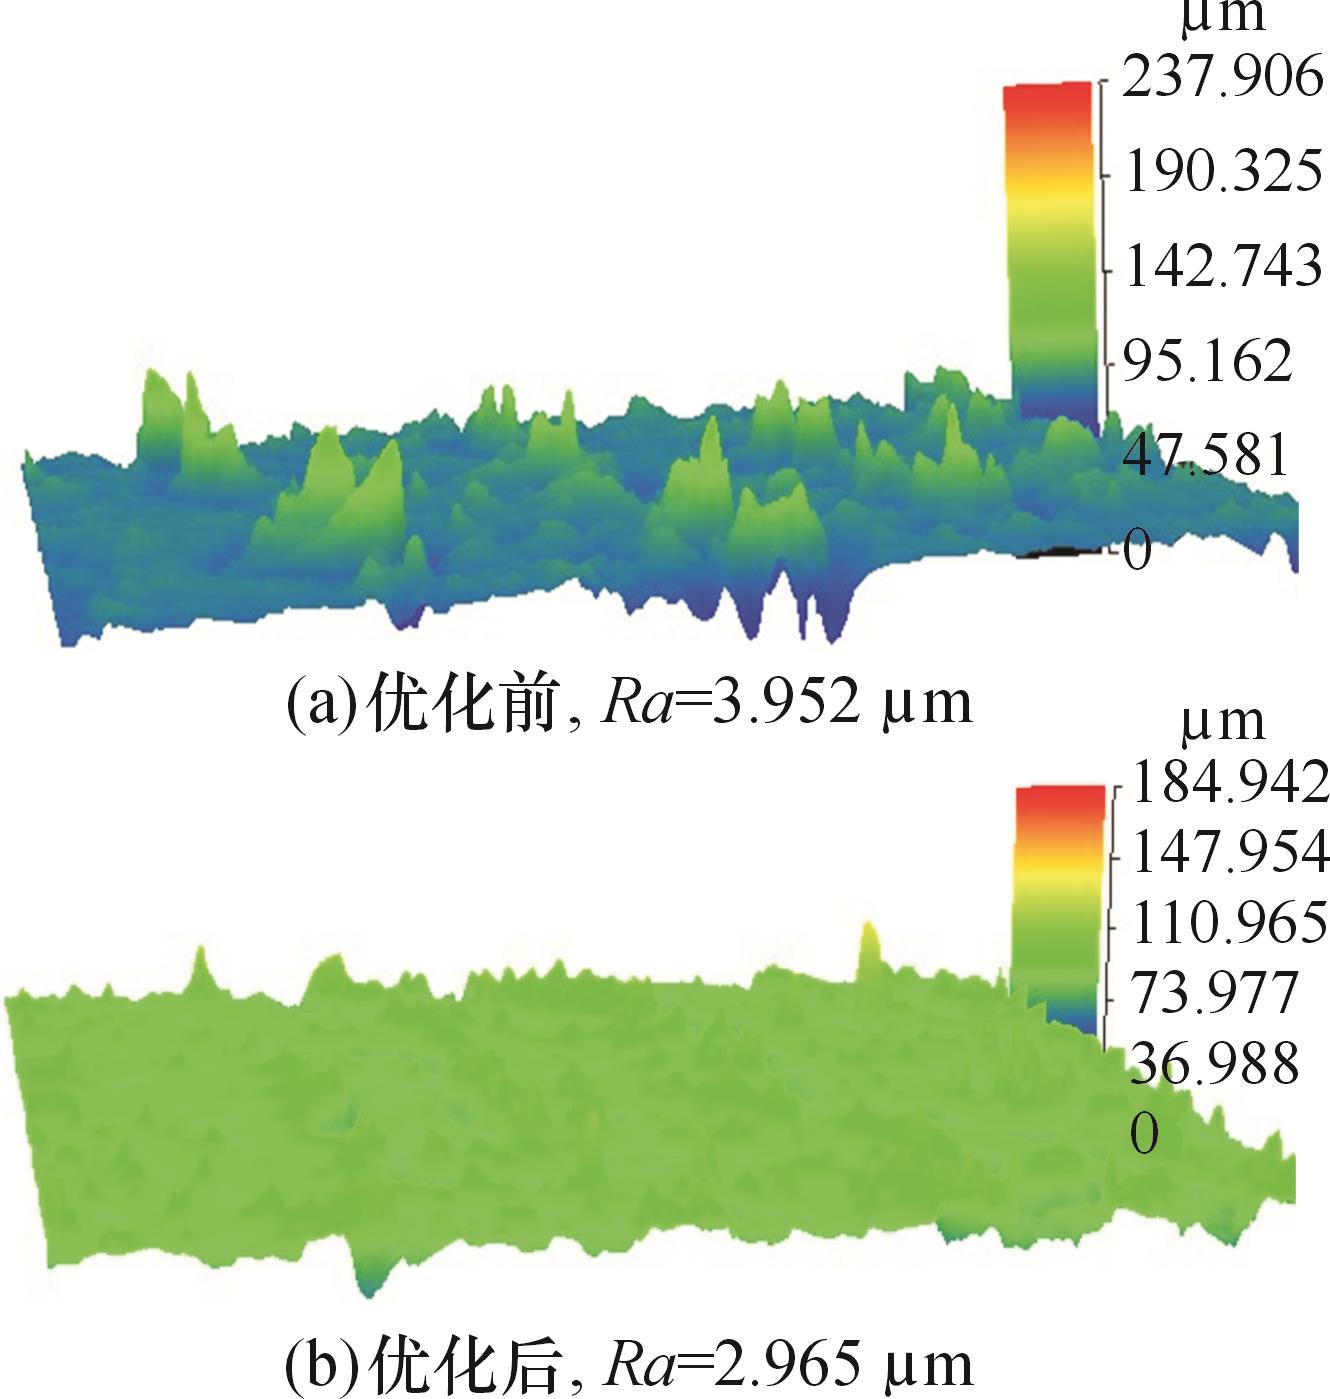
图11 优化前后粗糙度对比
Fig.11 Roughness comparison
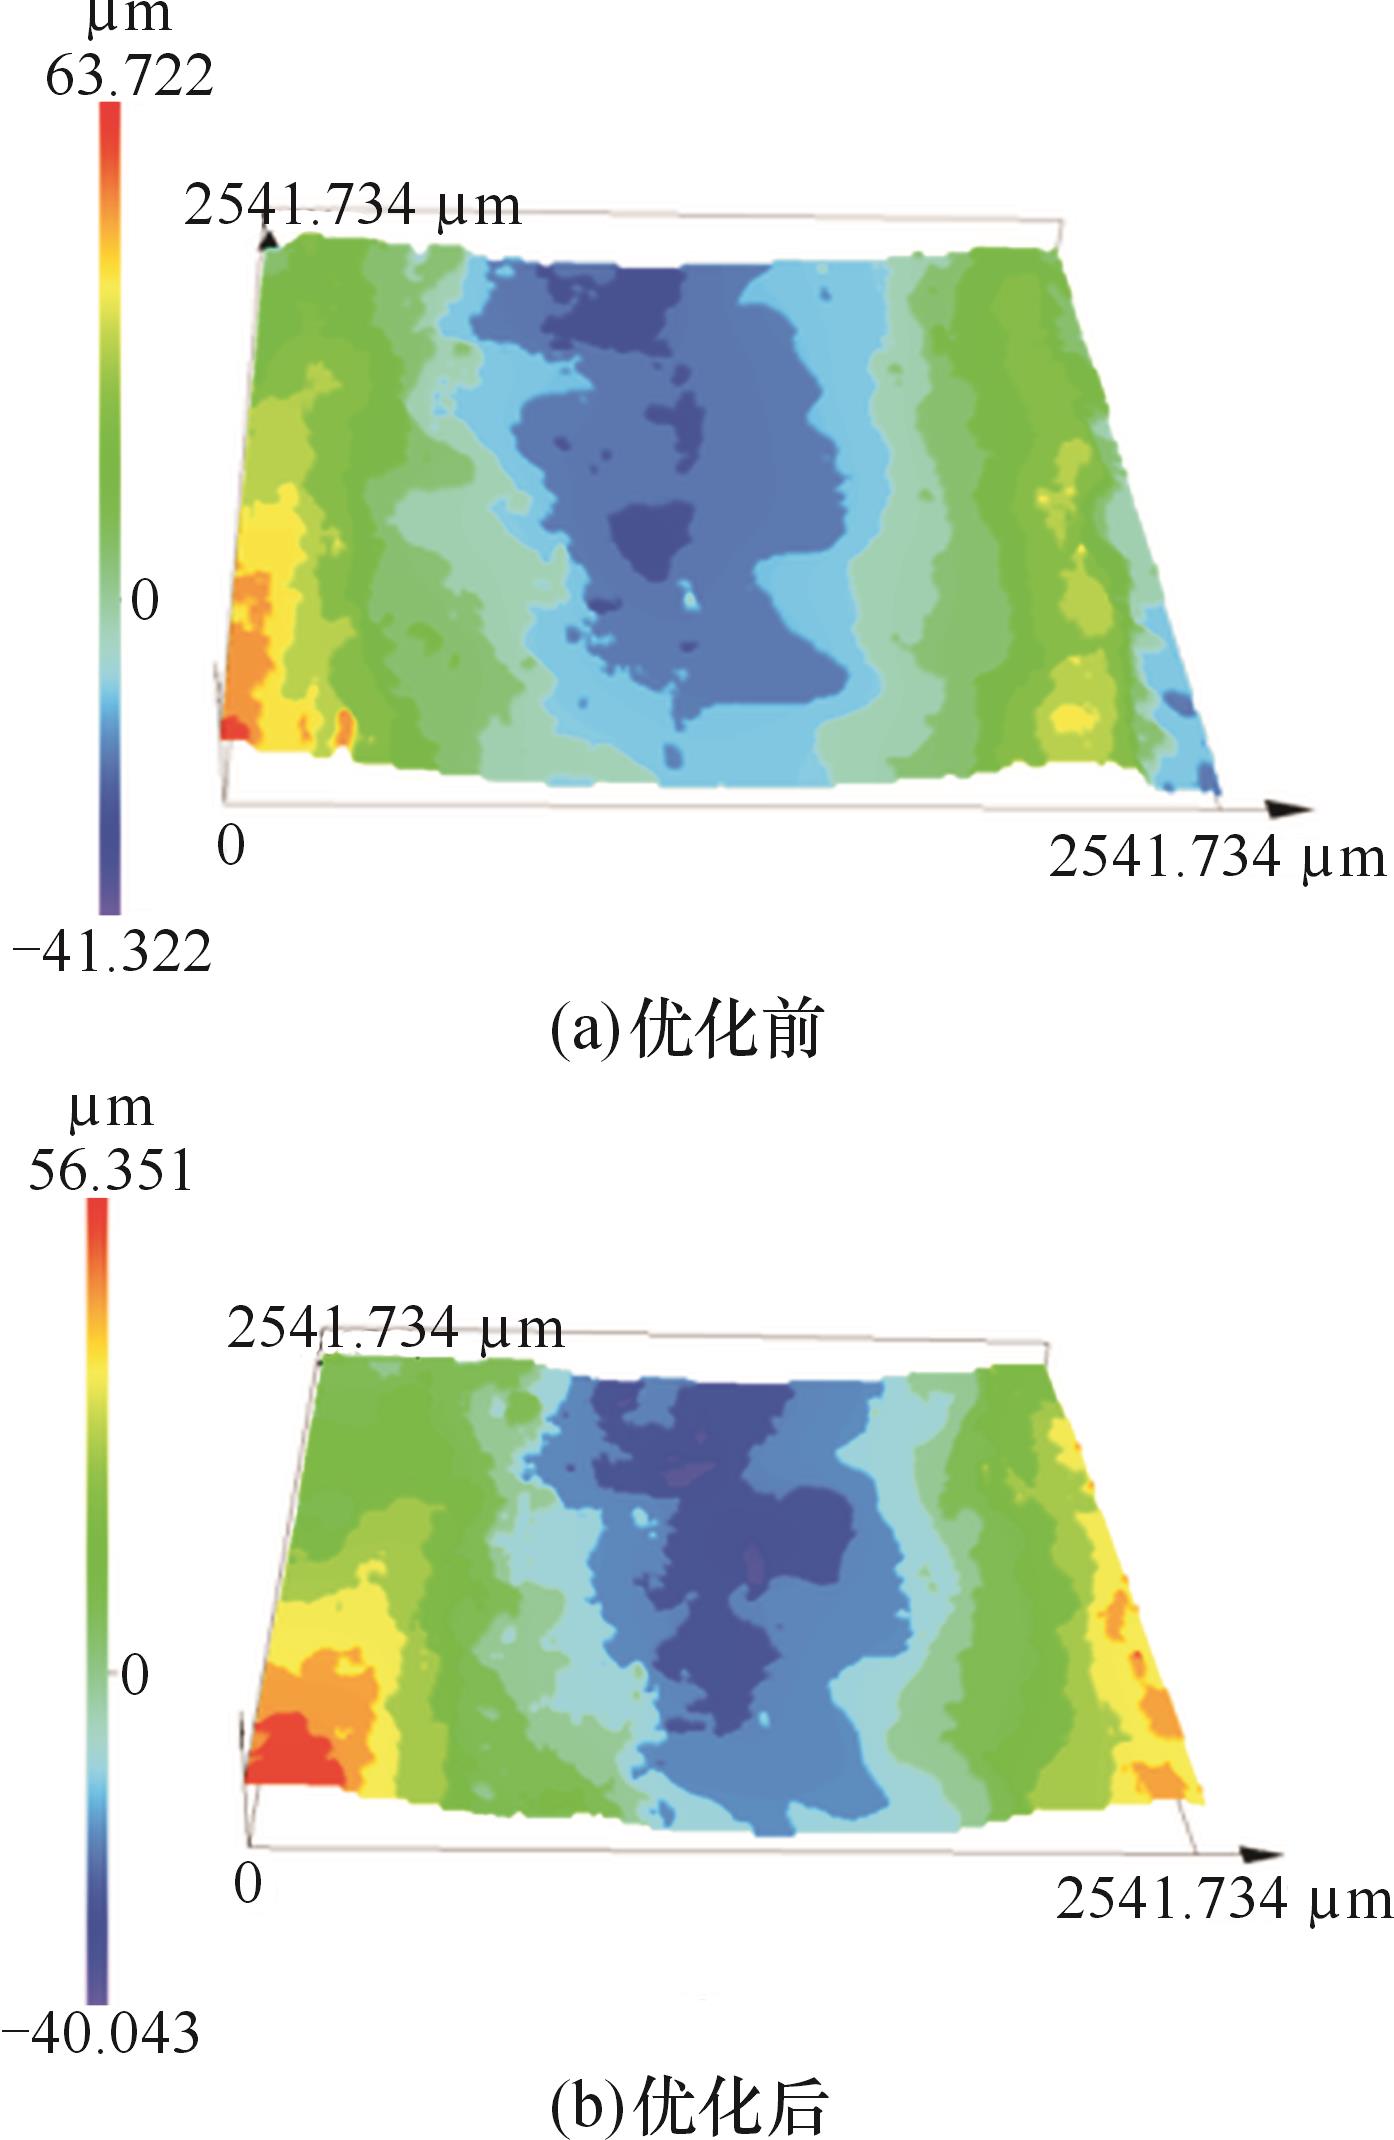
图12 磨痕三维形貌
Fig.12 Friction depth 3-dimensional map
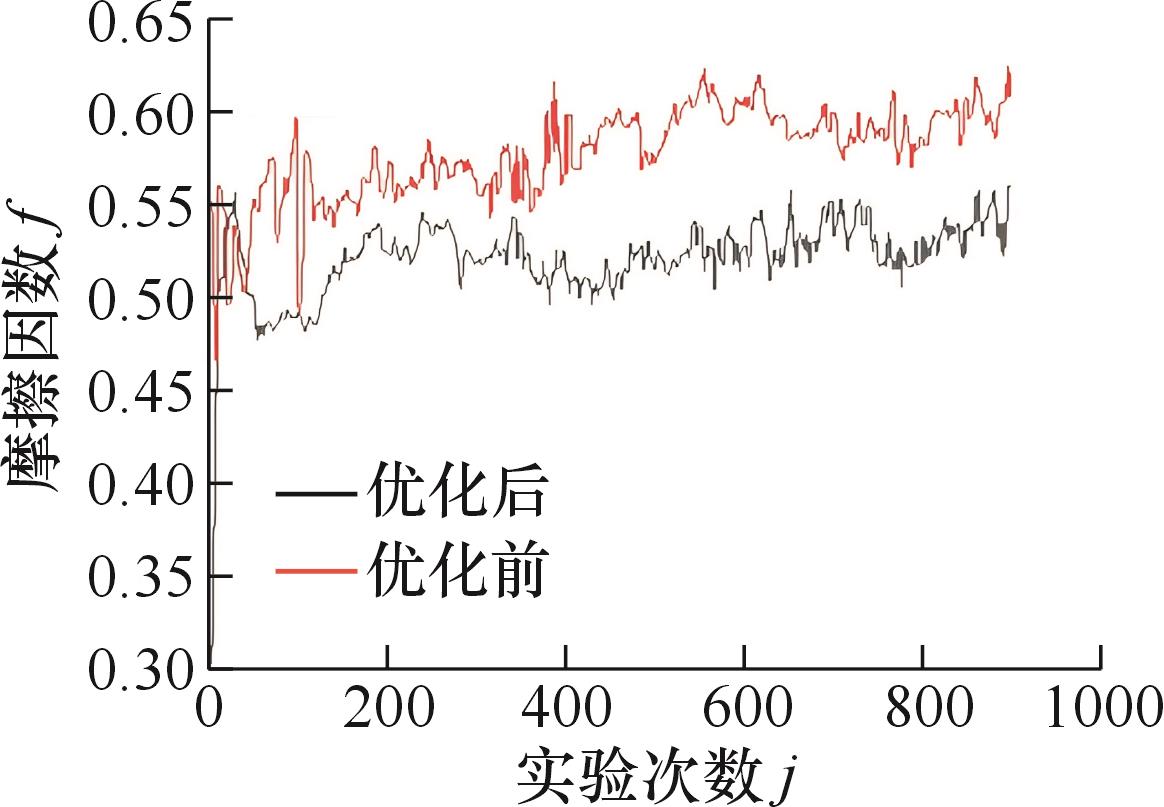
图13 摩擦因数对比
Fig.13 Friction coefficient comparison
| [1] | XU X, BIAN H, LIU W, et al. Microstructure and Properties of the Tribaloy T-800 Coating Fabricated by Laser Cladding on the DZ125 Superalloy[J]. Journal of Thermal Spray Technology, 2023, 32(7): 2112-2122. |
| [2] | COZZOLINO E, LOPRESTO V, BORRELLI D, et al. An Integrated Approach to Investigate the Energy Consumption for Manufacturing and Surface Finishing 3D Printed Inconel 718 Parts[J]. Journal of Manufacturing Processes, 2022, 79: 193-205. |
| [3] | LIU W, WEI H, LIU A, et al. Multi-index Co-evaluation of Metal Laser Direct Deposition: an Investigation of Energy Input Effect on Energy Efficiency and Mechanical Properties of 316l Parts[J]. Journal of Manufacturing Processes, 2022, 76: 277-290. |
| [4] | GE W, LI H, WEN X, et al. Mathematical Modelling of Carbon Emissions and Process Parameters Optimisation for Laser Welding Cell[J]. International Journal of Production Research, 2023, 61(15): 5009-5028. |
| [5] | WU J, ZHANG C, LIAN K, et al. Carbon Emission Modeling and Mechanical Properties of Laser, Arc and Laser-arc Hybrid Welded Aluminum Alloy Joints[J]. Journal of Cleaner Production, 2022, 378: 134437. |
| [6] | INGARAO G, PRIARONE P C. A Comparative Assessment of Energy Demand and Life Cycle Costs for Additive- and Subtractive-based Manufacturing Approaches[J]. Journal of Manufacturing Processes, 2020, 56: 1219-1229. |
| [7] | PANDEY S, SRIVASTAVA R, NARAIN R, et al. Optimization of Process Parameters for Direct Energy Deposition of 15Cr5Ni Precipitation Hardened Stainless Steel for Aircraft Parts Repair and Maintenance[J]. Proceedings of the Institution of Mechanical Engineers, Part C: Journal of Mechanical Engineering Science, 2022, 236(24): 11505-11520. |
| [8] | ZHENG J, CHEN A, YAO J, et al. Combination Method of Multiple Molding Technologies for Reducing Energy and Carbon Emission in the Foundry Industry[J]. Sustainable Materials and Technologies, 2022, 34: e00522. |
| [9] | PAWANR S, GARG G K, ROUTROY S. Development of an Empirical Model to Quantify Carbon Emissions for Machining of Cylindrical Parts[J]. Environmental Science and Pollution Research, 2023, 30(8): 21565-21587. |
| [10] | NI H, YAN C, GE W, et al. Integrated Optimization of Cutting Parameters and Hob Parameters for Energy-conscious Gear Hobbing[J]. The International Journal of Advanced Manufacturing Technology, 2022, 118(5): 1609-1626. |
| [11] | JIANG X, TIAN Z, LIU W, et al. An Energy-efficient Method of Laser Remanufacturing Process[J]. Sustainable Energy Technologies and Assessments, 2022, 52: 102201. |
| [12] | WANG W, TIAN G, ZHANG H, et al. A Hybrid Genetic Algorithm with Multiple Decoding Methods for Energy-aware Remanufacturing System Scheduling Problem[J]. Robotics and Computer-Integrated Manufacturing, 2023, 81: 102509. |
| [13] | CHEN K, JIANG X, LIU W, et al. A Novel Multi-objective Optimization of High-power Laser Directed Energy Deposition Green Processes: a Case Study of Titanium Alloy[J]. Journal of Cleaner Production, 2025, 494: 144877. |
| [14] | 段诚茂, 曹华军, 李洪丞, 等. 基于碳效率的铝合金激光焊接工艺系统低碳优化方法[J]. 计算机集成制造系统, 2021, 27(5): 1309-1318. |
| DUAN Chengmao, CAO Huajun, LI Hongcheng, et al. Low-carbon Optimization Method of Aluminum Alloy Laser Welding Process System Based on Carbon Efficiency[J]. Computer Integrated Manufacturing Systems, 2021, 27(5): 1309-1318. | |
| [15] | 吴剑钊, 孙家豪, 张超勇, 等. 光纤激光焊接的碳排放建模与多响应评价[J]. 机械工程学报, 2023, 59(7): 186-199. |
| WU Jianzhao, SUN Jiahao, ZHANG Chaoyong, et al. Carbon Emission Modeling and Multi-response Evaluation of Fiber Laser Welding[J]. Journal of Mechanical Engineering, 2023, 59(7): 186-199. | |
| [16] | WU P, HE Y, LI Y, et al. Multi-objective Optimisation of Machining Process Parameters Using Deep Learning-based Data-driven Genetic Algorithm and TOPSIS[J]. Journal of Manufacturing Systems, 2022, 64: 40-52. |
| [1] | 李明磊, 贾育秦, 张学良, 刘丽琴, 杜娟, 温淑花, 兰国生. 基于多目标差异演化算法的并联机构结构优化 [J]. J4, 201016, 21(16): 1915-1920. |
| [2] | 武星, 吕鹏, 沙金龙, 李杨志, 孟昭旭. 基于改进多目标粒子群优化的移动机器人对接轨迹规划[J]. 中国机械工程, 2026, 37(8): 1999-2008. |
| [3] | 王聪, 魏立新, 孙浩, 呼子宇, 崔慧慧. 考虑运输资源限制的动态柔性车间调度问题及自适应竞争重构算法[J]. 中国机械工程, 2026, 37(7): 1708-1716. |
| [4] | 刘设, 李佳欣, 田志强, 张诗曼. 考虑客户满意度的模糊柔性作业车间调度优化方法[J]. 中国机械工程, 2026, 37(7): 1734-1745. |
| [5] | 刘金锋, 顾世民, 张占虎, 李苏, 陈宇, 王学敏, 钱天龙. 基于多目标约束的狭小空间便携式机器人轨迹优化方法[J]. 中国机械工程, 2026, 37(6): 1508-1517. |
| [6] | 付昊成, 吴少伟, 姜潮. 基于蒙特卡罗减方差方法的图像传感器辐射屏蔽结构多目标优化设计[J]. 中国机械工程, 2026, 37(5): 1045-1053. |
| [7] | 王冰旭, 高彤, 万敏, 焦龙飞, 蔚飞, 张卫红. 结合部对精密机床动态特性影响的分析[J]. 中国机械工程, 2026, 37(5): 1111-1121. |
| [8] | 曹卫东, 汪袁烁, 李闽榕, 陈富祺, 陈行政, 吴电建, 胡可心. 滚齿刀具和控制参数超启发优化与决策[J]. 中国机械工程, 2026, 37(4): 846-854. |
| [9] | 王志会, 彭涛, 刘伟鹏, 唐任仲. 基于数据分配的铝铸件生产过程细粒度碳排放核算方法[J]. 中国机械工程, 2026, 37(4): 920-928. |
| [10] | 张雷, 张振, 刘润泽. 制造特征智能解析驱动的零件低碳工艺优化方法[J]. 中国机械工程, 2026, 37(4): 929-938. |
| [11] | 孔琳, 曾庆良, 王黎明, 李方义, 张鑫, 逯振国, 王桂杰. 制造场景驱动的机械加工过程碳排放预测与不确定性分析方法[J]. 中国机械工程, 2026, 37(4): 948-958. |
| [12] | 杨洁, 江志刚, 朱硕, 陈鑫, 张华. 多寿命特征下再制造机电产品全工作域可靠性设计研究进展[J]. 中国机械工程, 2026, 37(4): 987-998. |
| [13] | 曾丹, 杨武, 杜彦斌, 吕岩, 李聪波. 基于双注意力网络深度强化学习的柔性作业车间节能调度方法[J]. 中国机械工程, 2026, 37(10): 2511-2519. |
| [14] | 杜虹汗, 谭建军, 孙义忠, 宋朝省, 李浩, 关远. 多工况下风电齿轮箱行星轮滑动轴承耦合系统啮合与润滑分层优化[J]. 中国机械工程, 2026, 37(10): 2566-2576. |
| [15] | 赵丁选, 郭瑞, 王硕, 闫长长, 王子鹤, 张天赐. 复杂地形环境下无人步履式挖掘机的车身姿态规划方法[J]. 中国机械工程, 2026, 37(1): 233-242. |
| 阅读次数 | ||||||
|
全文 |
|
|||||
|
摘要 |
|
|||||
