ISSN 1004-132X
CN 42-1294/TH
CN 42-1294/TH
中国机械工程 ›› 2026, Vol. 37 ›› Issue (10): 2603-2609.DOI: 10.3969/j.issn.1004-132X.2026.10.023
王晓沁2( ), 殷增斌2(), 唐海权1, 洪东波2, 袁军堂2
收稿日期:2025-09-02
出版日期:2026-10-25
发布日期:2026-11-10
通讯作者:
殷增斌
作者简介:王晓沁,女,1972年生,副教授。研究方向为数字化设计与制造、高效加工技术。E-mail:wxq971011@aliyun.com基金资助:
WANG Xiaoqin2(), YIN Zengbin2(), TANG Haiquan1, HONG Dongbo2, YUAN Juntang2
Received:2025-09-02
Online:2026-10-25
Published:2026-11-10
Contact:
YIN Zengbin
摘要:
利用微波烧结技术制备了可转位带槽形α/β-SiAlON陶瓷刀具,系统研究了微波烧结的复杂刃形SiAlON陶瓷刀具高速干切削镍基高温合金GH4169的切削性能、失效机理和加工表面完整性。研究结果表明:微波烧结的复杂刃形α/β-SiAlON陶瓷刀具寿命随铣削速度先增长后缩短,铣削深度对刀具寿命影响不明显,可转位复杂刃形α/β-SiAlON陶瓷刀具更适合高速大切深的粗加工,最优切削参数为铣削速度800 m/min、铣削深度1.5 mm、每齿进给量0.12 mm;在不同切削参数下,黏结磨损是造成SiAlON陶瓷刀具失效的主要原因;加工表面粗糙度随着铣削速度的提高而增大;加工表面硬化程度随着铣削速度的提高(600~1000 m/min)由177%增大至221%,随铣削深度的变化较小,介于180%~190%;硬化深度随着铣削速度和铣削深度的增大变化均不明显,介于240~300 μm。
中图分类号:
王晓沁, 殷增斌, 唐海权, 洪东波, 袁军堂. α/β-SiAlON陶瓷刀具高速铣削GH4169性能与表面完整性[J]. 中国机械工程, 2026, 37(10): 2603-2609.
WANG Xiaoqin, YIN Zengbin, TANG Haiquan, HONG Dongbo, YUAN Juntang. Performance and Surface Integrity of High-speed Milling of GH4169 with α/β-SiAlON Ceramic Tools[J]. China Mechanical Engineering, 2026, 37(10): 2603-2609.
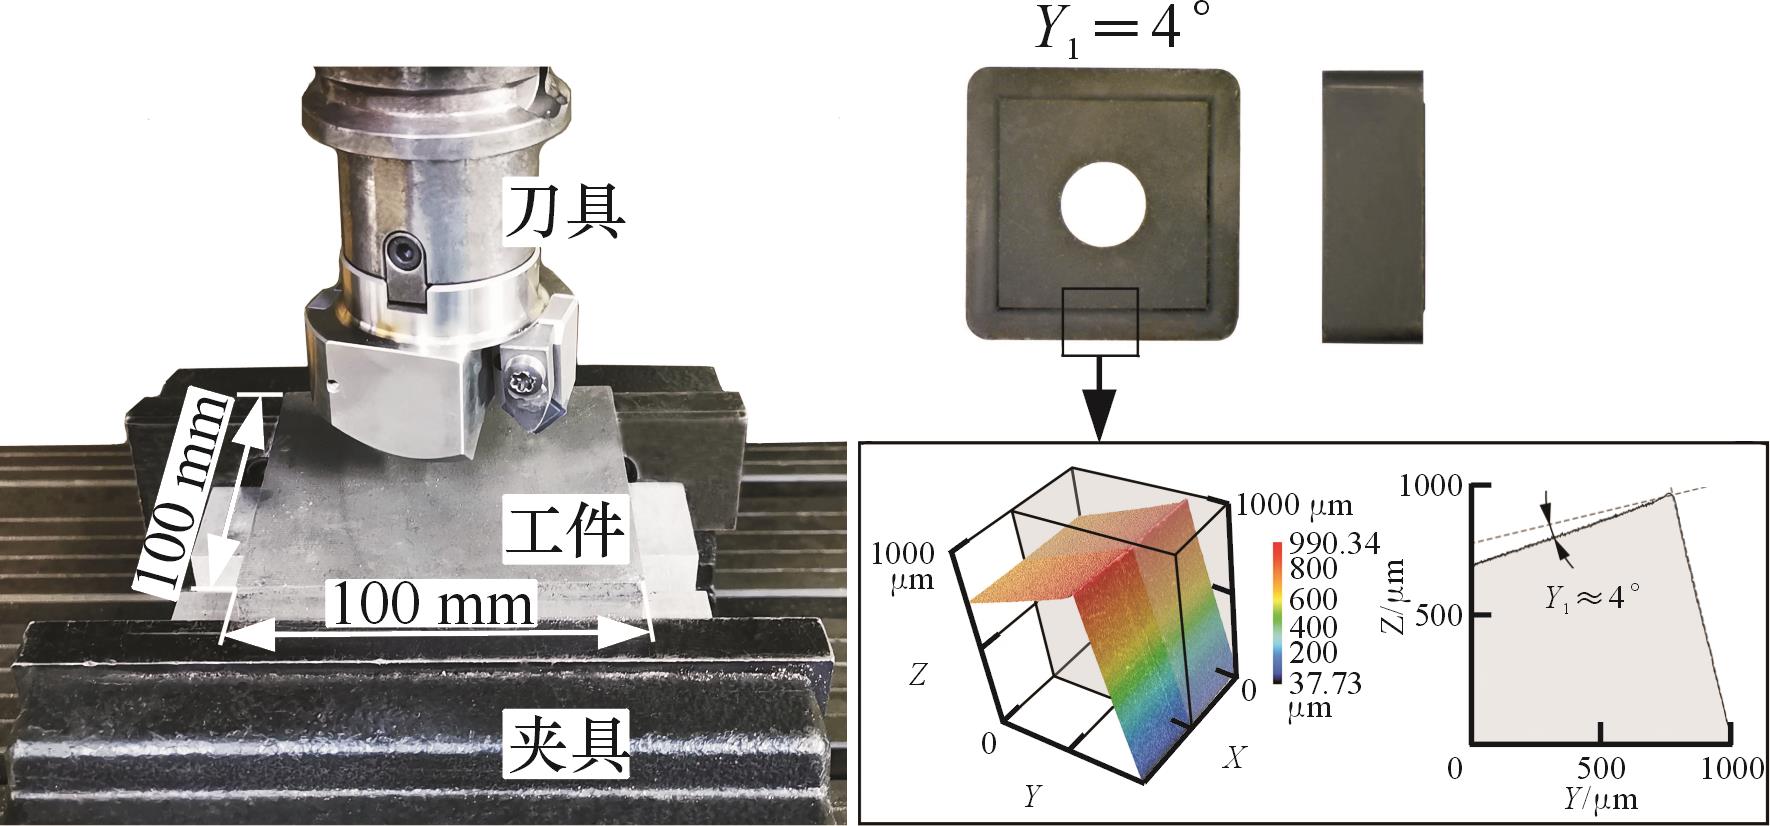
图1 切削试验图和SiAlON陶瓷刀具
Fig.1 Cutting test diagram and SiAlON ceramic cutting tools
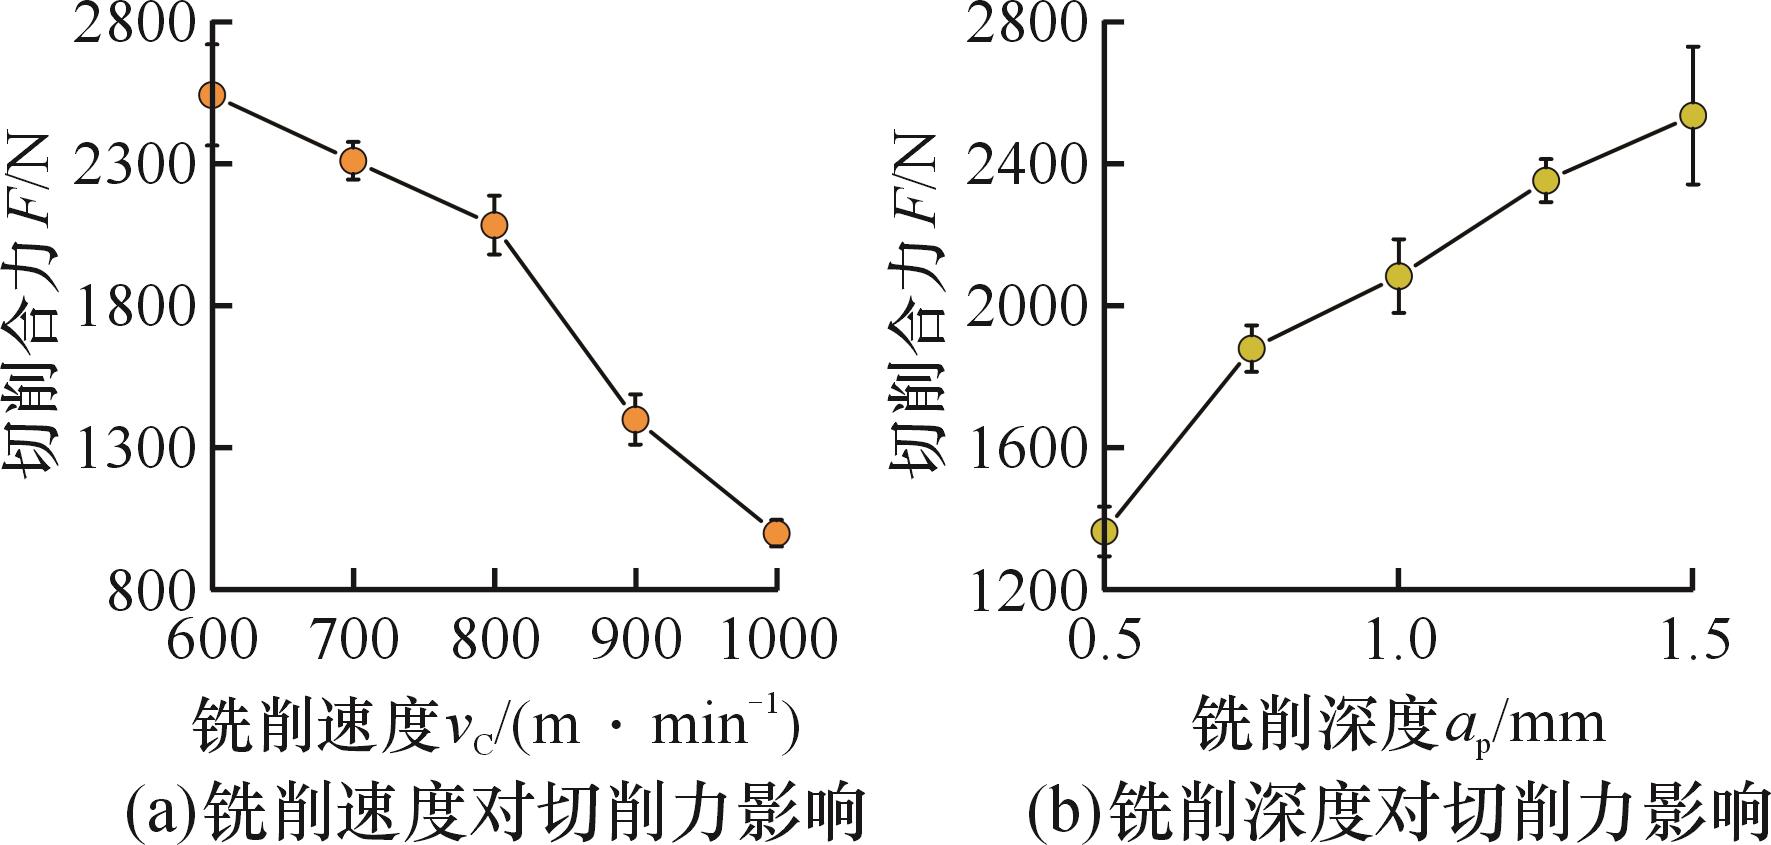
图2 切削参数对SiAlON陶瓷刀具面铣高温合金GH4169切削力的影响规律
Fig.2 The influence of cutting parameters on the cutting force of SiAlON ceramic cutting tools during face milling of the high-temperature alloy GH4169
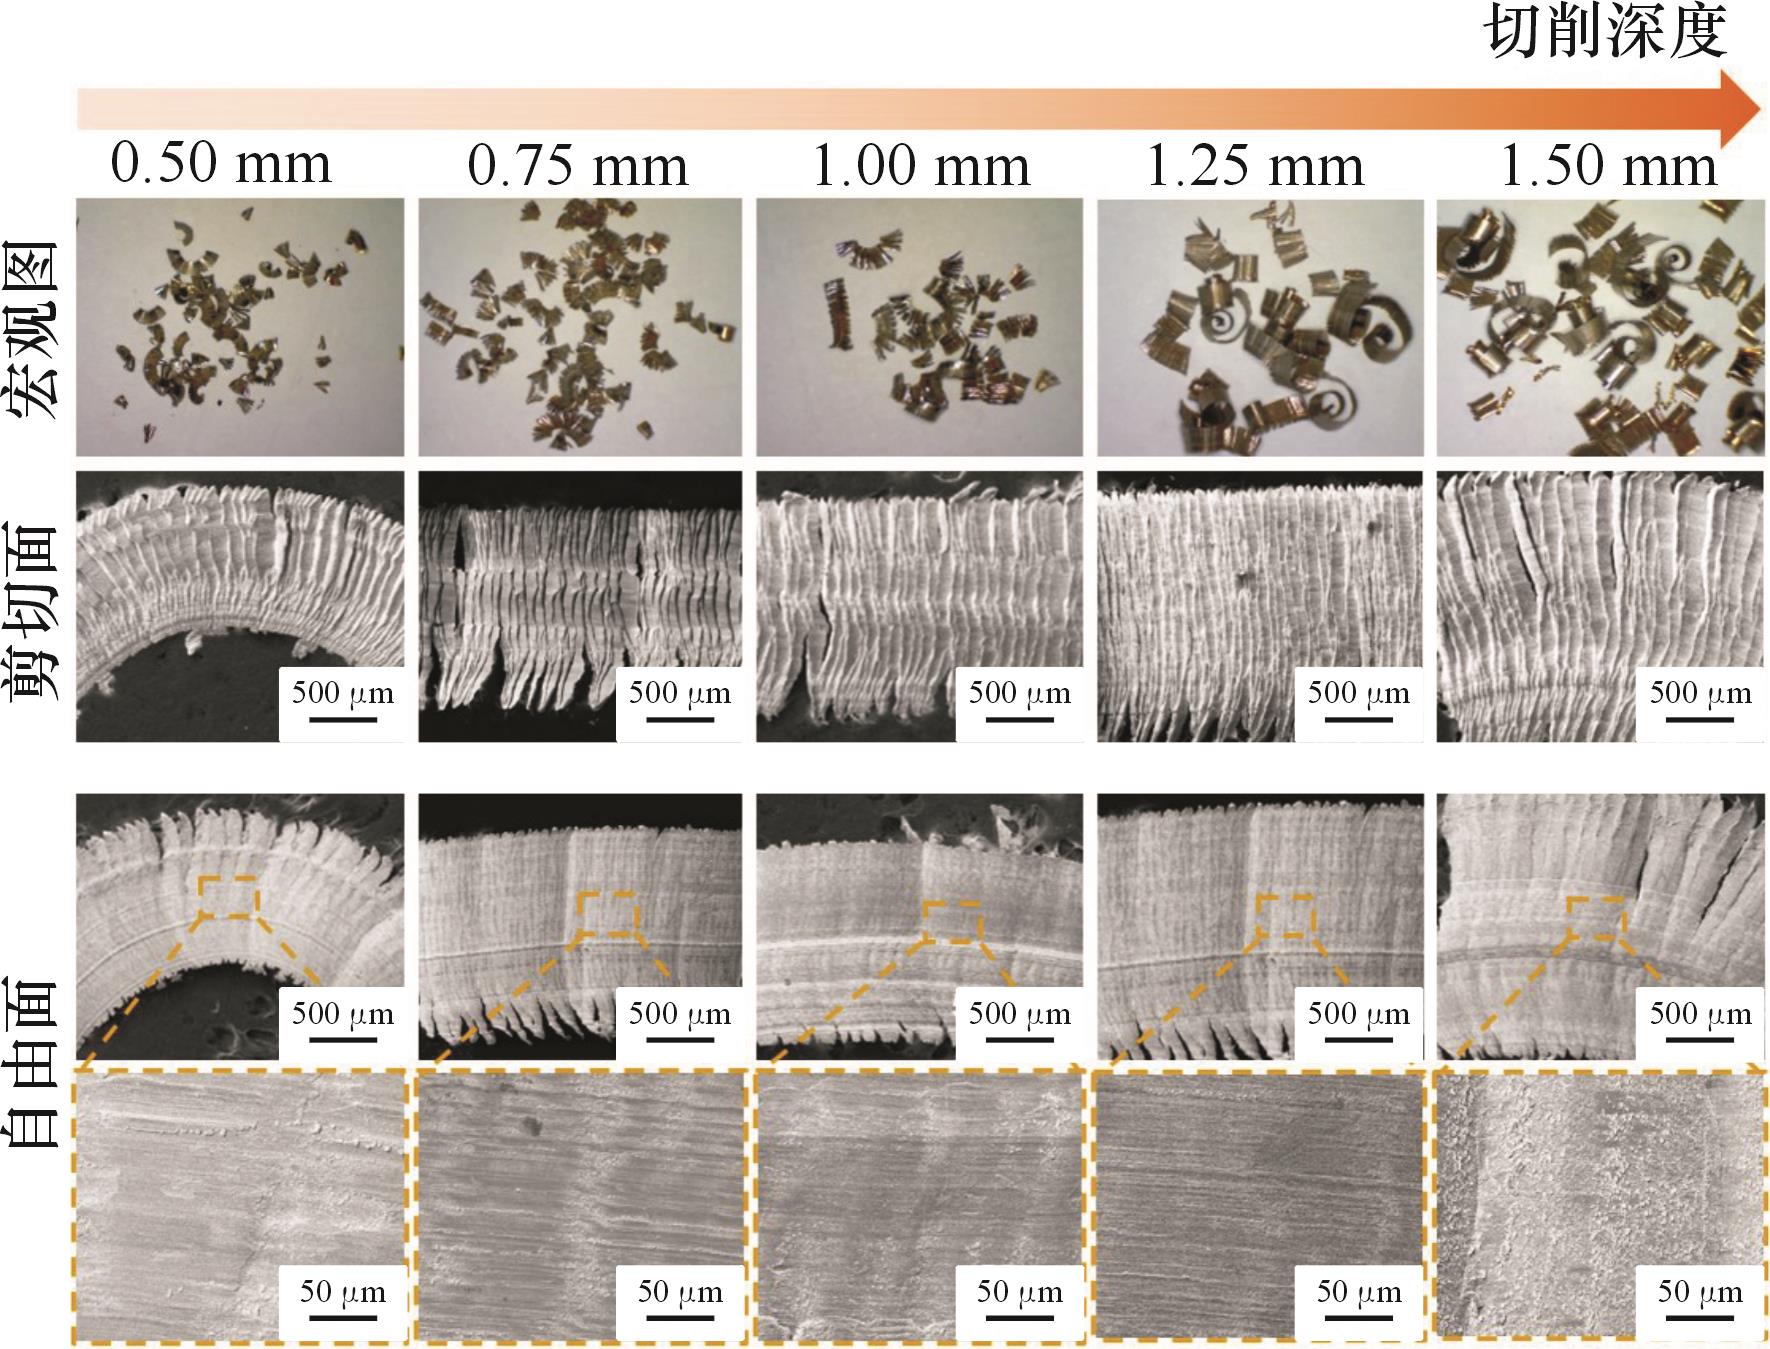
图3 不同铣削深度下切屑的宏观形貌以及剪切面和自由面的SEM微观形貌
Fig.3 The macroscopic morphology of the chips under different milling depth and SEM microscopic morphology of the shear surfaces and free surfaces
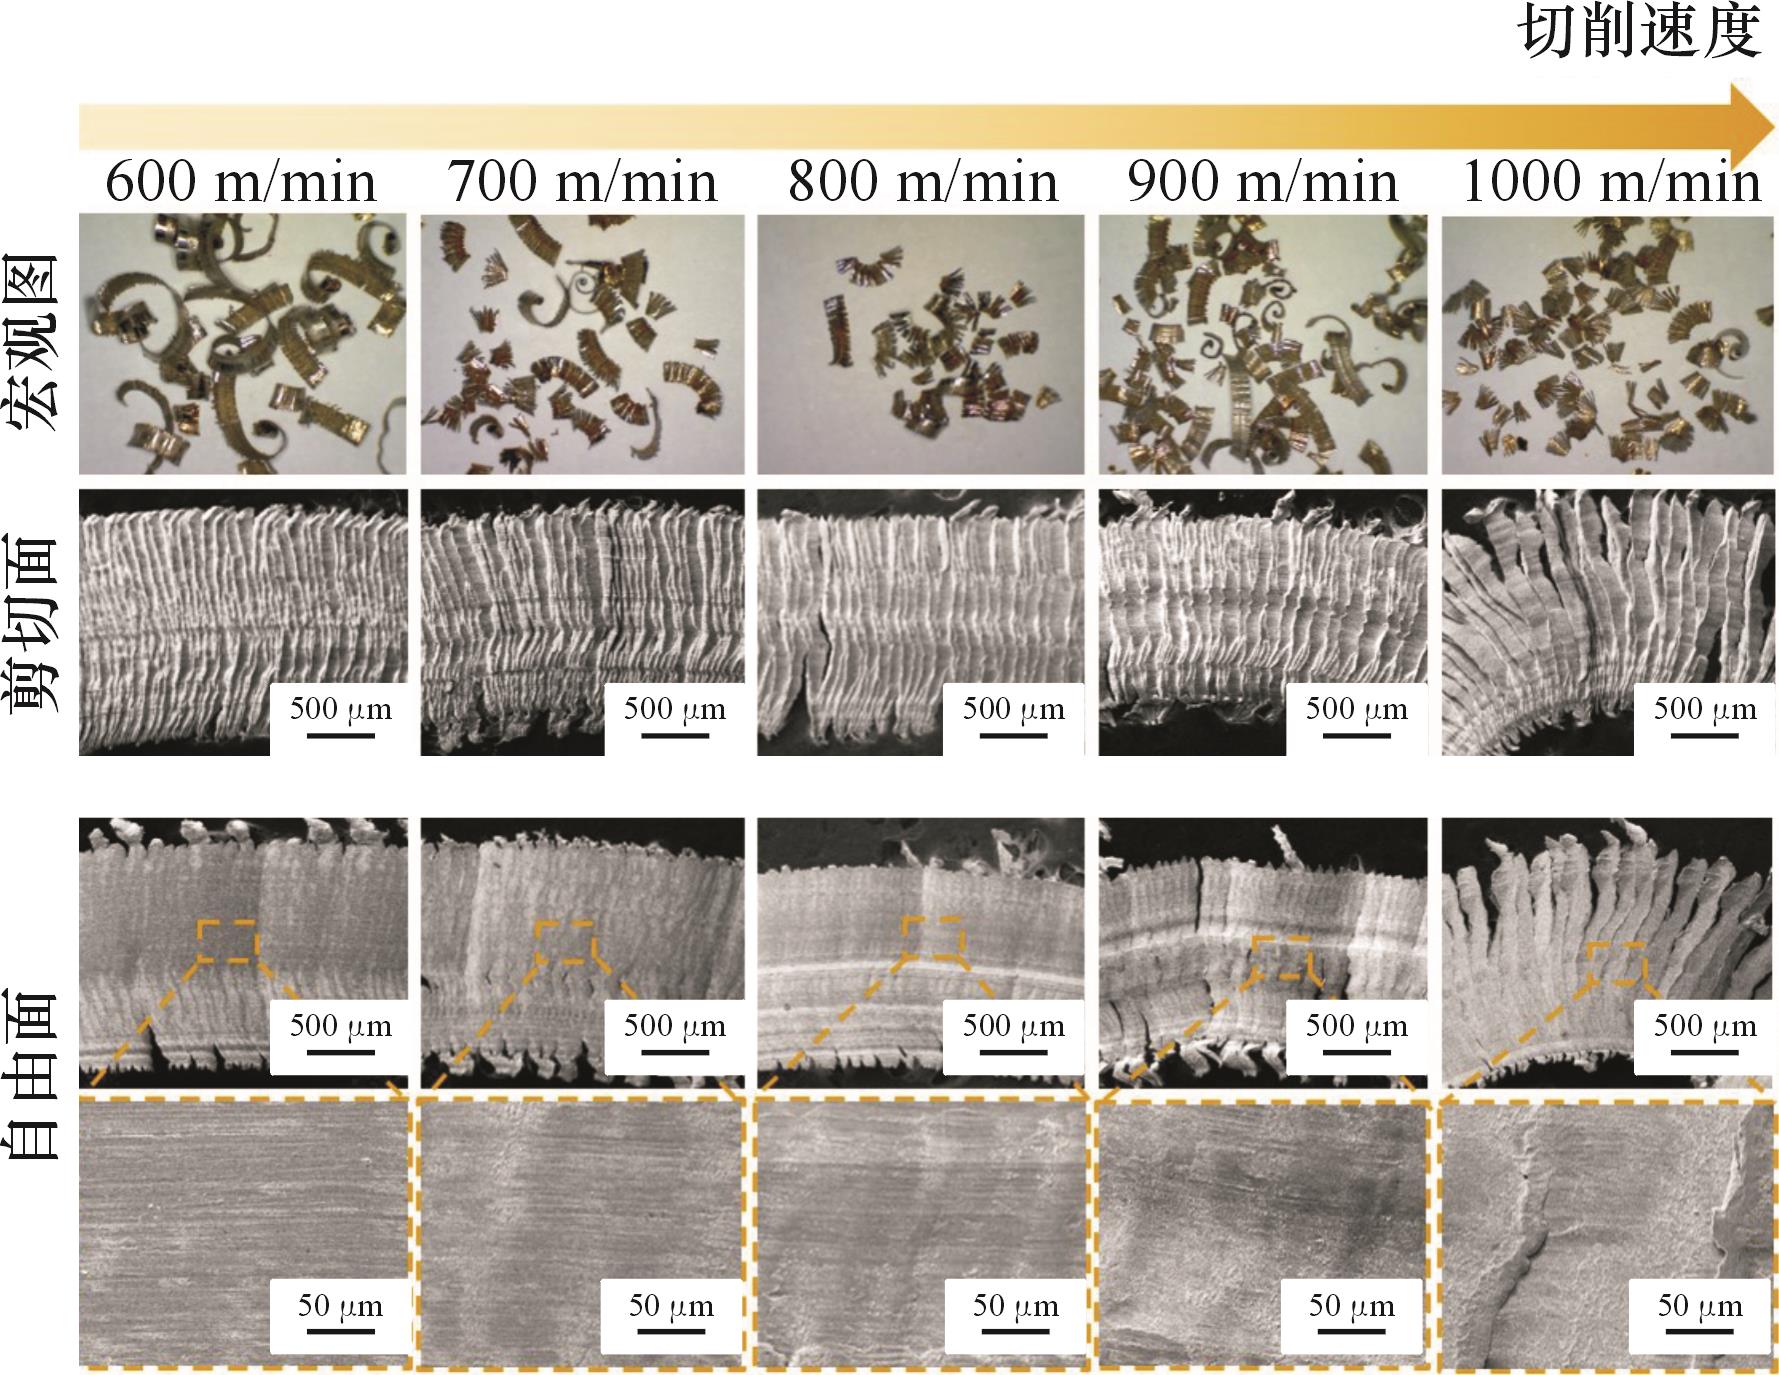
图4 不同铣削速度下切屑的宏观形貌以及剪切面和自由面的SEM微观形貌
Fig.4 The macroscopic morphology of the chips under different milling speed and SEM microscopic morphology of the shear surfaces and free surfaces
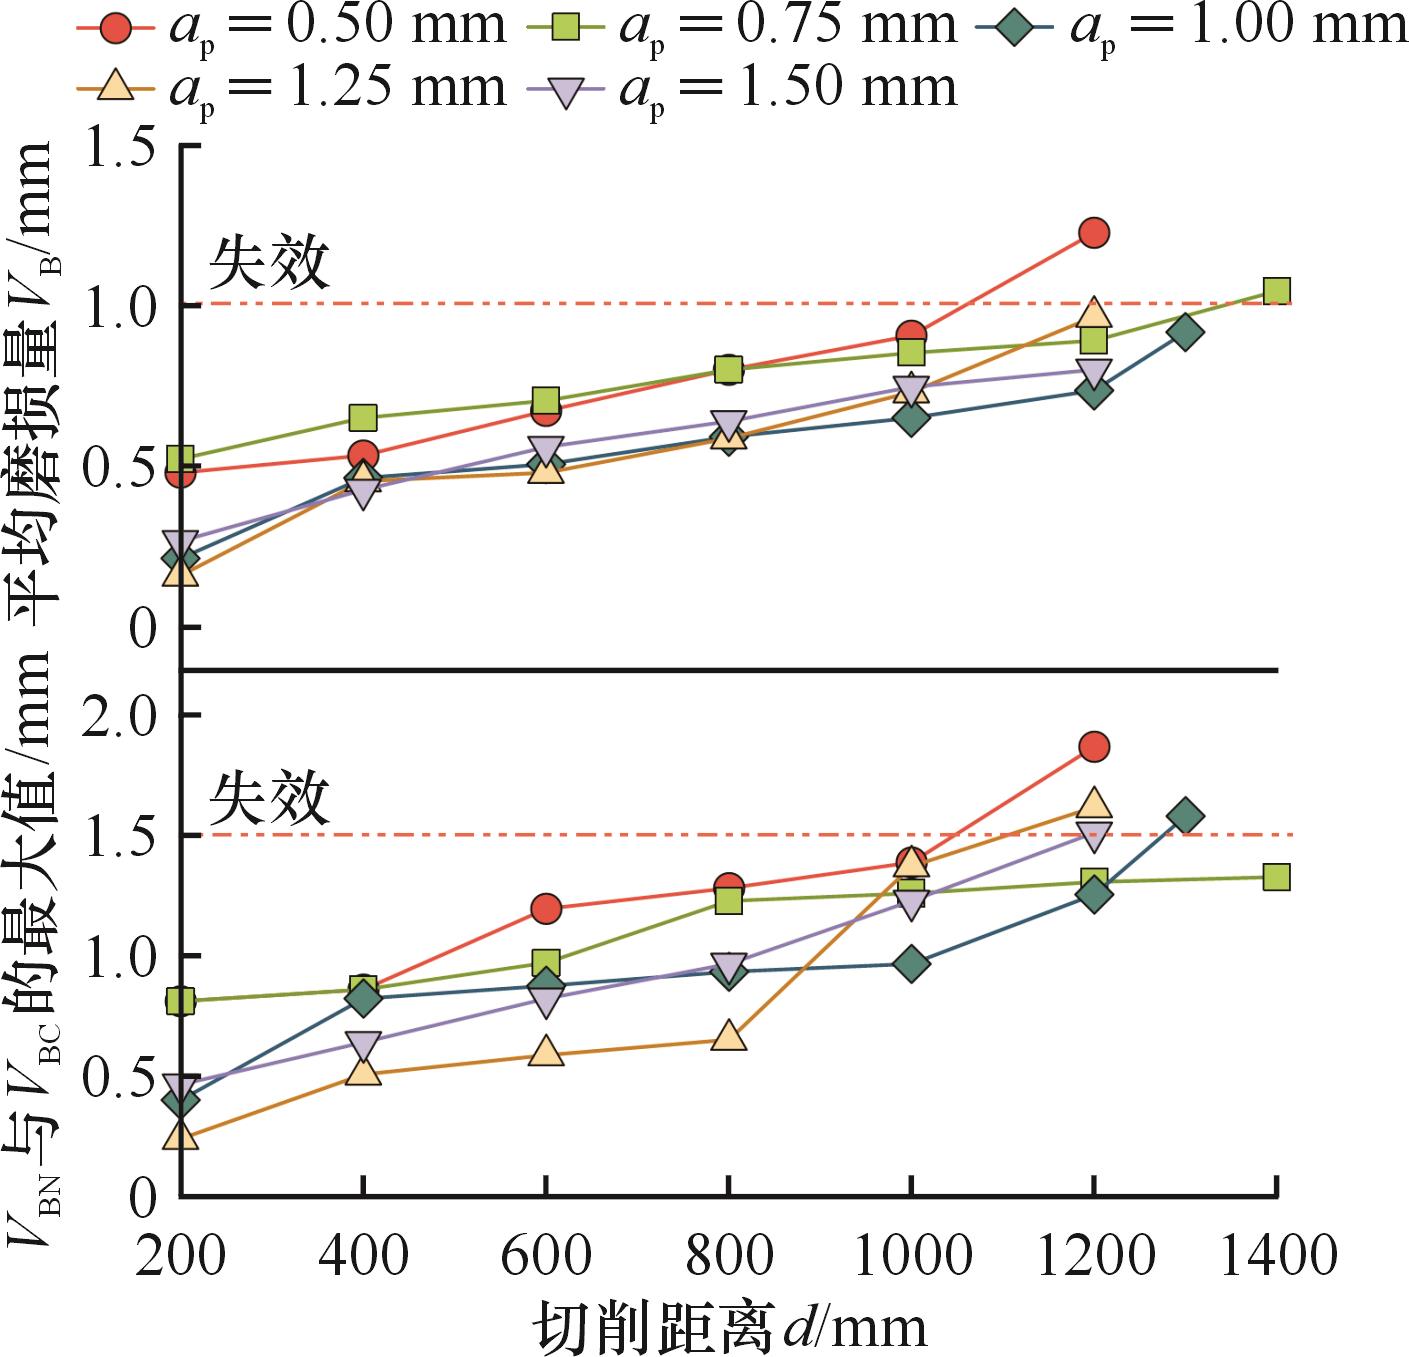
图5 不同铣削深度下复杂刃形α/β-SiAlON陶瓷刀片刀具寿命
Fig.5 Tool life of complex-edge α/β-SiAlON ceramic cutting tools under different milling depth
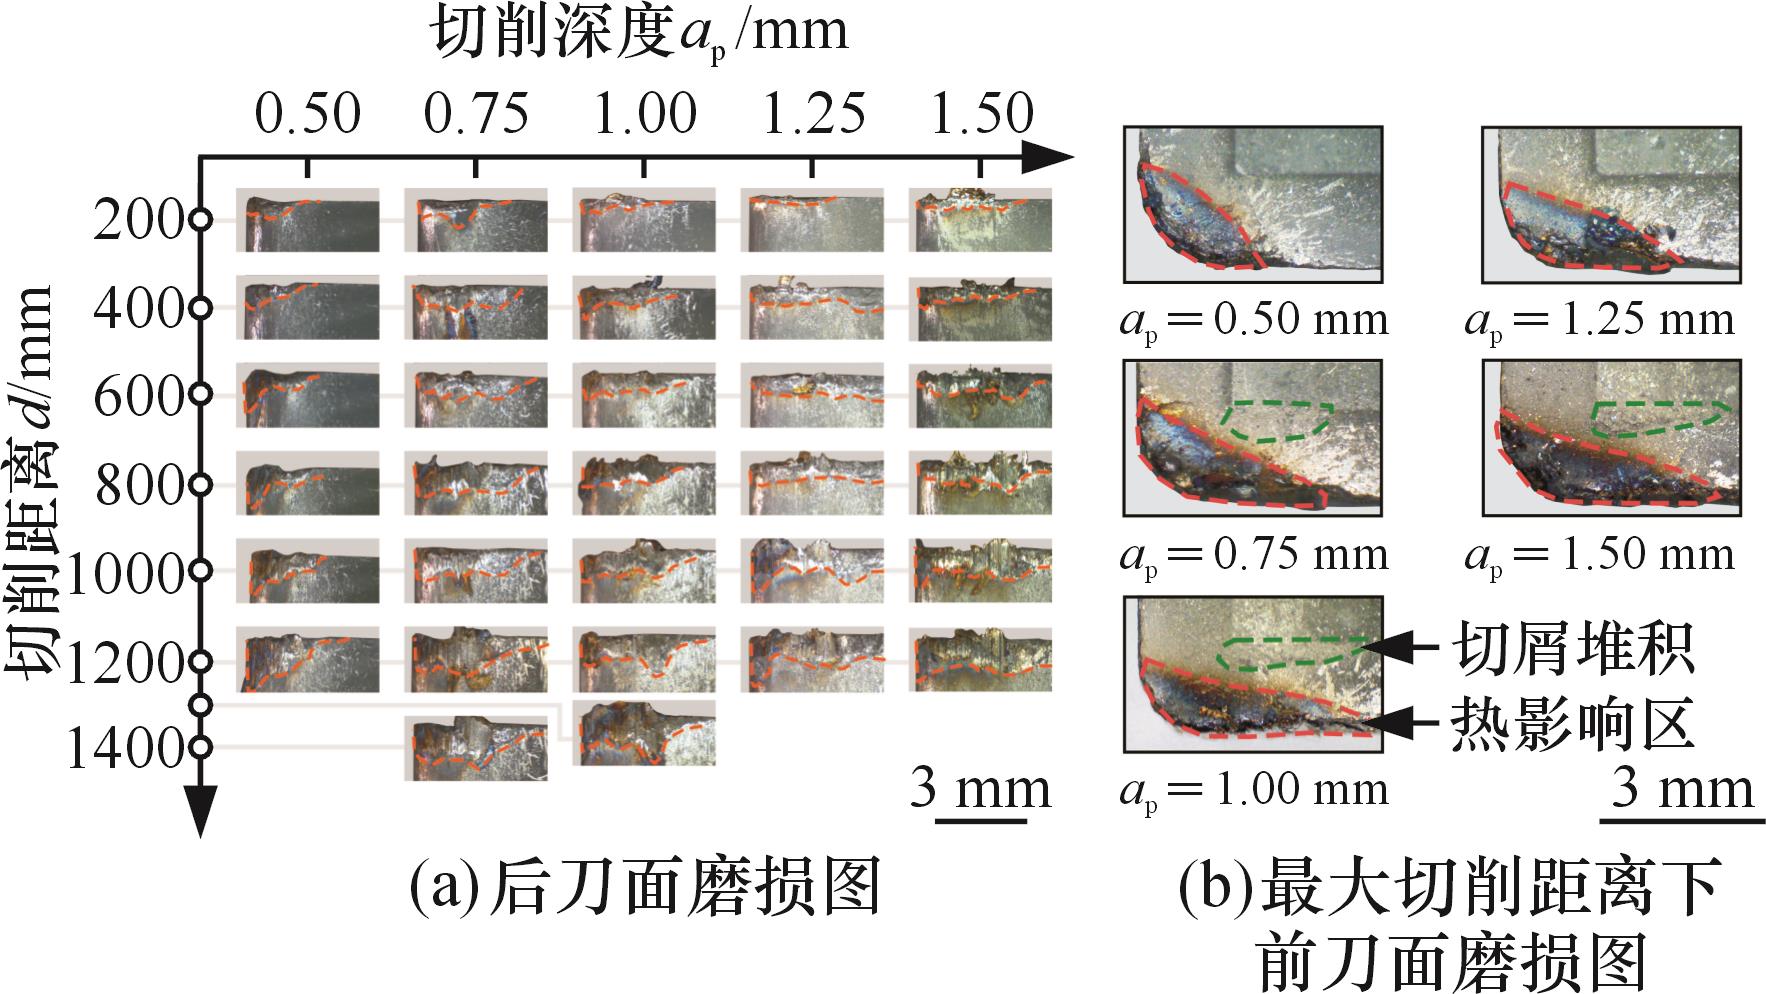
图6 不同铣削深度复杂刃形α/β-SiAlON陶瓷刀片磨损
Fig.6 Wear diagrams of complex-shaped α/β-SiAlON ceramic cutting tools after machining at different milling depths
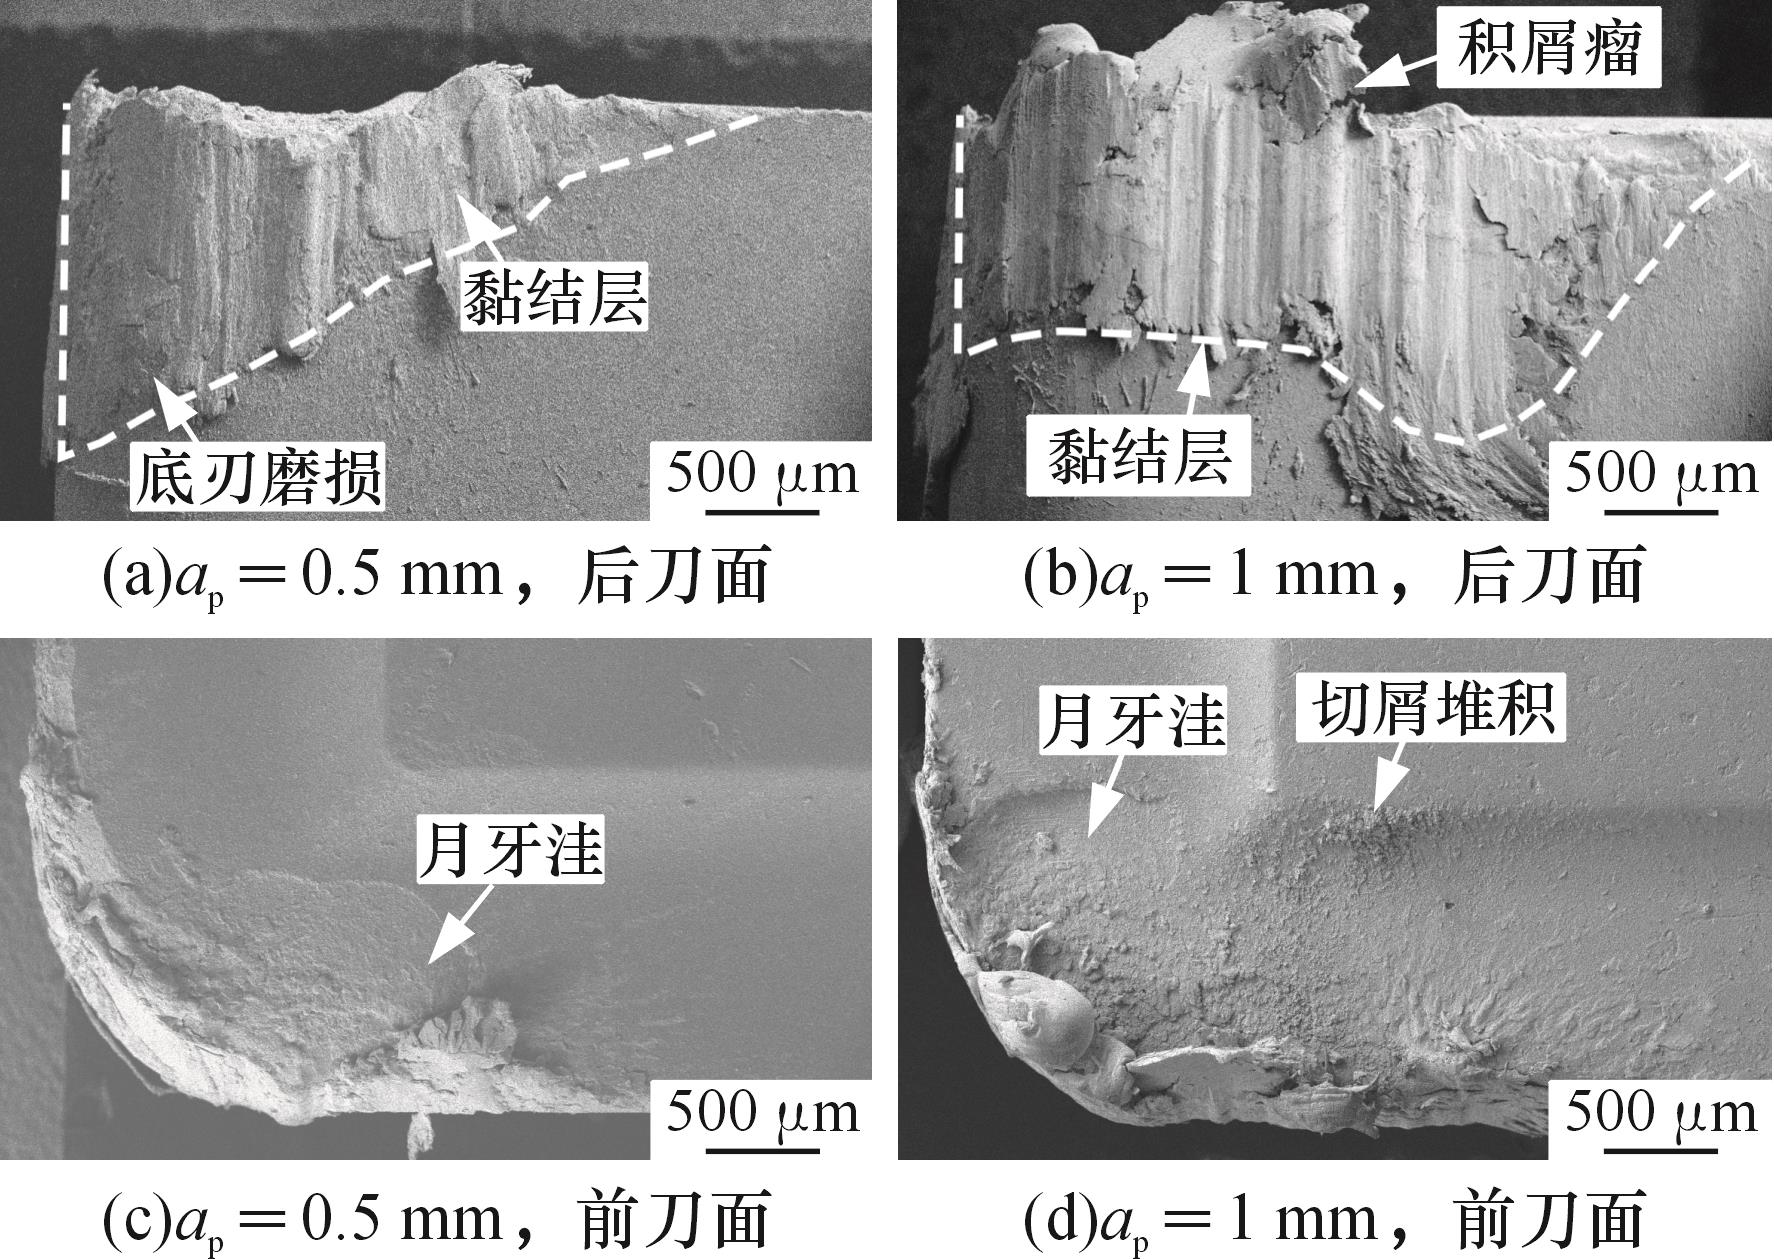
图7 不同铣削深度复杂刃形α/β-SiAlON陶瓷刀片SEM形貌
Fig.7 SEM morphologies of complex-profiled α/β-SiAlON ceramic inserts under different milling depths
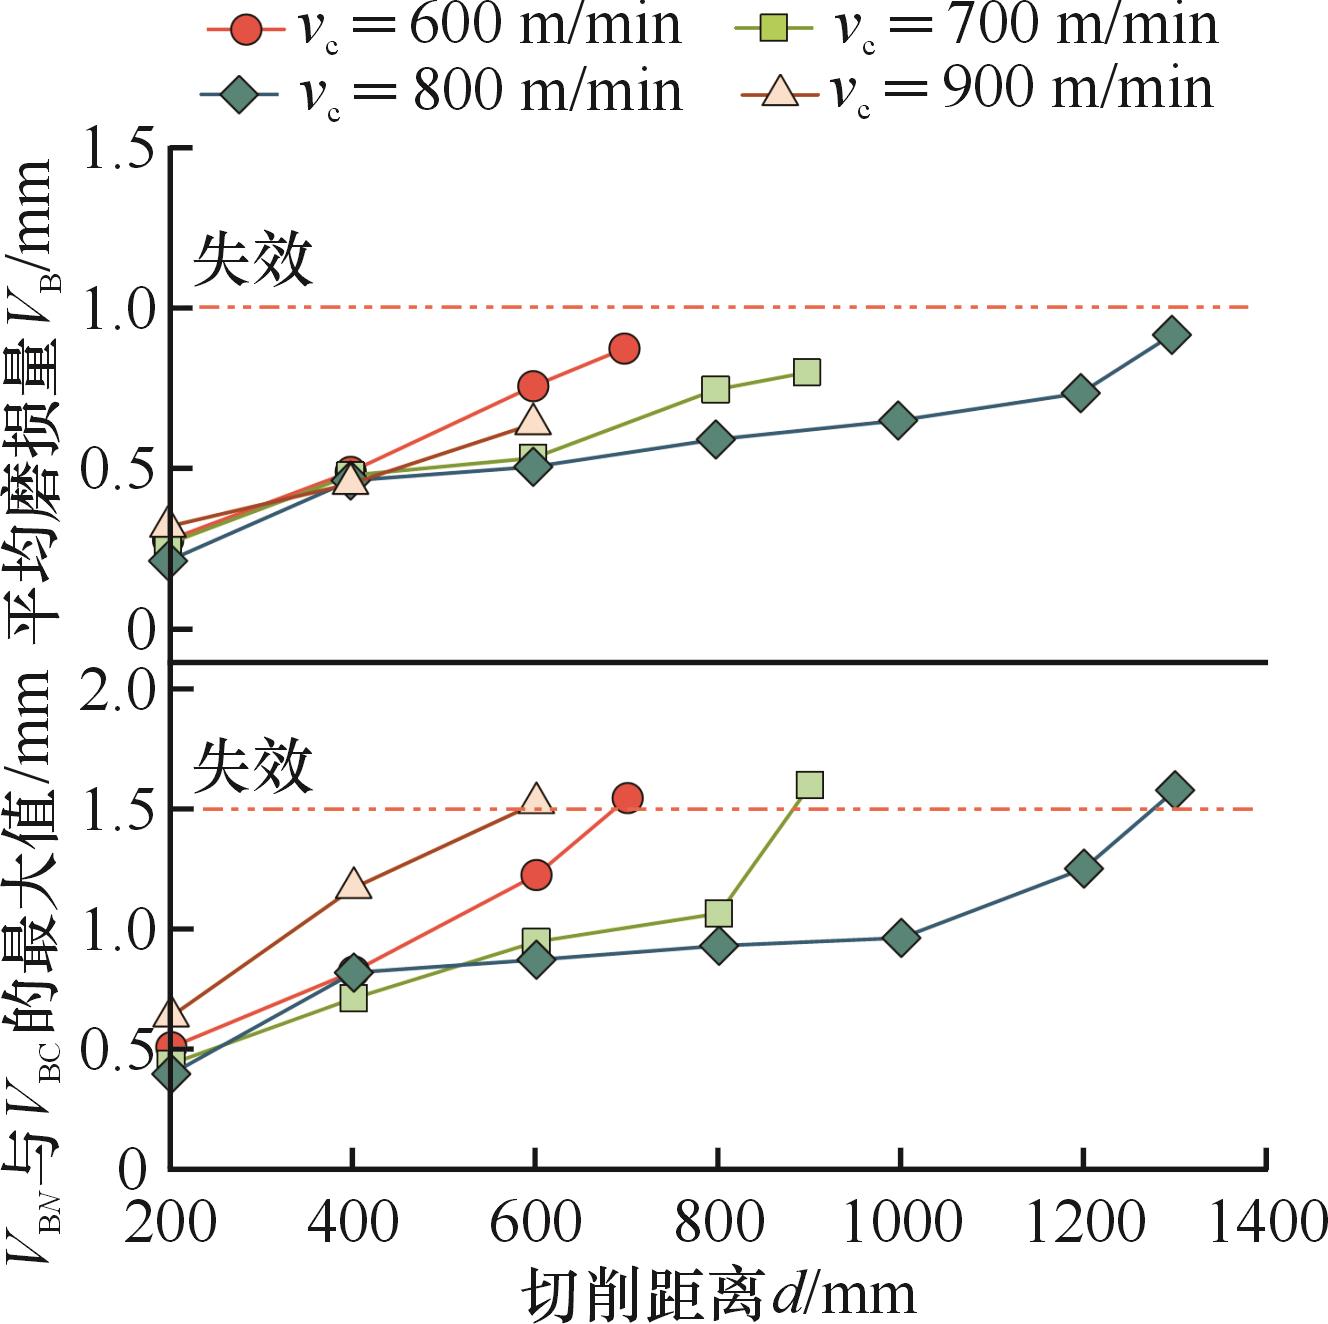
图8 不同铣削速度下复杂刃形α/β-SiAlON陶瓷刀具寿命曲线
Fig.8 Life curves of complex-edge α/β-SiAlON ceramic cutting tools under different milling speeds
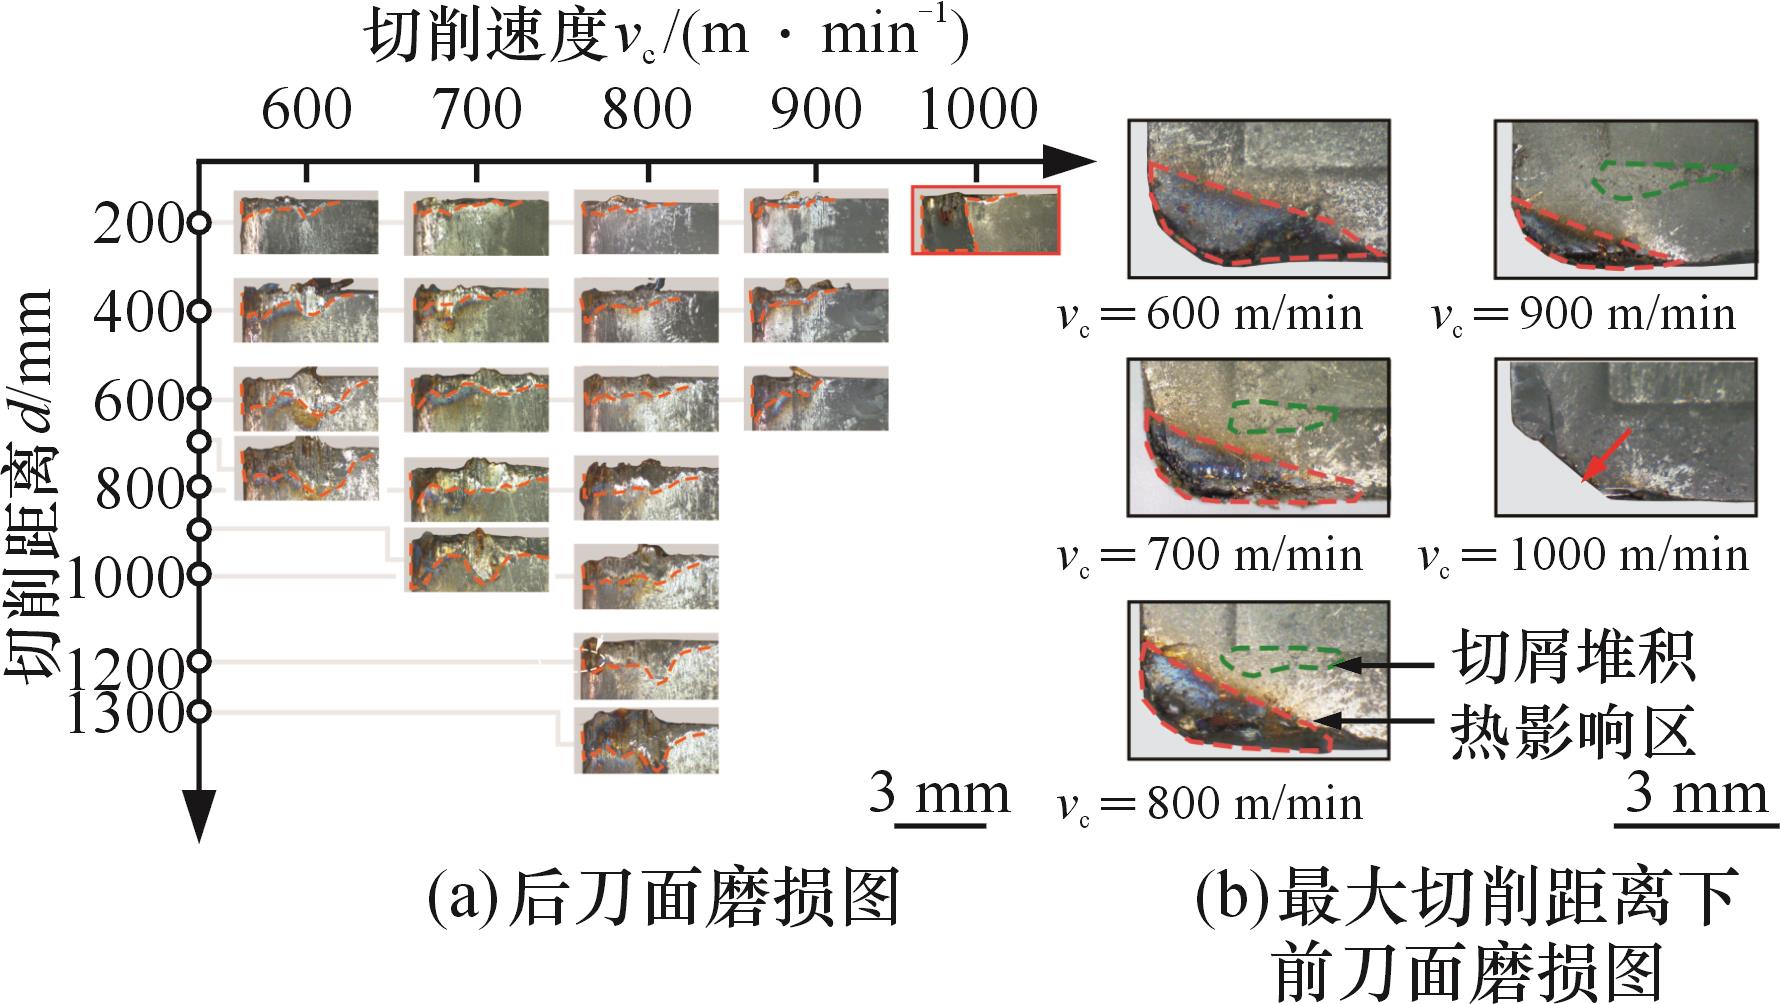
图9 不同铣削速度复杂刃形α/β-SiAlON陶瓷刀片磨损
Fig.9 Wear diagrams of complex-shaped α/β-SiAlON ceramic cutting tools after machining at different milling speeds
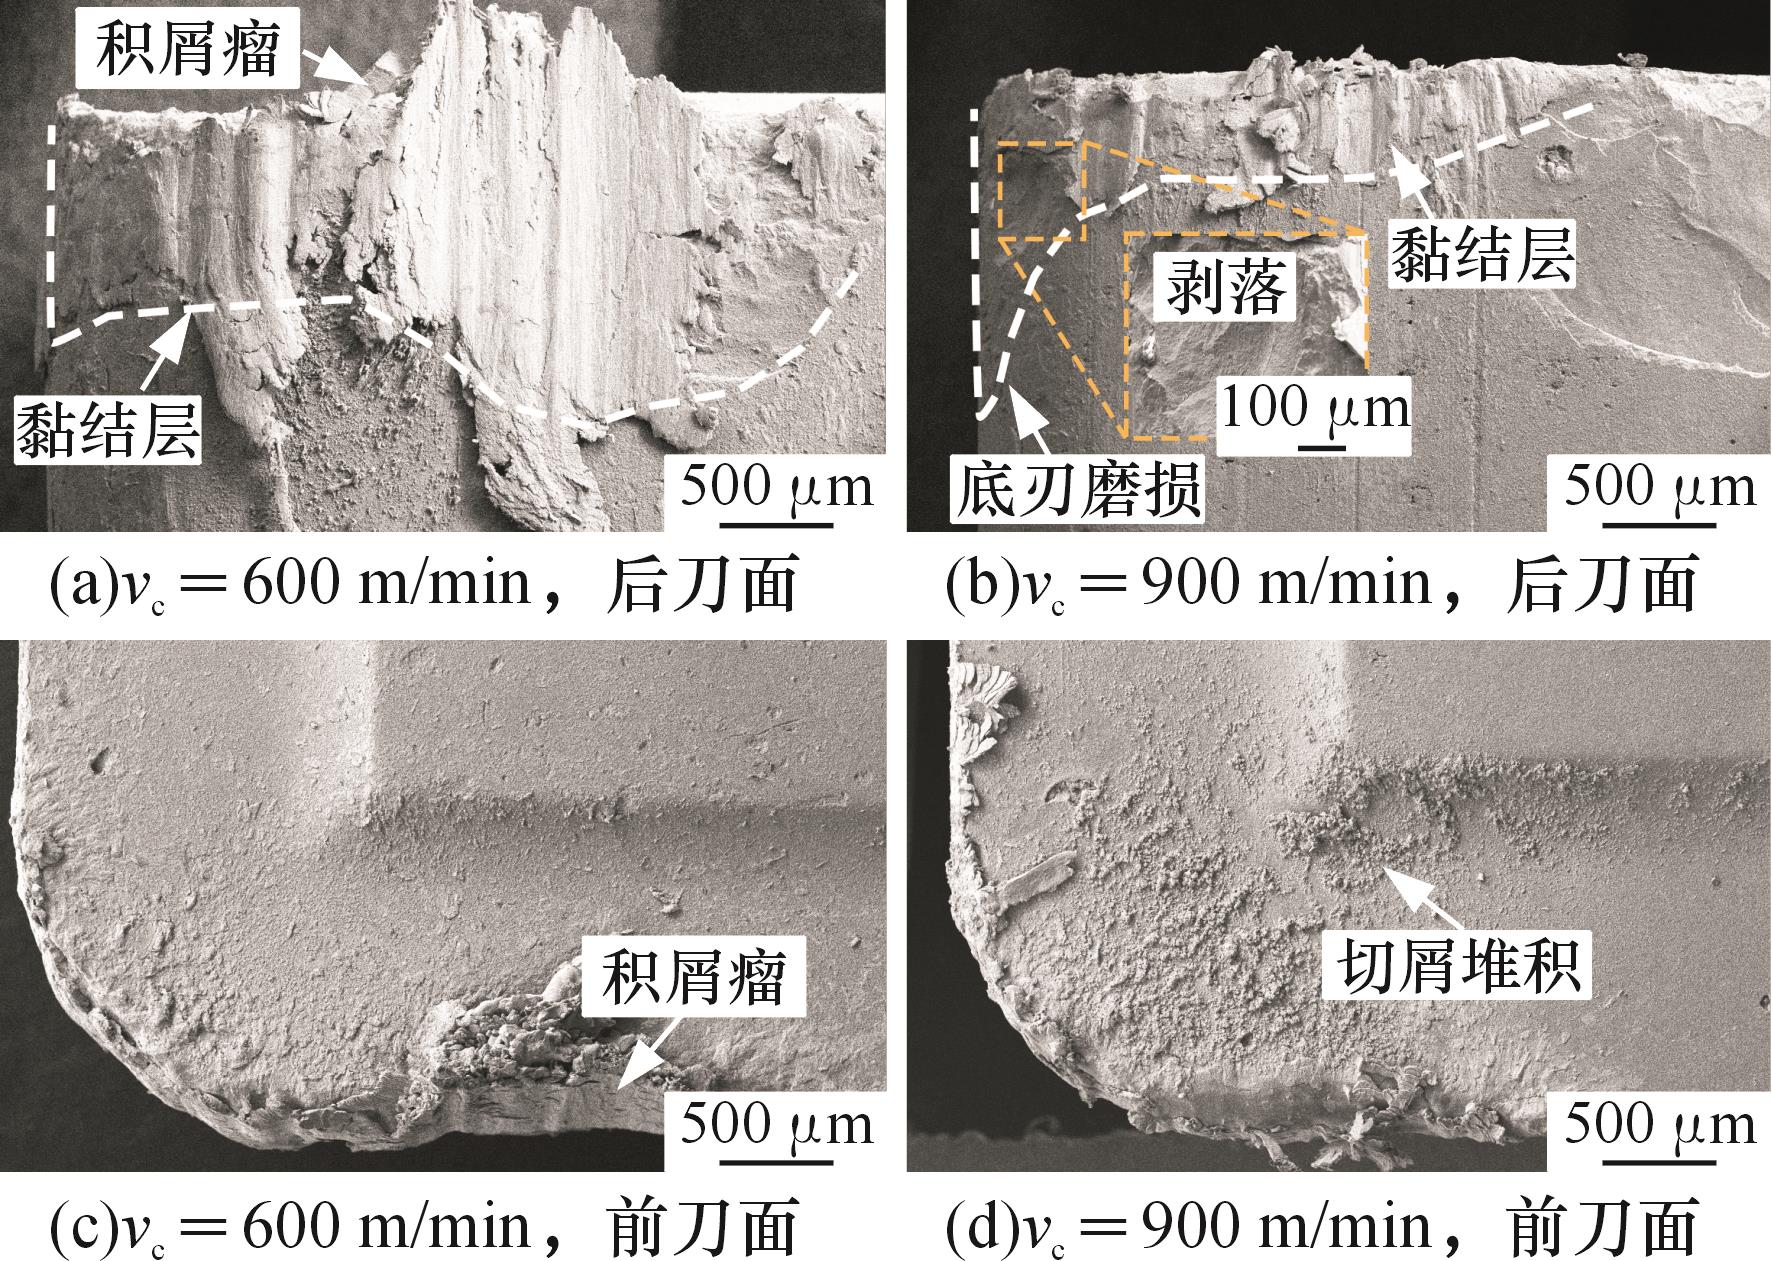
图10 不同铣削速度下复杂刃形α/β-SiAlON陶瓷刀片SEM形貌
Fig.10 SEM morphologies of complex-profiled α/β- SiAlON ceramic inserts under different milling speeds
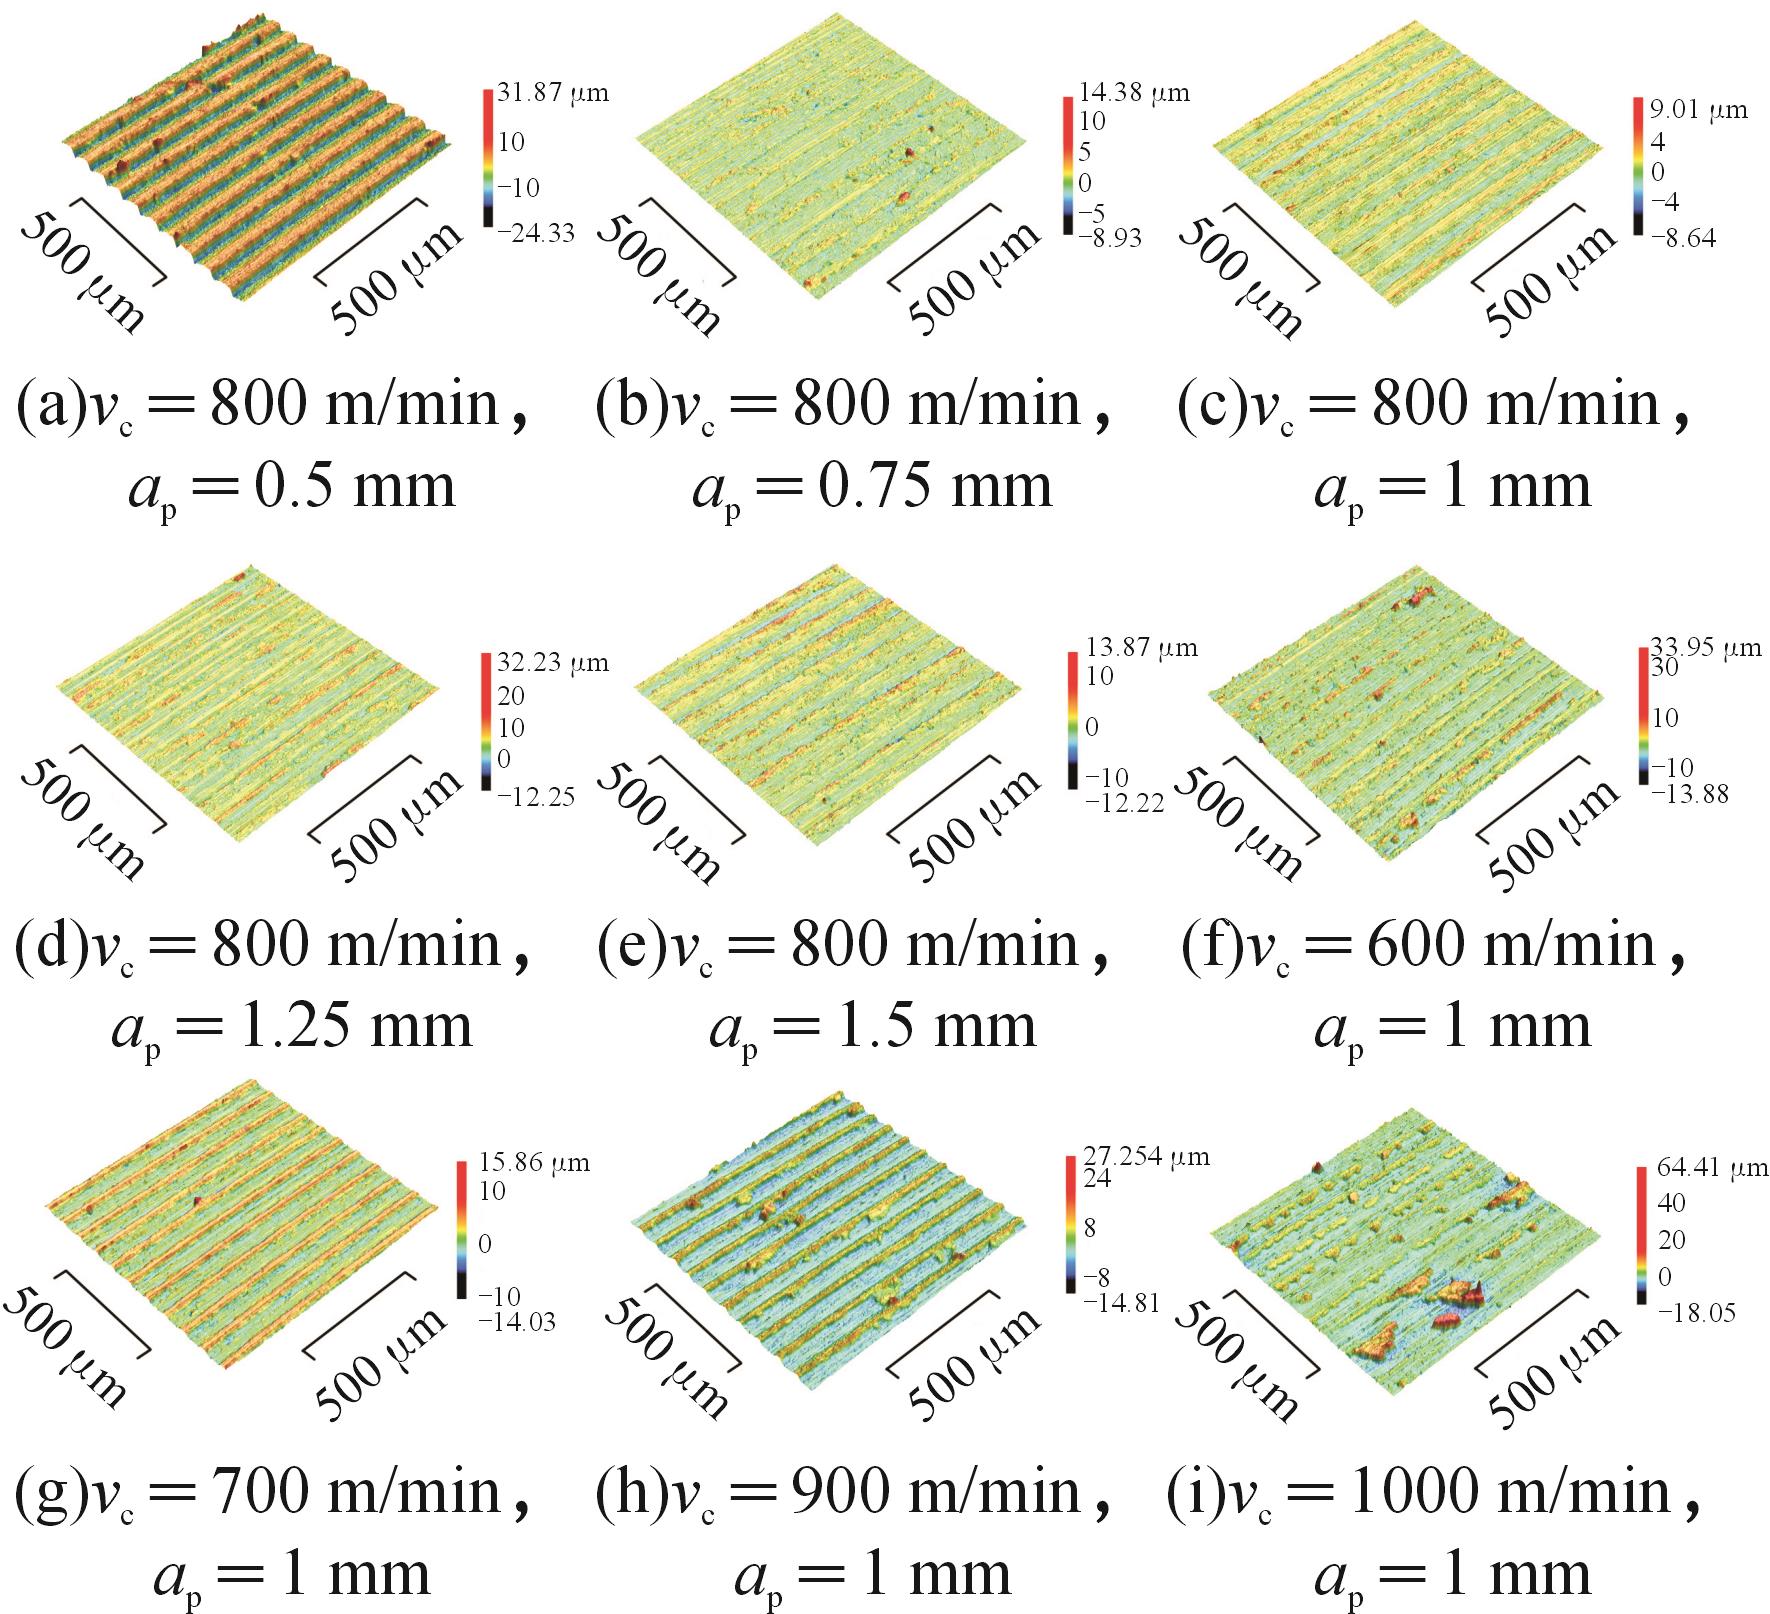
图11 不同工况下加工表面三维形貌
Fig.11 Three-dimensional surface topography under different working conditions
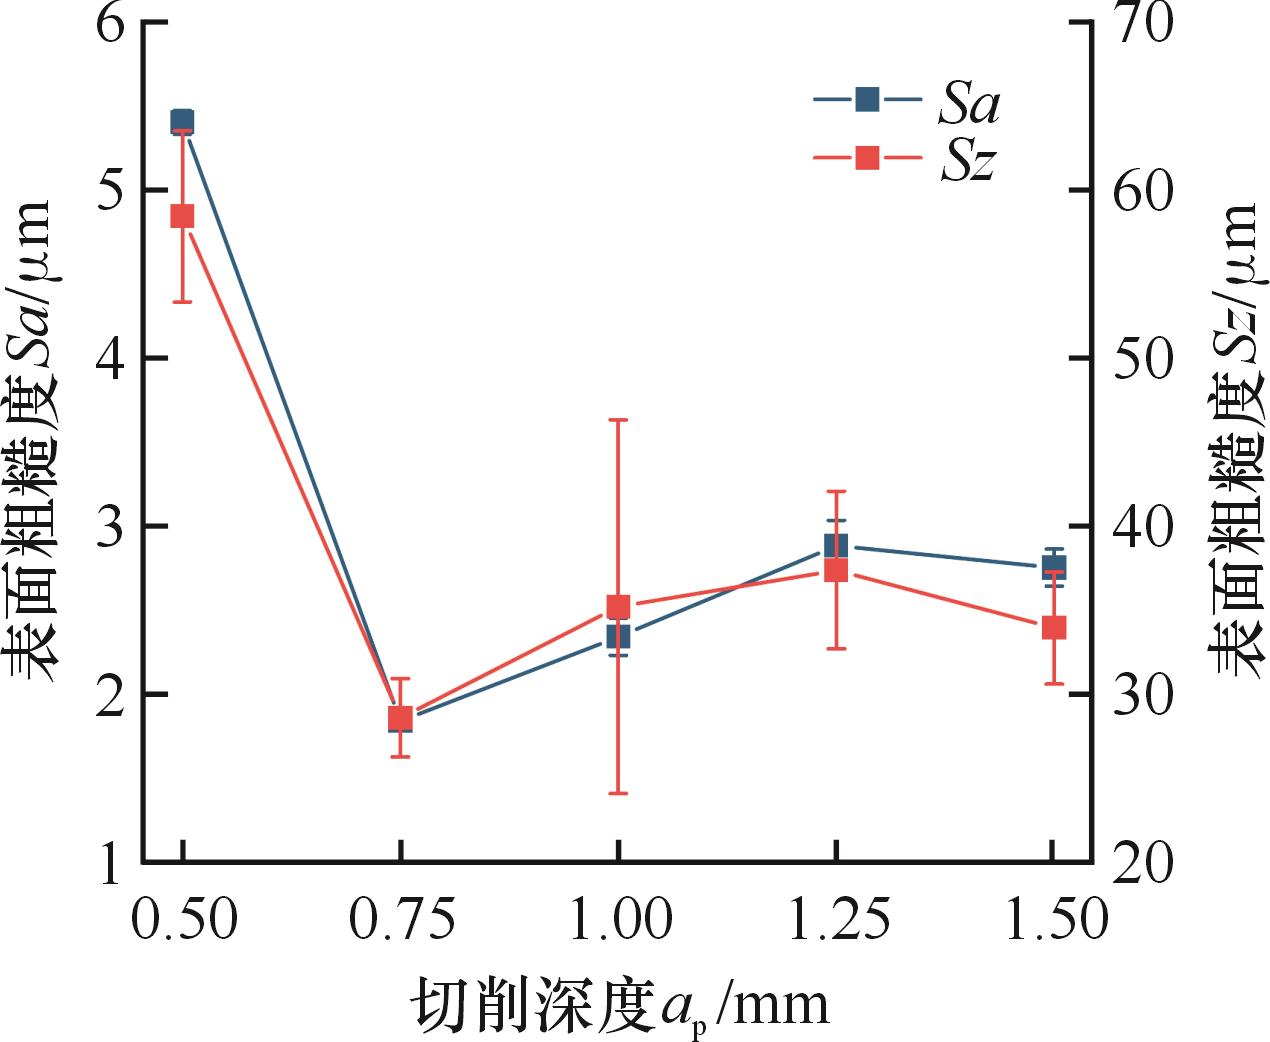
图12 不同铣削深度下的工件表面粗糙度
Fig.12 Surface roughness vs. milling depth
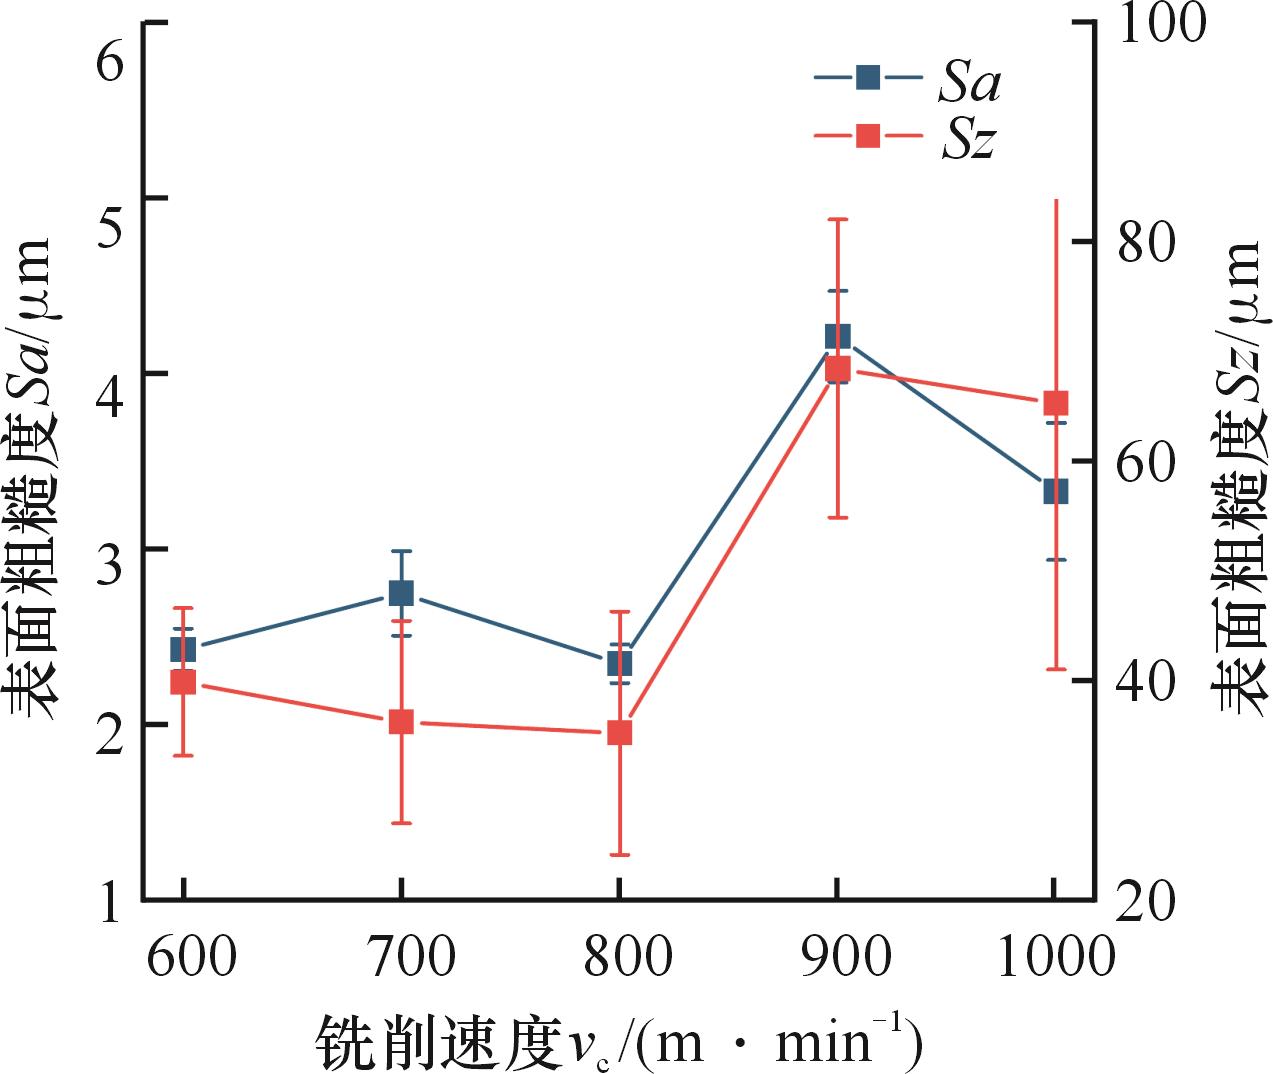
图13 不同铣削速度下的工件表面粗糙度
Fig.13 Surface roughness vs. milling speed
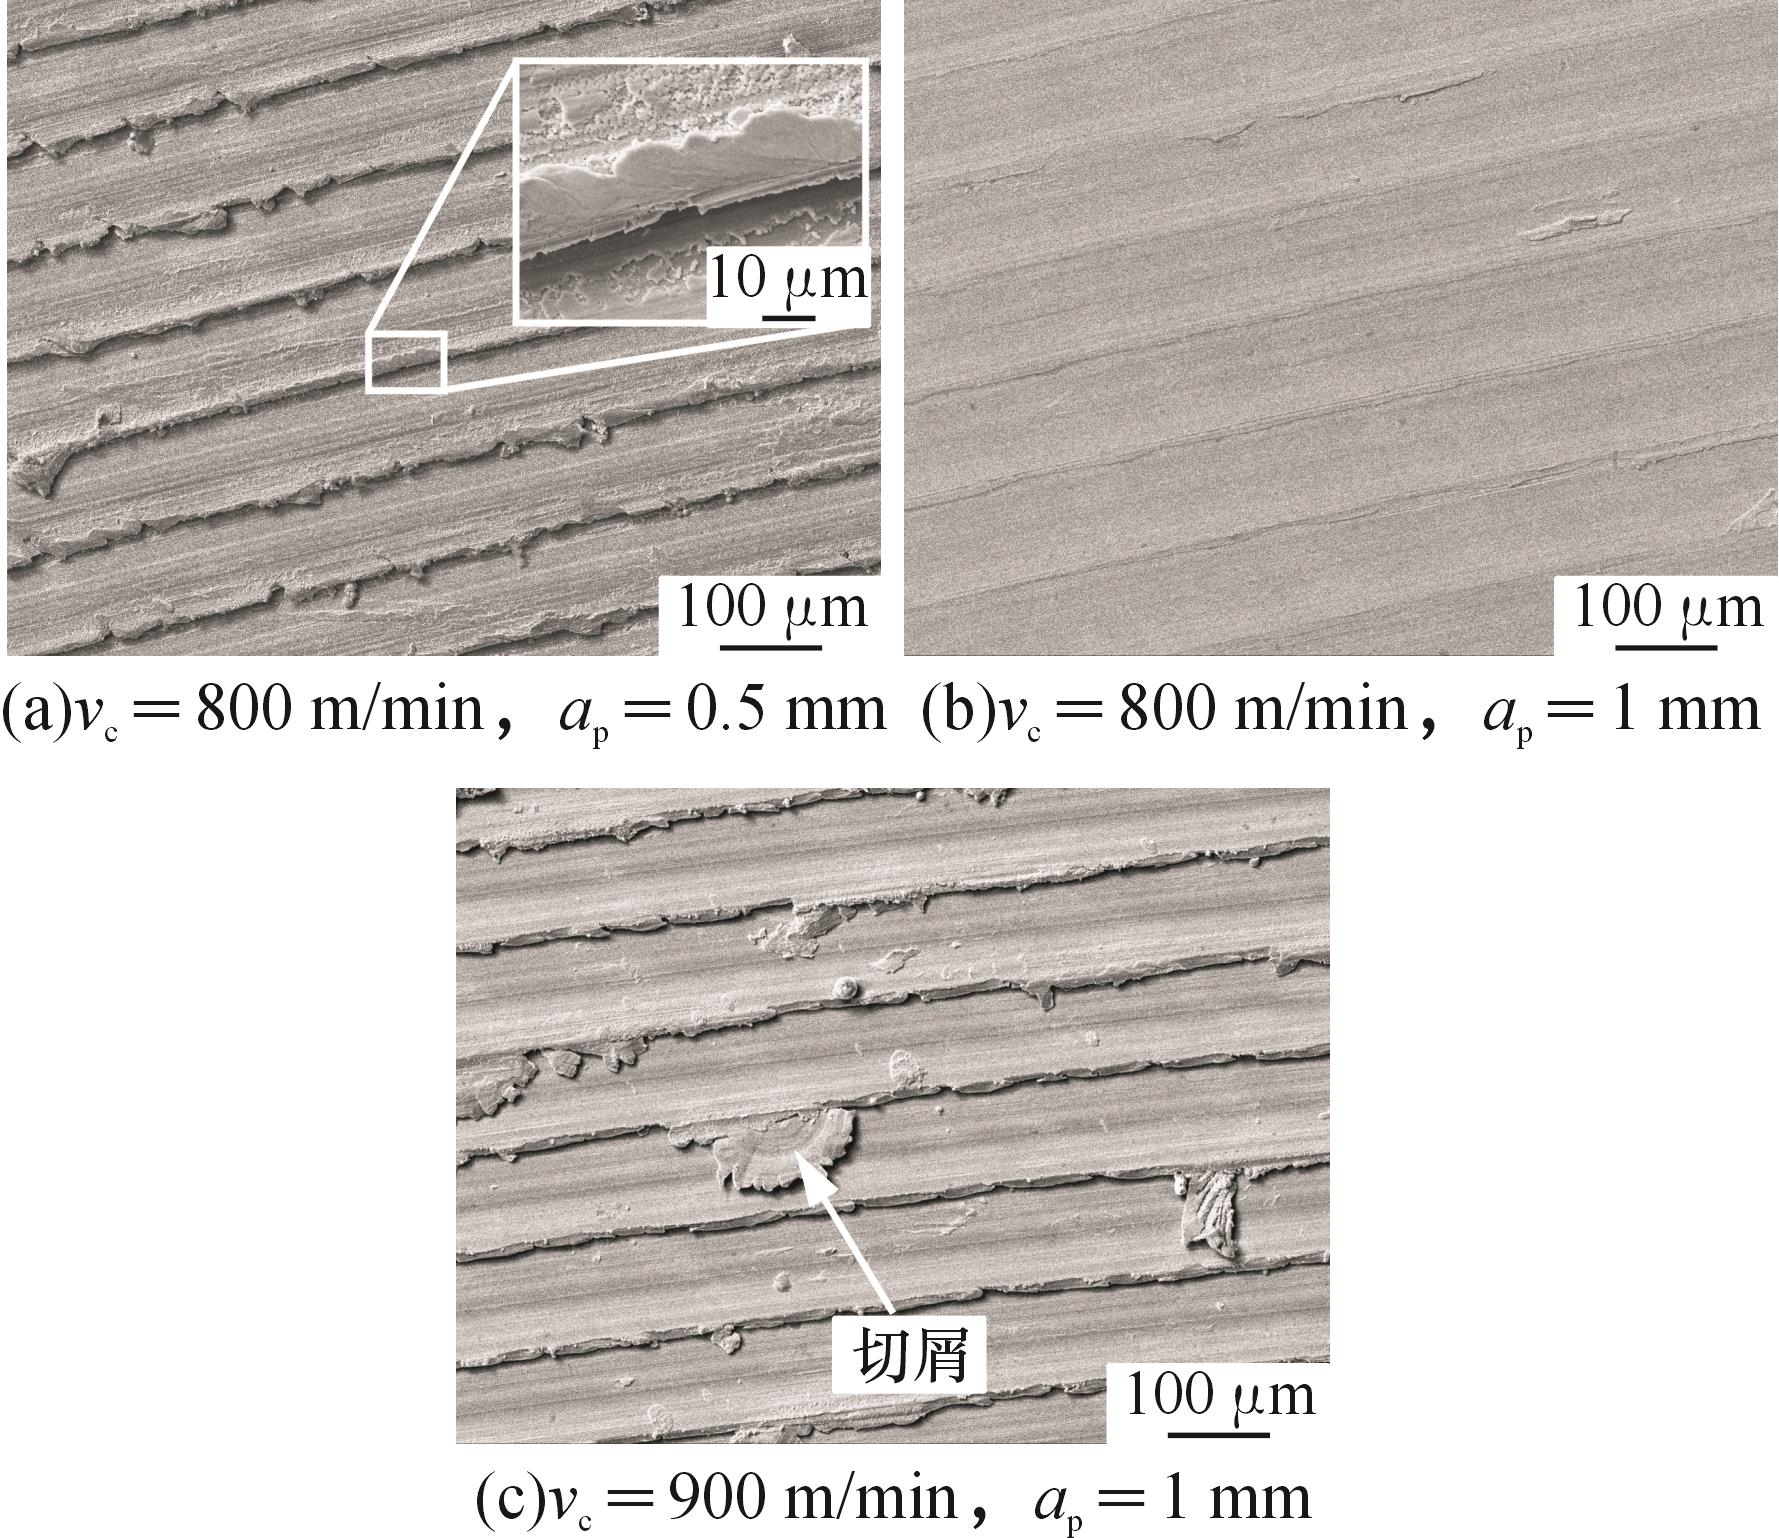
图14 不同工况下加工表面SEM形貌
Fig.14 SEM morphologies of machined surfaces under different working conditions
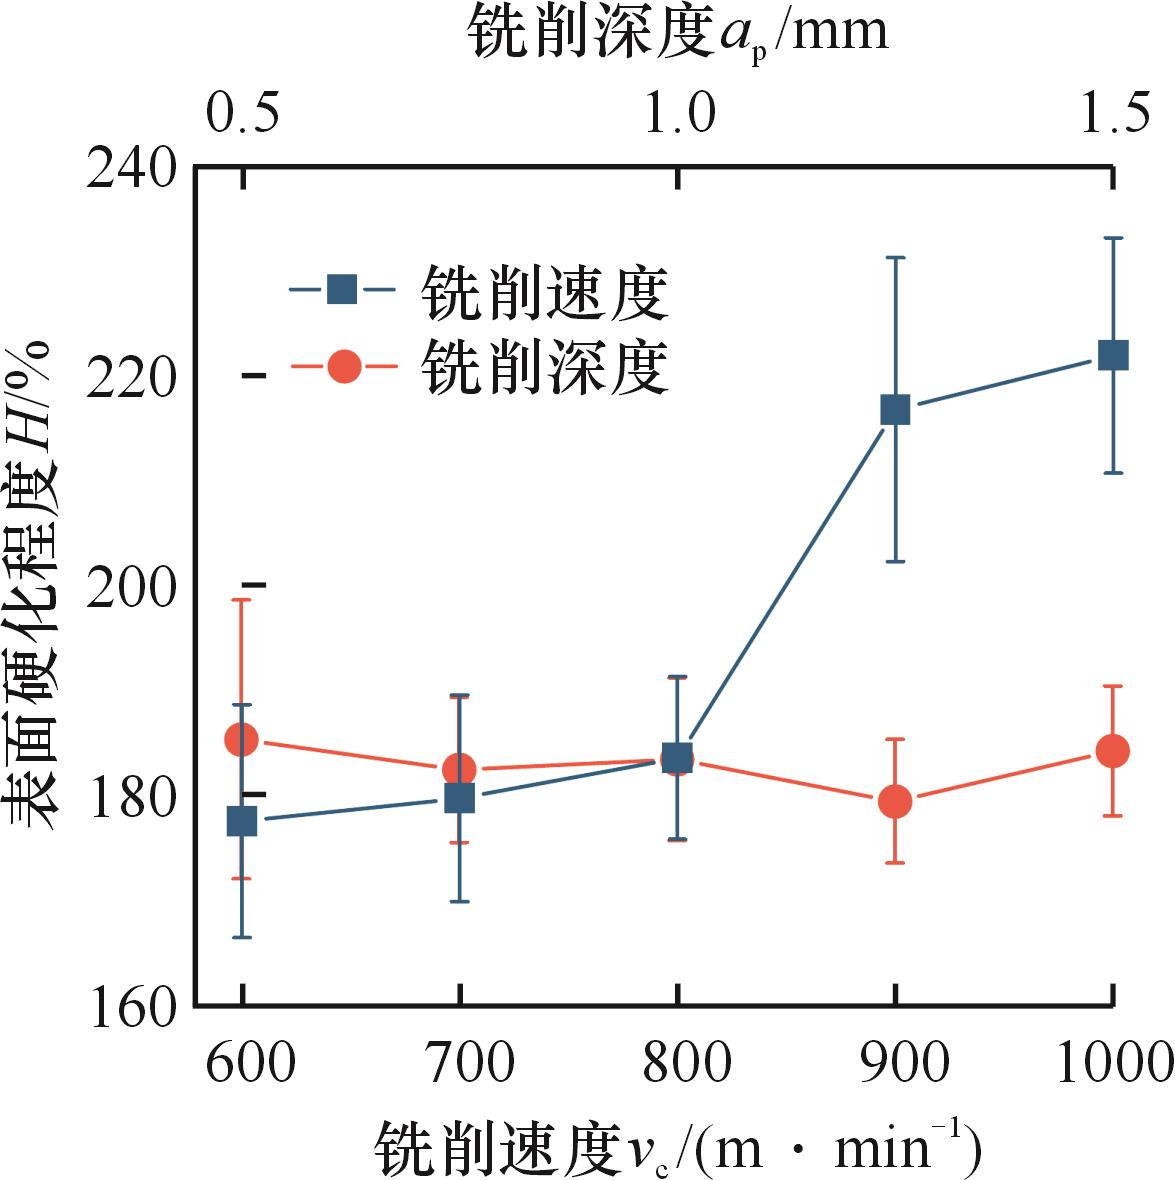
图15 铣削速度和铣削深度对表面硬化程度的影响
Fig.15 Influence of milling speed and milling depth on the degree of surface hardening
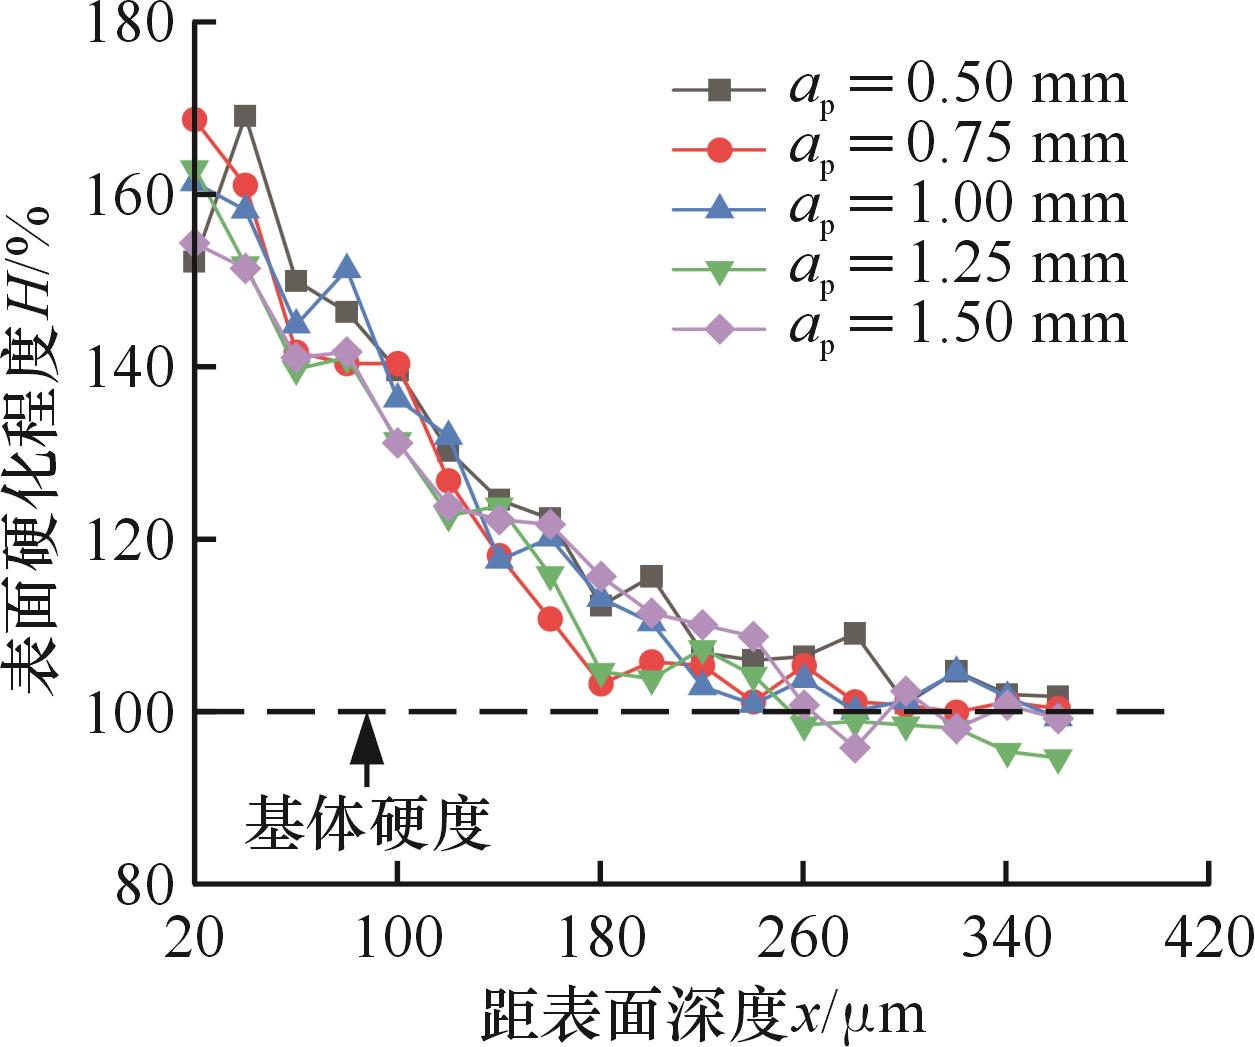
图16 不同铣削深度工件表层硬化测试结果
Fig.16 Test results of surface hardening of workpieces at different milling depths
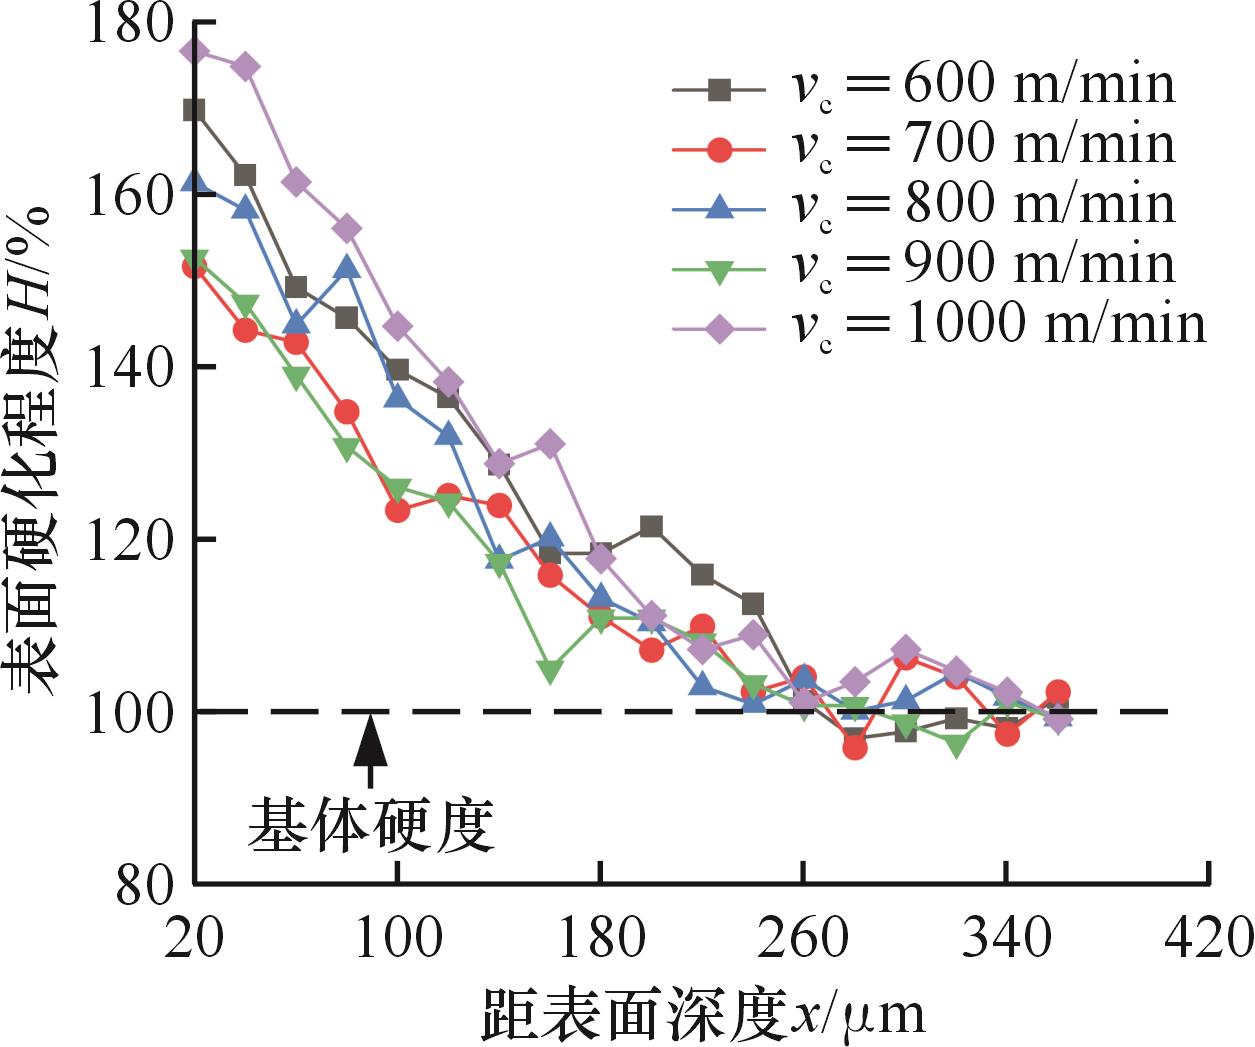
图17 不同铣削速度工件表层硬化测试结果
Fig.17 Test results of surface hardening of workpieces at different milling speeds
| [1] | de BARTOLOMEIS A, NEWMAN S T, JAWAHIR I S, et al. Future Research Directions in the Machining of Inconel 718[J]. Journal of Materials Processing Technology, 2021, 297: 117260. |
| [2] | YIN Zengbin, HAO Xiaohua, PENG Haohui, et al. A New β-Sialon Ceramic Tool Prepared by Microwave Sintering and Its Cutting Performance in High-speed Dry Machining Inconel718[J]. The International Journal of Advanced Manufacturing Technology, 2022, 118(9/10): 3105-3117. |
| [3] | GUO Fuzhou, YIN Zengbin, HONG Dongbo, et al. Cutting Performance of a New Spark Plasma Sintered SiAlON Ceramic Tool for High-speed Milling of Inconel 718[J]. The International Journal of Advanced Manufacturing Technology, 2022, 119(11/12): 7327-7338. |
| [4] | PARENTI P, PUGLIELLI F, GOLETTI M, et al. An Experimental Investigation on Inconel 718 Interrupted Cutting with Ceramic Solid End Mills[J]. The International Journal of Advanced Manufacturing Technology, 2021, 117(7): 2173-2184. |
| [5] | MING W, HUANG X, JI M, et al. Analysis of Cutting Responses of Sialon Ceramic Tools in High-speed Milling of FGH96 Superalloys[J]. Ceramics International, 2021, 47(1): 149-156. |
| [6] | LI Y, ZOU B, SHI Z, et al. Wear Patterns and Mechanisms of Sialon Ceramic End-milling Tool during High Speed Machining of Nickel-based Superalloy[J]. Ceramics International, 2021, 47(4): 5690-5698. |
| [7] | FERNÁNDEZ-LUCIO P, PEREIRA NETO O, GÓMEZ-ESCUDERO G, et al. Roughing Milling with Ceramic Tools in Comparison with Sintered Carbide on Nickel-based Alloys[J]. Coatings, 2021, 11(6): 734. |
| [8] | MA Z, XU X, HUANG X, et al. Cutting Performance and Tool Wear of SiAlON and TiC-whisker-reinforced Si3N4 Ceramic Tools in Side Milling Inconel 718[J]. Ceramics International, 2022, 48(3): 3096-3108. |
| [9] | OGHBAEI M, MIRZAEE O. Microwave Versus Conventional Sintering: a Review of Fundamentals, Advantages and Applications[J]. Journal of Alloys and Compounds, 2010, 494(1/2): 175-189. |
| [10] | THAKUR A, GANGOPADHYAY S. State-of-the-art in Surface Integrity in Machining of Nickel-based Super Alloys[J]. International Journal of Machine Tools and Manufacture, 2016, 100: 25-54. |
| [11] | BITTERLICH B, BITSCH S, FRIEDERICH K. SiAlON Based Ceramic Cutting Tools[J]. Journal of the European Ceramic Society, 2008, 28(5): 989-994. |
| [12] | 殷增斌, 朱智勇, 王子祥, 等. 复杂刃形陶瓷刀具微波烧结技术研究[J]. 中国机械工程, 2022, 33(8): 899-907. |
| YIN Zengbin, ZHU Zhiyong, WANG Zixiang, et al. Study on Microwave Sintering Technology of Complex-shaped Ceramic Tools[J]. China Mechanical Engineering, 2022, 33(8): 899-907. | |
| [13] | 洪东波, 殷增斌, 陈为友, 等. 微波烧结复杂刃形SiAlON陶瓷刀具铣削GH4169高温合金性能研究[J]. 中国机械工程, 2023, 34(7): 770-779. |
| HONG Dongbo, YIN Zengbin, CHEN Weiyou, et al. Cutting Performance of Microwave-sintered Complex-shaped SiAlON Ceramic Cutting Tools in Milling GH4169 Superalloys[J]. China Mechanical Engineering, 2023, 34(7): 770-779. | |
| [14] | MOLAIEKIYA F, STOLF P, PAIVA J M, et al. Influence of Process Parameters on the Cutting Performance of SiAlON Ceramic Tools during High-speed Dry Face Milling of Hardened Inconel 718[J]. The International Journal of Advanced Manufacturing Technology, 2019, 105(1): 1083-1098. |
| [1] | 牛秋林, 朱陈一, 吴炳辉, 张晟逢, 郭涛, 高菁忆. 刀具表面微织构与微量润滑协同技术研究进展[J]. 中国机械工程, 2026, 37(4): 885-899. |
| [2] | 余昶锐, 刘良宝, 周靖刚, 张函, 黄东, 张宁, 李勋. 面向涡轮盘榫槽凹圆弧表面的滚压参数优化[J]. 中国机械工程, 2026, 37(1): 60-65. |
| [3] | 徐伟伟1, 张作轩1, 朱松青1, 殷增斌2. 氮化硅基陶瓷材料微波烧结参数实验优化[J]. 中国机械工程, 2025, 36(03): 435-443. |
| [4] | 周后明, 陈皓月, 李神贵. 基于梯度结构的Al2O3/ZrO2陶瓷刀具材料的制备及其力学性能[J]. 中国机械工程, 2023, 34(10): 1199-1207. |
| [5] | 洪东波, 殷增斌, 陈为友, 郑轶彤, 袁军堂. 微波烧结复杂刃形SiAlON陶瓷刀具铣削GH4169高温合金性能研究[J]. 中国机械工程, 2023, 34(07): 770-779,788. |
| [6] | 李祥, 郑光明, 颜培, 孙作民, 程祥, 刘焕宝. 清洁切削高温合金涂层刀具切削性能及加工表面完整性[J]. 中国机械工程, 2023, 34(04): 454-463. |
| [7] | 张硕, 邹平, 方锐, 周亮. 微织构车刀椭圆超声辅助切削加工性能研究[J]. 中国机械工程, 2023, 34(03): 287-291,299. |
| [8] | 张岩, 黄传真, 刘含莲. 氮化碳基陶瓷刀具材料的制备与力学性能研究[J]. 中国机械工程, 2023, 34(03): 352-358,368. |
| [9] | 吴振宇, 郑光明, 颜培, 杨先海, 赵光喜, 李学伟. 表面处理对TiAlSiN涂层刀具表面完整性及切削性能的影响研究[J]. 中国机械工程, 2023, 34(01): 75-83. |
| [10] | 于良, 郑光明, 杨先海, 程祥, 常垲硕, 李学伟. 深冷处理对PCBN刀具切削性能的影响研究[J]. 中国机械工程, 2022, 33(20): 2450-2458. |
| [11] | 张帅, 陈照强, 肖光春, 衣明东, 张静婕, 周婷婷, 许崇海. Si3N4/TiC/ZrSi2陶瓷刀具裂纹愈合性能研究[J]. 中国机械工程, 2022, 33(19): 2288-2297. |
| [12] | 关集俱, 高超, 徐正亚, 丁云鹏, 李特, 许雪峰. 多壁碳纳米管/油酸复合物纳米流体车削GCr15钢的性能研究[J]. 中国机械工程, 2022, 33(18): 2205-2214,2226. |
| [13] | 范庆波, 杨帆, 关晓艳, 李浩, 樊小强, 朱旻昊. TiVN涂层的耐磨性与切削性能的关联研究[J]. 中国机械工程, 2022, 33(12): 1493-1503. |
| [14] | 殷增斌, 朱智勇, 王子祥, 袁军堂. 复杂刃形陶瓷刀具微波烧结技术研究[J]. 中国机械工程, 2022, 33(08): 899-907. |
| [15] | 衣明东, 王建平, 李传浩 , 许崇海, . 双重润滑条件下的刀具切削特性研究[J]. 中国机械工程, 2022, 33(05): 615-622. |
| 阅读次数 | ||||||
|
全文 |
|
|||||
|
摘要 |
|
|||||
